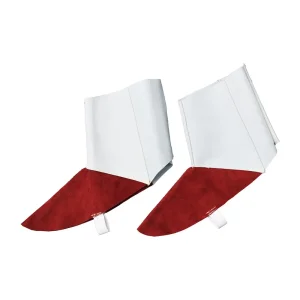
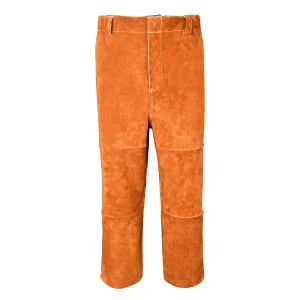
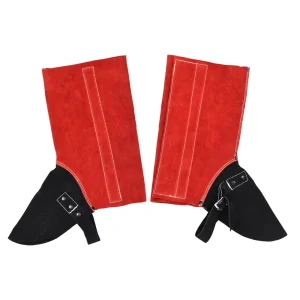
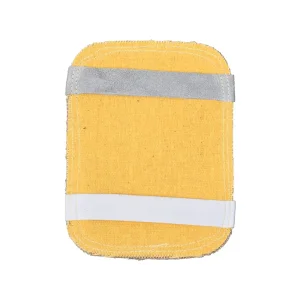
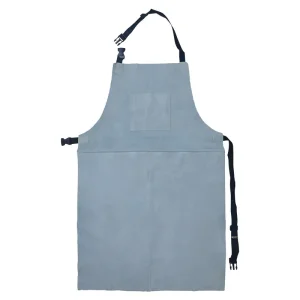
Direct factory supply featuring split cowhide spats, Kevlar-stitched gloves, aluminized backing pads, and abrasion-resistant leather trousers tailored for high-amperage metallurgy.
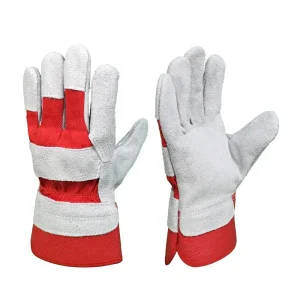
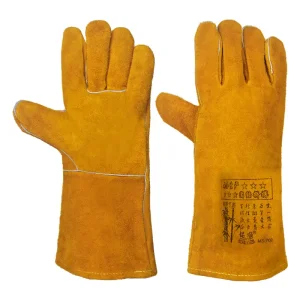
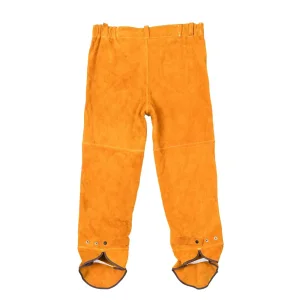
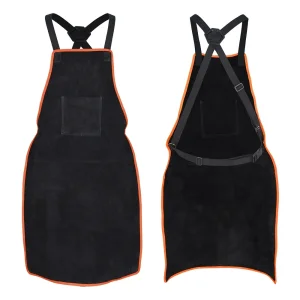
Modern heavy fabrication demands an evolution beyond rudimentary heat barriers. Industrial ergonomics, multi-hazard hybridization, and carbon-neutral supply chains define the new paradigm.
The traditional reliance on heavyweight whole-leather garments induces physical fatigue and heat stress during multi-hour operational shifts. Emerging industrial engineering integrates 9 oz / 11 oz treated flame-resistant cotton along the torso with selective Grade-A split cowhide or grain goatskin across zones subject to molten slag spatter, achieving an optimal thermal balance.
With the precision requirements of orbital TIG welding and automated flux-cored arc welding (FCAW), hand and arm protection must allow millimeter-level tactile dexterity. Ming Shun utilizes 3D keystone-thumb patterns, unlined seamless index finger contours, and heat-resistant Para-Aramid (Kevlar®) stitching to eliminate restrictive seam friction.
International regulatory regimes under EU REACH and North American OSHA mandates are aggressively penalizing toxic Chromium VI compounds in leather tanning. Our Gaozhou manufacturing base leverages eco-optimized tanning protocols that maintain structural leather fiber integrity while eradicating hazardous effluent runoff.
Global supply chain directors require quantifiable risk management. Ming Shun provides verifiable batch consistency, deep mechanical resistance data, and strict QA protocols across the production lifecycle.
| Procurement Evaluation Vector | Common Market Pitfalls (Brokers / Low-Tier) | Ming Shun Manufacturing Standard (Factory Direct) | Industrial Advantage |
|---|---|---|---|
| Raw Leather Homogeneity | Inconsistent hide split thickness (0.8mm - 1.6mm variance), brittle belly cuts prone to burn-through. | Uniform selection of selected shoulder and side cowhide; strictly graded 1.1mm - 1.4mm gauge. | Predictable thermal insulation; zero sudden slag burn-through under 300A current. |
| Thread Thermal Tensile | Polyester or nylon blend threads that melt instantly at 180°C, leading to catastrophic seam blowouts. | 100% 3-ply to 5-ply Dupont™ Kevlar® aramid fiber thread; flame-resistant up to 450°C continuous. | Zero seam opening during overhead welding; minimizes enterprise occupational liability. |
| Dyeing & pH Stability | High residual salt and acidic levels (pH < 3.5), causing operator skin contact dermatitis and premature dry rot. | Controlled neutral buffering (pH 4.5 – 6.5) with colorfast eco-dyes resistant to sweat leaching. | Superior wearer comfort; zero discoloration onto undergarments; prolonged shelf life. |
| Supply Chain Lineage | Intermediary trading companies with zero audit authority over subcontracted rural cottage workshops. | Fully integrated facility: Raw hide splitting → Precision die cutting → Dedicated assembly lines → In-house QA. | Uncompromised batch traceability; rapid sample iterations; direct OEM engineering adjustments. |
Safety environments differ fundamentally between enclosed confined spaces, open-air shipyards, and high-speed robotic assembly plants. Our garments are custom-engineered for specific hazard profiles.
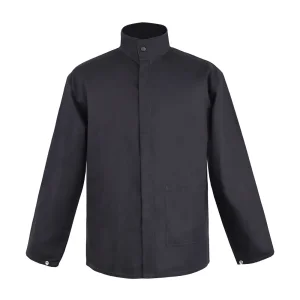
Designed for heavy multi-position flux-cored welding in damp, high-humidity environments. Features full split cowhide jackets with stand-up mandarin collars, double-reinforced Kevlar seams, and anti-static rust-proof covered brass snaps to insulate operators from conductive steel hulls.
Catering to cellulosic downhill pipeline welding where intense spatters drop vertically onto the lower abdomen, thighs, and boots. Tailored spats (e.g., MS-369D, MS-113) and cowhide leather trousers prevent molten iron ingress while maintaining stride mobility over uneven trench terrain.
High-dexterity goatskin TIG gloves matched with hybrid FR cotton jackets. Designed for robot programming maintenance technicians who require micro-control of wire-feed nozzles and digital teach pendants without stripping off their primary protective gear.
Direct radiation defenses incorporating aluminized composite hand pads (MS-106T) that reflect up to 95% of infrared radiant heat up to 1000°C. Paired with heavy split cowhide aprons featuring cross-back ergonomic harness systems (MS-360B) to disperse front-load weight evenly across the torso.
Quality is not inspected in; it is engineered through 8 discrete checkpoints controlled completely within our Guangdong industrial base.
Grading for structural fiber density, uniform tensile threshold, and zero scar blemishes across raw heavy cowhide stock.
Formulated non-chrome tanning solutions ensuring batch-to-batch colorfastness and permanent flame retardancy.
CAD-driven laser and hydraulic die cutting ensures zero panel measurement variance, optimizing seam alignment.
Heavy lockstitch assembly reinforced with 100% aramid thread, embedding concealed welts across all high-stress seams.
Application of dielectric insulated snaps, reinforced eyelets, and heavy-duty instep straps tested for mechanical tear resistance.
Automated steam and thermal pressing sets final garment dimensional stability to prevent post-laundering shrinkage.
100% inspection of stitch density (minimum 8-10 stitches per inch), tensile pull tests, and surface cleanliness.
Vapor-barrier polybagging with industrial desiccant agents preserving leather suppleness during trans-oceanic shipping.
Ming Shun products are manufactured to fulfill the exacting test benchmarks established by European (EN), North American (ANSI/NFPA), and International (ISO) bodies.
Certifying complete protective garments against minor spatter (Class 1: MMA, TIG, MIG) and extreme spatter scenarios with radiant heat (Class 2: MMA with basic or cellulose-covered electrodes, MAG with CO2 or mixed gases, MIG high-current, plasma arc gouging).
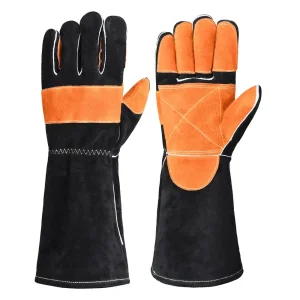
Classifies welders' protective gloves into Type A (elevated thermal and mechanical protection with moderate dexterity, ideal for MIG/Stick) and Type B (high flexibility and tactile micro-dexterity, standard for precision TIG operations).
Aligned with North American standards governing cut resistance levels (A1 to A9), puncture resistance, contact heat threshold, and open arc flash ATPV ratings for utility and multi-hazard field crews.
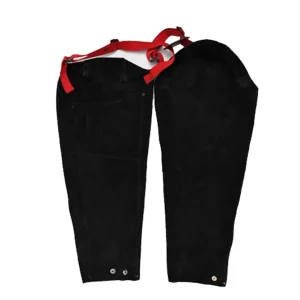
Direct factory supply featuring reflective FR cotton jackets, unlined TIG gloves, aluminized thermal gloves, full-grain winter options, and heavy split leather sleeves.
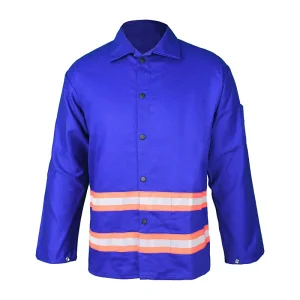
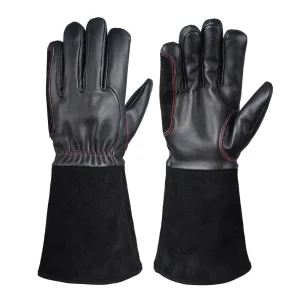
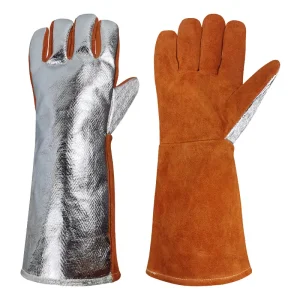
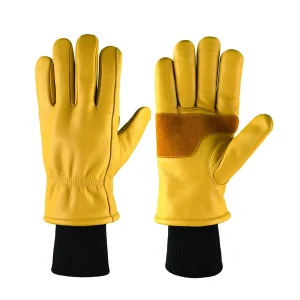
Ming Shun R&D facilities continuously prototype next-generation functional textiles, thermal barrier layering, and ergonomic integration for 2025–2028 deployment.
Integrating 1.5mm flexible silica-aerogel insulation blankets into the dorsal side of MIG/TIG gloves and shoulder yokes. This technology delivers a 60% reduction in heat transmission without the stiff, cumbersome bulk of conventional fiberglass batting.
Developing closed-loop regeneration protocols that convert tannery split-shavings into reinforced bonded technical leather substrates, achieving a 40% reduction in raw hide material waste while fulfilling corporate scope-3 emissions reduction goals.
Conductive yarn-embedded micro-sensors woven directly into FR cotton under-sleeves. These arrays communicate real-time core temperature and radiant thermal spike warnings to industrial telemetry platforms, proactively preventing heat prostration.
Direct answers addressing technical parameters, minimum order quantities (MOQ), custom private-label branding, and regulatory compliance protocols.
Guangdong Ming Shun Labour Protective Products Co., Ltd. operates a vertically integrated production campus encompassing over 25 years of specialized experience in Gaozhou, Guangdong. Rather than outsourcing, we maintain direct oversight of raw hide grading, eco-tanning drums, precision cutting, and high-tensile Kevlar lock-stitching across our 1,000+ strong workforce, ensuring absolute lot-to-lot consistency.
Yes. We specialize in contract private-label manufacturing for major industrial distributors across Europe, North America, and Australia. We support custom pattern tailoring, proprietary leather dye formulations, heat-debossed logos, embroidered badges, multi-language technical tags, and full retail or industrial bulk container packaging.
For established standard catalog styles, our baseline MOQ begins at 600 to 1,200 pairs for specialized gloves and 300 to 500 units for leather jackets or coveralls. Full container volume orders (20GP / 40HQ) typically ship within 35 to 45 business days following formal sample sign-off and lab tech-pack verification.
Every batch of tanned cowhide and treated FR cotton undergoes rigorous mechanical and thermal testing: limited flame spread (ISO 15025), impact of spatter droplets (ISO 9150), radiant heat transfer (ISO 6942), tear resistance, and electrical resistance. Model-specific test certificates and technical documentation files are provided upon inquiry.
Standard cotton or synthetic nylon threads break down rapidly when exposed to slag spatter or concentrated UV arc radiation, causing seam blowout within weeks. Dupont™ Kevlar® aramid thread does not melt, is inherently flame-resistant up to 450°C, and delivers four times the tensile holding power under severe thermal cycling.
Our finished leather garments undergo controlled residual moisture calibration (maintained strictly between 12%–14%) before packaging. Shipments utilize airtight moisture-barrier polybags, high-adsorption clay desiccants, and container-level humidity control packs to ensure pristine condition upon arrival at destination ports.