Integrate our precision helmet bib attachments and compatible protective PPE into your global supply chain with audited CE, ISO 9001, and EN ISO 11611 certifications.

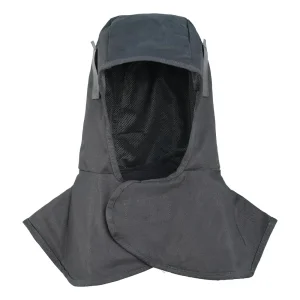
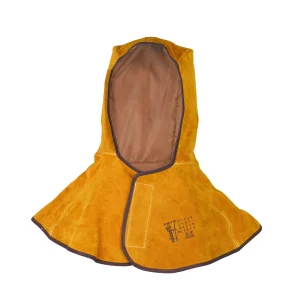
Analyzing cervical exposure risks, radiative heat flux in out-of-position fabrication, and the strategic convergence of ergonomic soft goods with hard-shell welding helmets.
Standard auto-darkening welding helmets terminate abruptly at the jawline, creating a vulnerable 6 to 10-centimeter aerodynamic vortex. In high-amperage FCAW and orbital GMAW, this critical gap exposes the thyroid, jugular artery, and anterior cervical triangle to direct infrared burns and incidental spatter accumulation.
Heavy preheating applications exceeding 250°C in pressure vessel manufacturing generate severe radiant fields. Industrial-grade helmet bibs engineered from Grade-A split cowhide or aluminized aramid form a convective barrier that dampens thermal conduction, preserving auto-darkening filter (ADF) battery packs and operator stamina.
Improperly calibrated bib attachments cause helmet pivot drag and anterior neck fatigue. Modern factory-engineered bibs utilize curved, perimeter-contoured die-cuts sewn with Kevlar® filament. This guarantees zero interference with PAPR (Powered Air-Purifying Respirator) airflow exhaust channels while keeping flex mass below 180 grams.
Why Guangdong Ming Shun's fully integrated processing, raw hide selection, and automated stitching provide unassailable cost advantages, technical consistency, and container-scale scalability.
By operating proprietary splitting and chrome-tanning workshops in Gaozhou, our technicians monitor hide density, fat liquor retention, and tensile shear at the source. This completely eliminates inconsistent hide thickness (held strictly at 1.2mm–1.4mm) across bulk global runs.
Every helmet bib profile is precision-cut using digital oscillating knife plotters. Edge variances are maintained within ±0.25mm, ensuring our tension-lock clips, silicone retention beadings, and Velcro® strips align flawlessly with OEM helmet shells like 3M Speedglas, Miller, and Lincoln Electric.
Standard stitching burns through in under 2 minutes when exposed to molten slag spatter. Ming Shun incorporates 100% 3-ply DuPont Kevlar® thread locked with twin-needle chain stitching at 8–10 stitches per inch, resisting mechanical pull forces exceeding 160 Newtons.
Every production batch of split cowhide and 9 oz / 11 oz FR cotton undergoing bib conversion is subjected to rigorous vertical flammability tests (ISO 15025 / ASTM D6413). Zero afterflame, zero afterglow, and zero molten dripping are strictly documented before carton pack-out.
From overhead pipeline passes to confined ballast tanks, explore the environmental hazards and exact technical specifications required for helmet bib deployment.
| Industrial Sector | Predominant Welding Process | Thermal & Physical Hazard Profile | Recommended Helmet Bib Configuration |
|---|---|---|---|
| Shipbuilding & Marine Drydocks | FCAW, Sub-Arc, Carbon Arc Gouging | Heavy dripping slag, high-amperage radiant heat (400A+), restricted neck rotation inside cellular hulls. | 1.3mm Premium Split Cowhide with Para-Aramid Thread & Push-Pin Rim Locking System. |
| Cross-Country Oil & Gas Pipelines | SMAW (Cellulosic 6010/8010), Orbital TIG | Overhead passes (5G/6G position), high ambient heat, windblown spatter, back-reflected sunlight arc glare. | Hybrid Split Leather front apron with 9 oz breathable FR Cotton nape drape and seal gasket. |
| Structural Steel & Bridge Erection | Self-Shielded Flux-Core (FCAW-S) | Gusting crosswinds directing molten iron beads behind the mask; high fall-arrest harness abrasion. | Extended 11-inch bib with curved lateral flare, compatible with industrial hard hat brim adaptors. |
| Heavy Pressure Vessel & Boiler Tanks | Heavy SAW, Multi-wire GMAW, GTAW | Severe preheat radiation (up to 300°C), prolonged enclosed thermal accumulation, extreme spatter rebound. | Aluminized Glass-Fiber laminated split leather with interior moisture-wicking FR liner. |
| Mining & Quarry Equipment Rebuild | Hardfacing, High-deposition SMAW | Massive tungsten carbide molten dropoff, excessive abrasion from gouging slag and grinding dust. | Extra-thick 1.5mm cowhide bib reinforced with brass mechanical rivets at lateral flex points. |
The helmet bib is transforming from a rudimentary leather flap into a modular, aerodynamically tuned protective interface integrated with respiratory and sensing technologies.
Positive-pressure respirator helmets require precise exhalation flow paths. Next-generation bib designs feature calibrated micro-perforated FR baffles that vent exhaled CO₂ and moisture downward while sustaining an impermeable barrier against airborne molten particulate.
Traditional pure leather, while robust, exhibits stiffness over long shifts. Emerging models combine an exterior chrome-free split leather contact shield with an interior silicone-treated meta-aramid membrane, reducing thermal weight by 35% without losing Class 2 spatter protection.
Adhesive Velcro strips frequently fail in greasy, high-heat environments. Ming Shun has engineered flexible anodized steel edge clips and magnetic snap rim tracks that clamp instantaneously onto any welding helmet brim without drilling, screw-holes, or adhesive degradation.
Evaluating vendor capabilities, regulatory documentation, and physical test performance to de-risk high-volume safety gear importing.
European PPE Regulation (EU) 2016/425 mandates that all leather products in skin proximity test below detection limits (<3 mg/kg) for Hexavalent Chromium (Cr VI) under ISO 17075-1, preventing contact dermatitis.
Bibs must withstand at least 25 drops of molten metal droplets without burn-through, while preserving radiant heat transfer index (RHTI 24) requirements of ≥16 seconds under a heat flux of 20 kW/m².
Random tensile tests pull sample seams to destruction. Premium industrial contracts require verifiable seam shear ratings along with complete material traceability back to the wet-blue tanning drum lot.
Tier-1 multinational contractors require audited labor parameters. Ming Shun operates in full compliance with BSCI and ISO 14001, verifying zero child labor, safe air exchange, and certified tannery effluent processing.
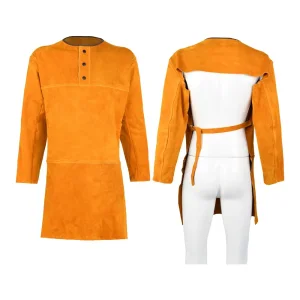
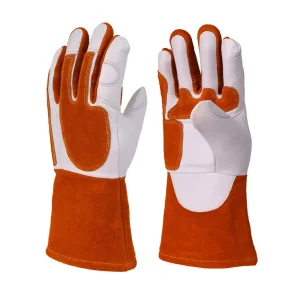
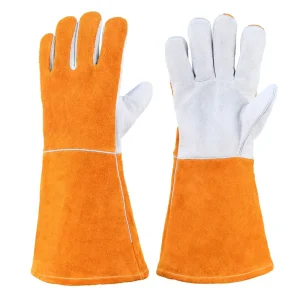
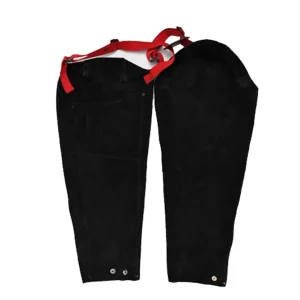
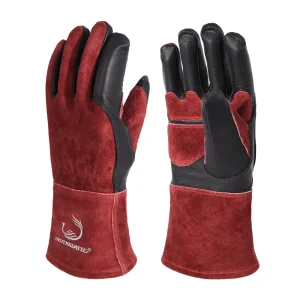
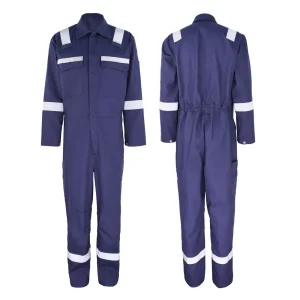
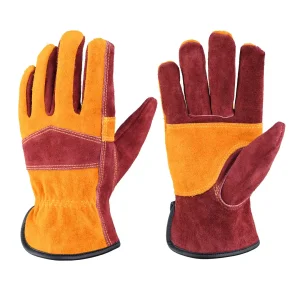
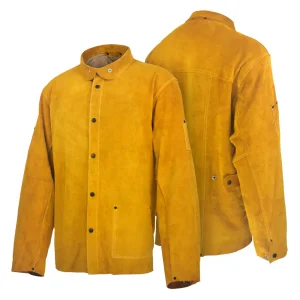
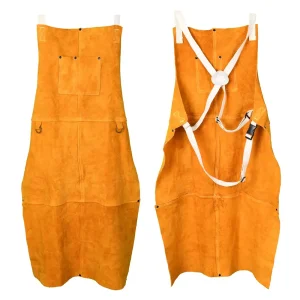
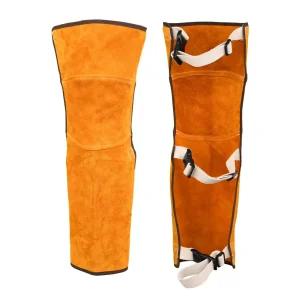
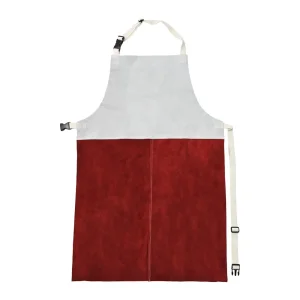
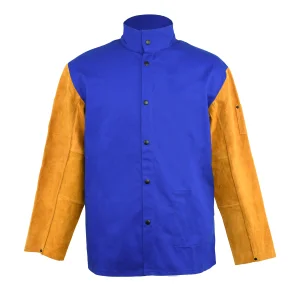
Complete your catalog with factory-direct procurement of matching cowhide jackets, aprons, sleeves, and protective leg covers engineered to work seamlessly with helmet bib attachments.
In-depth responses covering custom patterning, flame tests, mounting mechanism ergonomics, and container load optimization for global importers.
For high-amperage applications (MIG/FCAW/Stick), 1.2mm–1.4mm split cowhide leather provides unmatched defense against molten droplets up to 1,650°C. For prolonged production welding with minimal overhead spatter, hybrid composite constructions—featuring a leather chest drop backed with a 9 oz flame-retardant (FR) sateen cotton nape flap—deliver superior airflow and reduce thermal fatigue by over 25%.
We manufacture four universal fastening systems: (1) High-shear adhesive-backed heat-resistant hook-and-loop strips; (2) Molded elastomeric silicone push-on channel tracks that snap onto the helmet's perimeter lip; (3) Spring-steel tension clips engineered for hard hat combinations; and (4) Direct OEM rivet-hole pattern alignments matching Miller Digital Elite, Lincoln Viking, and 3M Speedglas shells.
Yes. Ming Shun operates a dedicated OEM/ODM prototyping line. We provide precision die adjustments, custom extension lengths (from 6 to 14 inches), laser debossing, thermal transfer brand logos, and retail-ready polybags with customized EAN/UPC barcoding for international retail distribution and industrial safety supply chains.
Our helmet bibs and protective leather assemblies conform to EN ISO 11611:2015 (Protective clothing for use in welding and allied processes) Class 1 and Class 2, EN 388 mechanical durability benchmarks, and ASTM D6413 vertical flame testing. Complete test reports from accredited bodies (SGS, TUV, SATRA) are supplied alongside bulk compliance documentation.
For standard catalog styles, our baseline MOQ is 500 units per design. For fully customized private-label configurations (bespoke dies, custom leather shades, specific hook-and-loop hardware), the MOQ is 1,000 units. Typical bulk order fulfillment for 20-foot or 40-foot high-cube containers averages 30 to 45 business days from sample approval.
Gaozhou is the global nucleus for split cowhide tanning and industrial protective soft-goods assembly. Because Ming Shun controls hide sorting, splitting, chemical degreasing, and chrome-tanning in-house, we eliminate the third-party intermediary markups that plague traders. This enables consistent thickness, odor minimization, low chromium volatility, and lower unit costs.
Partner directly with Guangdong Ming Shun's engineering team to develop bespoke helmet bib attachments and protective PPE matching your regional safety standards and market requirements.

