Verified manufacturing lots built with reinforced Kevlar® stitching, heavy-duty split cowhide, and radiant barrier membranes for global tier-one supply chains.
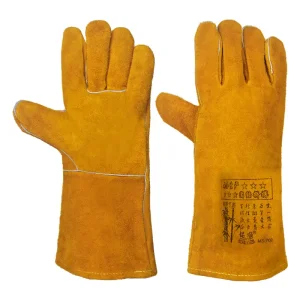
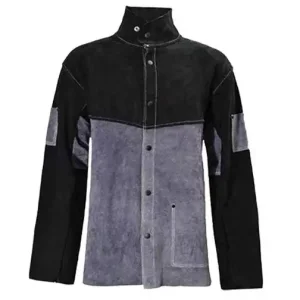
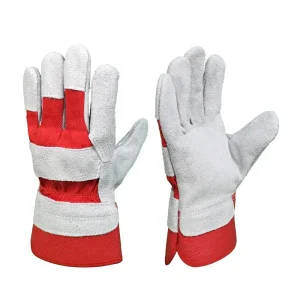
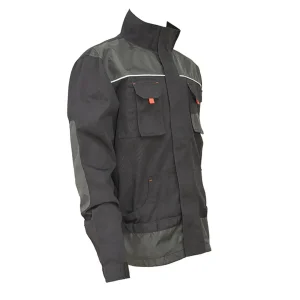

In high-amperage MIG/TIG welding cells, robotic spot-welding gantries, and subsea fabrication docks, power leads and utility bundles face extreme mechanical wear, molten spatter contact, and continuous friction.
Unscheduled MIG Torch Failures Attributed to Unprotected Lead Sheathing
Spec-Grade Split Cowhide Caliper Thickness for High-Spatter Shielding
Transient Thermal Resistance with Aluminized Aramid Composite Sheaths
Monthly Factory Throughput Units Supplying 40+ Industrial Sovereign Markets
Welding current leads operate under elevated duty cycles. When molten droplets pierce unarmored rubber or PVC jackets, dielectric breakdown triggers immediate short-circuiting against conductive workbenches, creating flashover risks, expensive copper loss, and catastrophic line stoppages.
In manual and automated fabrications, cable bundles are continuously dragged over rough diamond-plate flooring, laser-cut steel burrs, and structural beams. Factory-grade cable covers provide sacrificial outer dermis barriers with exceptional tear and tensile ratings.
Replacing an industrial multi-conductor TIG or MIG torch harness costs between $450 and $1,800, excluding unrecovered operational downtime during production shifts. Factory-direct cable covers extend harness operational life by 300% to 500% across demanding shifts.
From robotic automotive manufacturing cells to extreme-heat naval yards, each operating environment demands tailored material specifications and custom closure dynamics.
Continuous robotic spot and laser welding gantries demand dynamic flexibility. Cable covers must withstand multi-axis torsion (Axes 4, 5, and 6) without binding, pinching, or shedding particulate onto sensitive painted surfaces.
Low-Lint Chrome-Free CowhideCables routed hundreds of meters across wet, salty steel gratings endure continuous saline humidity and exposure to high-tonnage flux-cored arc welding (FCAW) slag. Heavy-duty cowhide covers prevent premature outer insulation cracking.
1.6mm Heavy Heavy CowhideTIG welding titanium and nickel superalloys requires absolute shielding gas purity. Flexible full-grain goatskin and pigskin covers protect high-frequency pulse lines from electrical interference while safeguarding delicate gas hoses.
Supple Grain ShieldingHeavy cross-country pipeline construction exposes equipment to mud, radiant ultraviolet degradation, and constant field manipulation. High-denier ballistic canvas and split leather hybrids offer high abrasion resistance and manageable drag weight.
Hybrid Heavy Canvas / Split LeatherSelecting the optimal cable cover system requires matching outer-layer metallurgy, stitch tension, and closure ergonomics with actual shop-floor hazards.
| Material Core Classification | Effective Thickness | Contact Temp Limit | Abrasion Cycle Rating (EN 388) | Ideal Closure Mechanism | Primary Industrial Use-Case |
|---|---|---|---|---|---|
| Selected Split Cowhide (Grade A) | 1.3 mm – 1.6 mm | Up to 480°C (Direct Droplet) | Level 4 (>8,000 Cycles) | Continuous Heavy Aramid Velcro / #10 Zipper | Heavy Manual MIG / Flux-Core Fabrication |
| Aluminized Radiant Fiberglass Composite | 0.8 mm – 1.1 mm | Up to 900°C (Radiant Heat) | Level 2 (>2,000 Cycles) | Overlapping Snap Flap + Aramid Lining | Foundry Hot-Metal Ladle Arc Welding |
| Premium Grain Goatskin / Cowhide | 0.9 mm – 1.2 mm | Up to 320°C (Conductive) | Level 3 (>4,000 Cycles) | Precision Coil Zipper with Leather Lip | High-Precision Orbital TIG & Cleanroom Welding |
| High-Tensile Flame-Resistant Canvas | 12 oz – 14 oz / yd² | Up to 260°C (Char Threshold) | Level 3 (>5,000 Cycles) | Industrial Brass Snaps / Molded Zipper | General Engineering Assembly & Shop Floor Bundling |
| Silicone Coated Para-Aramid (Kevlar®) | 0.7 mm – 1.0 mm | Up to 550°C (Continuous) | Level 4 (>10,000 Cycles) | Flame-Retardant Polyurethane Coated Zipper | Robotic Articulated Arms, BIW High-Speed Cells |
Operating a dedicated 25-year PPE and specialized leather facility in Gaozhou, Guangdong, we control every transformation step from raw hide sorting to final boxed export inspection.
Digital CAD nesting tables cut uniform lengths from 3.8m (12.5 ft) to 15m (50 ft) with sub-millimeter edge tolerances, preventing raw hide edge fraying and ensuring seamless zipper alignment on long production runs.
Every structural seam is sewn with 4-ply or 5-ply 100% DuPont™ Kevlar® thread. Seam terminations receive automated bar-tacking to eliminate tension unraveling when pulled around tight floor obstacles.
Comprehensive OEM/ODM personalization including deep heat debossing, flame-retardant heat transfers, custom pantone leather dyeing, bespoke inner diameters (from 22mm to 120mm), and branded distribution cartons.
Navigating global compliance frameworks is vital for safety PPE importers and tier-one engineering suppliers. Our production models are routinely audited and verified by independent accredited notified bodies.
Conforms to Class 1 and Class 2 protective gear parameters against spatters, short contact with flame, and thermal radiant heat loads. Raw leathers undergo strict testing to ensure zero azo dye content and compliant low Chromium (VI) levels under REACH Annex XVII.
Supports OSHA General Industry welding safety requirements (29 CFR 1910.252) regarding flame impingement resistance and cable damage mitigation. Meets burn rate resistance criteria under ASTM D6413 vertical flame testing.
Standardized operational quality management covers chemical treatment tracing, incoming raw material tensile testing, inline stitching inspection, and container drop testing for safe long-distance sea freight.
Key technical answers regarding raw material selection, closure mechanics, and container-level procurement.
Ballistic nylon performs well in pure abrasion tests, but it melts and fuses to inner cables when exposed to welding spatter and high-temp slag (temperatures often exceeding 800°C). Split cowhide is naturally flame-resistant, chars without melting, and provides reliable thermal insulation to protect internal gas and water lines.
Zippers offer a clean, snag-free exterior profile ideal for crowded welding tables and automated robotic arms. Hook-and-loop (Velcro®) allows rapid field installation and easy partial inspection without disconnecting torch leads from power sources. We manufacture both configurations to suit specific shop workflows.
Our raw cattle hides undergo calibrated mechanical splitting and electronic thickness grading. Each batch is sorted within tight caliper bands (e.g., 1.2–1.4mm or 1.4–1.6mm) to ensure uniform weight, flex resistance, and protective performance across complete container shipments.
Yes. Beyond standard widths (yielding 30mm, 40mm, and 50mm inner diameters), we build custom sleeves from 20mm up to 150mm ID to accommodate high-volume GMAW water cooling lines, internal push-pull wire feeders, and robotic sensor harnesses.
Standard lead times for custom-branded, private-label container lots range from 35 to 45 business days following technical sample approval. Stock-pattern trial lots can ship within 14 to 20 days via our expedited export division.
Yes. All tanned hides and hardware fittings are certified free of prohibited substances, complying with REACH Annex XVII, SVHC candidate lists, and RoHS directives, with verified documentation supplied prior to customs clearance.
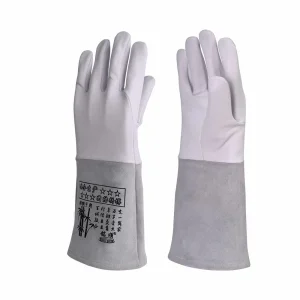
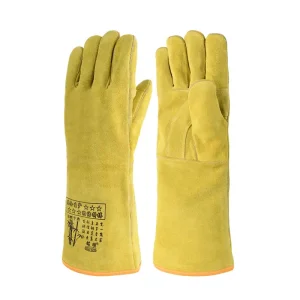
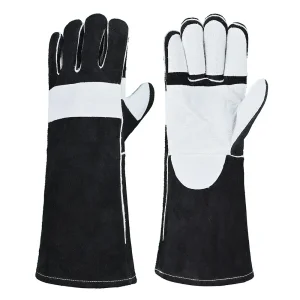
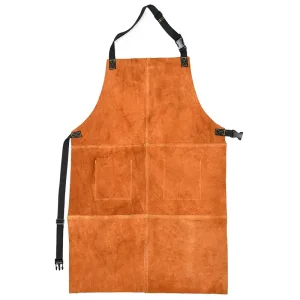
Integrate torch cable protection with our comprehensive range of certified welding apparel, leather jackets, hand protection, and workshop safety accessories.
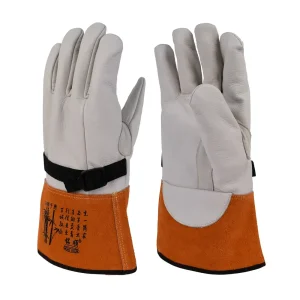
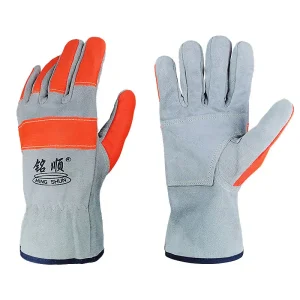
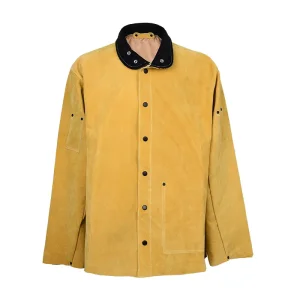
Partner directly with an established industrial manufacturer. Request a tailored technical quote, order certified prototype samples, or schedule an engineering consultation for your specific cable sleeve requirements.
Initiate Factory Inquiry