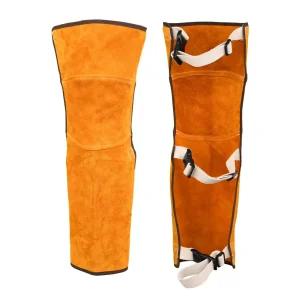
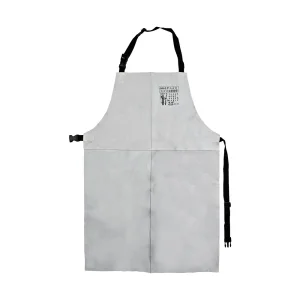
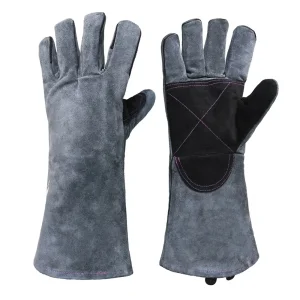
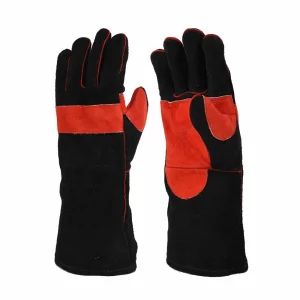
Engineered to mitigate radiant thermal exposure, molten drop slag penetration, and abrasion across intense fabrication workflows.

Analyzing supply chain shifts, occupational hazard metrics, and tier-1 fabrication requirements worldwide.
Lower extremity burns represent nearly 18.4% of total welding-related lost-time incidents according to global occupational health data. Incidents predominantly stem from downward-falling slag lodging in footwear seams, burning through shoelaces, or penetrating sub-standard synthetic blends.
The transition from low-density split leather to premium A-Grade Bovine Split Leather (1.2mm – 1.6mm thickness) has eliminated burn-through variations. With controlled chrome tanning, our hides offer uniform collagen fiber integrity that prevents embrittlement.
Heavy engineering projects in Europe, North America, and Australia are consolidating PPE vendor matrices. Direct alignment with primary tanning and stitch manufacturers eliminates middle-tier markup and guarantees strict traceability down to raw hide origin batches.
A quantifiable evaluation of protective gaiter substrates under extreme radiant heat and physical contact testing.
| Evaluation Parameter | Mingshun Premium Split Cowhide | Standard Commercial Cowhide | Aluminized Composite Glass | Treated FR Heavy Cotton (12oz) |
|---|---|---|---|---|
| Molten Drop Impact (EN ISO 11611) | Class 2 (>25 Drops) | Class 1 (15-20 Drops) | Class 2 (>30 Drops) | Class 1 (<15 Drops) |
| Direct Abrasion Resistance (EN 388) | Level 4 (>8000 Cycles) | Level 2-3 (2000-4000 Cycles) | Level 1 (Foil Delamination) | Level 2 (Pilling Risk) |
| Radiant Heat Transfer (RHTI 24) | Superior Retention (>18s) | Moderate (12-14s) | Maximum Reflection (>35s) | Low (<8s) |
| Seam Construction Integrity | 3-Ply Dupont Kevlar® Welded | Polyester / Cotton Blend | Kevlar® with Foil Sealing | Aramid Thread |
| Field Longevity (Heavy Duty Fabrication) | 12 - 18 Months | 3 - 6 Months | 4 - 8 Months (Delicate) | 2 - 4 Months |
Delivering turn-key documentary certification and custom anatomical sizing across distinct regional industrial markets.
Certified strictly in alignment with EN ISO 11611:2015 (Class 2, A1+A2) and Regulation (EU) 2016/425. Tested for tear strength, dimensional stability, pH value, and azo dye exclusions.
Meeting ANSI/ISEA 105 and OSHA 1910.132 general PPE guidelines. Reinforced foot flares engineered to accommodate steel-toe, composite, and heavy metatarsal work boots without slippage.
Formulated to comply with AS/NZS 4824 and mining site protocols. Includes quick-release Velcro calf seals and fire-retardant synthetic under-shoe straps designed for deep slurry and wet slurry operations.
Complete tech-pack digitization, debossed leather logos, fire-retardant custom barcode tagging, and direct pallet shipments configured to port of entry or client distribution hubs.
Custom leg coverings configured to withstand varied physical stresses, from flux-core slag to continuous grinding sparks.
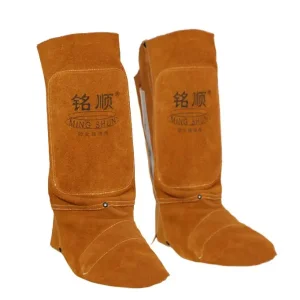
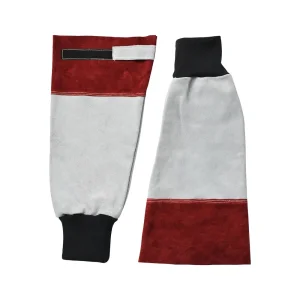
Welders operating in confined double-bottom vessel hulls face omnidirectional spark bounce and sharp edge contact. Extended-length split cowhide spats provide 360-degree lower-calf and ankle security against pooling dross.
High-elevation stick and sub-arc operators require lightweight articulation without compromising fire resistance. Ergonomic flared spat cuts prevent binding during deep kneeling or walking along I-beam flanges.
For operations facing continuous convective thermal currents and accidental molten bath splashes, our spats incorporate aluminized radiant overlays and fast-shedding exterior geometry for quick egress in emergencies.
Transforming traditional PPE through cutting-edge chemical treatments, ergonomic modularity, and circular sustainability.
Integrating eco-friendly silicone polymer matrices during the re-tanning drum phase to produce permanently water- and oil-resistant split cowhide that maintains flexibility even after repeated slurry exposure.
Developing magnetic high-shear closure systems that withstand rigorous physical movement yet allow millisecond emergency removal if molten iron breaks into footwear openings.
Investing in zero-liquid-discharge (ZLD) effluent tanning facilities in our Guangdong facility, lowering the carbon footprint of industrial protective leather by over 32% across the next 3 fiscal years.
Direct technical answers addressing procurement questions, OEM lead times, and engineering specifications.
Split cowhide features an open fibrous structure that naturally disperses radiant heat and resists blistering from hot slag beads far better than top grain leather, which tends to scorch and harden under direct spatter contact. Additionally, split leather offers superior dimensional stability under thermal loads.
All Ming Shun leather spats and leg protectors are constructed exclusively with continuous filament DuPont Kevlar® aramid or certified flame-retardant meta-aramid threads. This eliminates melted or burned-out seams when exposed to prolonged spark spray.
Standard bespoke OEM sample development requires 5–7 business days. Full container orders typically ship in 35–45 days depending on leather tanning batch sizes. Our minimum order quantity starts at 1,000 pairs per custom pattern.
Yes. We supply comprehensive factory test documents and third-party laboratory reports (such as SGS or TÜV) indicating conformity to EN ISO 11611 Class 2 standards for flame spread, radiant heat, and molten drop resistance upon client account initiation.
Source complementary protective equipment engineered under our unified Gaozhou manufacturing facility.