Direct-from-factory protective gear optimized for continuous wire feeding, intense thermal emissions, and heavy spatter environments across structural engineering and marine yards.
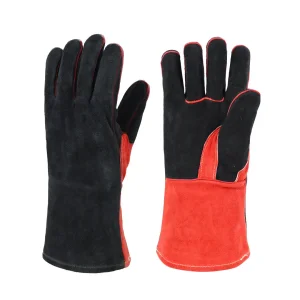
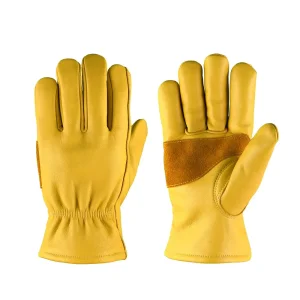
Why standard MIG or TIG welding gloves fail prematurely in Flux-Cored environments, and how specialized composite leather architectures provide vital thermodynamic defense.
Flux-Cored Arc Welding generates liquid core flux residues that react exothermically. Unlike GMAW (solid wire MIG), FCAW deposits up to 40% more slag at temperatures exceeding 1,450°C. Conventional leather rapidly vitrifies, leading to seam burn-through, leather hardening, and catastrophic micro-cracking across thumb crotches.
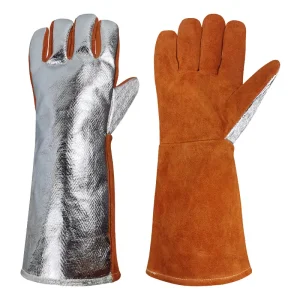
The open-arc chemistry of self-shielded (FCAW-S) and gas-shielded (FCAW-G) processes releases immense UV and infrared radiant energy. Without an internal thermal radiation barrier or reflective aluminized back hand paneling, heat transfer to the operative's dorsal region induces cumulative second-degree thermal fatigue within minutes.
Industrial FCAW utilizes continuous electrode diameters up to 3.2 mm (1/8"). The operator's guide hand experiences severe abrasive wear and frictional drag across the palm and index finger. Custom flux-cored gloves require grade-A side-split cowhide with tensile shear ratings capable of enduring mechanical scouring.
Quantitative breakdown of material specifications, thermal dissipation indices, and seam durability under severe industrial duty cycles.
| Performance Dimension | Standard MIG/GMAW Gloves | TIG/GTAW Fine Work Gloves | Ming Shun Heavy FCAW Gloves |
|---|---|---|---|
| Primary Shell Material | Split Cowhide / Pigskin (1.0 - 1.2 mm) | Top-Grain Goatskin (0.7 - 0.9 mm) | Select Heavy Side-Split Cowhide (1.3 - 1.5 mm) |
| Dorsal Radiant Heat Defense | Basic Cotton Fleece Lining | Unlined (Tactile Precision Priority) | Aluminized Rayon Sandwich + Aerogel/Fleece Barrier |
| Thread Specification | Standard Poly-Cotton or Single Kevlar | Fine Nomex / Kevlar 30/3 | 4-Ply Continuous Kevlar® with Full Welt Seams |
| Contact Heat Rating (EN 407) | Level 2 (Up to 250°C) | Level 1 (Up to 100°C) | Level 3 - 4 (Up to 350°C - 500°C Peak) |
| Slag Vitrification Resistance | Moderate (Crusts under heavy spatter) | Low (Perforates rapidly) | Exceptional (Sheds fluid molten beads without bonding) |
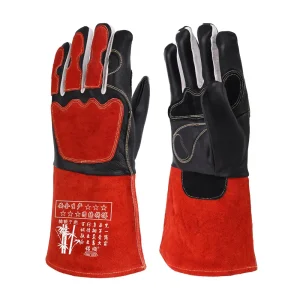
| Thumb & Palm Architecture | Standard Wing Thumb | Straight / Keystoned Thumb | Reinforced Keystone Thumb + Full Palm Load Spreader |
How tier-1 EPC contractors, shipyard operators, and national safety distributors optimize margin retention through engineered PPE lifecycle longevity.
Budget welding gloves often burn out every 2-3 shifts in 350-amp FCAW operations due to thread decomposition or stiffening leather. By selecting custom flux-cored gloves constructed with genuine Kevlar® welt shielding and specialized chromate tanning, procurement heads experience a dramatic plunge in inventory replenishment churn.
Transnational industrial infrastructure projects suffer when subcontractors purchase disparate safety items. Partnering with a vertically integrated OEM/ODM manufacturer guarantees uniform leather batch consistency, traceable chemical compliances (REACH, California Prop 65), and identical sizing standards across all port dispatches.
Worker fatigue and burn injuries remain leading contributors to lost work hours in heavy fabrication. Ergonomic gun-grip cuts, breathable non-woven fleece palm liners, and superior thumb flexibility encourage workers to keep protective gear on, preserving workflow cadence and driving safety record excellence.
Field-proven flux-cored hand protection configurations optimized for specific thermal loads, positional welding restrictions, and environmental stressors.
Hull erection and offshore jacket fabrication demand non-stop flux-cored welding in humid, high-salinity ambient conditions. Our marine-grade gloves incorporate moisture-resistant tallow tanning to stop leather crusting caused by constant sweat and sea mist exposure.
Field welders working on structural seismic splices use high-deposition self-shielded wires (FCAW-S). Gloves feature extended 6-inch split-leather gauntlets with rigid internal stays to prevent sparks from rolling into the sleeve while running vertical-up and overhead passes.
Thick-plate boom arms and excavator buckets require high-preheat multi-pass welding reaching 200°C interpass temps. Integrated aluminized outer backing reflects 95% of convective infrared glow, allowing uninterrupted bead deposition across heavy joints.
Navigating stringent PPE directives across North America, the European Union, the United Kingdom, and Australasia with certified testing dossiers.
Certified for Type A high-heat welding operations demanding maximum contact heat resistance, convective heat shielding, and high tear ratings per EN 388:2016+A1:2018.
Tested for the North American heavy industry market, achieving Level 4 abrasion resistance, Level 3 puncture performance, and Level 4 conductive heat resistance ratings.
Free of hazardous Hexavalent Chromium (Cr VI < 3 ppm), azo dyes, and short-chain chlorinated paraffins (SCCP), ensuring seamless clearance at EU and US customs.
Full retail packaging customization including barcoding, multiligual user information sheets (UIS) in 18 languages, and embossed client trademarks on cuff shields.
How Ming Shun integrates smart materials, nanofiber insulation, and circular sustainable chemistry into high-performance welding PPE.
Replacing bulky cotton linings with ultra-thin silica aerogel laminates, reducing glove bulk by 35% while increasing radiant heat deflection up to 600°C.
Advancing clean zeology and aldehyde-free organic tanning protocols to produce zero heavy-metal waste, drastically improving glove thermal shrink temperature limits.
Reinforcing structural stitching with graphene-functionalized aramid fibers to deliver exceptional anti-friction performance and imperviousness to molten micro-slag cuts.
Deploying micro-thermochromic indicators in cuff panels that visually signal when glove inner core temperatures approach the dermal threshold limit, alerting the operator.
Clear, direct answers for global procurement officers, compliance directors, and safety equipment distributors evaluating custom manufacturing partnerships.
For high-amperage FCAW operations, we recommend select side-split cowhide with a uniform thickness between 1.3 mm and 1.5 mm. When combined with an insulated palm pad and an aluminized dorsal barrier, this gauge delivers optimal slag dissipation without sacrificing trigger grip control.
All high-risk seams are built with full welted cowhide inserts that protect the underlying stitching. We strictly stitch using high-tensile 4-ply Kevlar® thread which remains dimensionally stable up to 450°C, preventing direct spark contact from cutting or unraveling thread loops.
Our standard MOQ for custom flux-cored gloves is 1,200 to 2,400 pairs per specification. This accommodates custom leather color matching, private brand debossing, customized woven label integration, and tailored size distribution (Size 8/M to 12/3XL).
Yes. We supply comprehensive testing dossiers through internationally accredited bodies (such as CTC, SATRA, and SGS) covering EN 388, EN 407, EN 12477 Type A, and ANSI/ISEA 105 protocols alongside our internal ISO 9001:2015 factory quality inspection data.
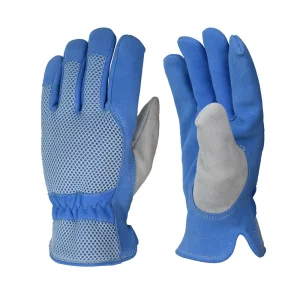
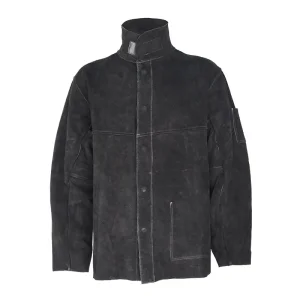
Comprehensive safety gear designed to build a complete thermal protection perimeter for welding teams, machine operators, and metallurgy craftsmen.