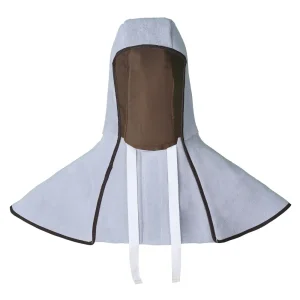
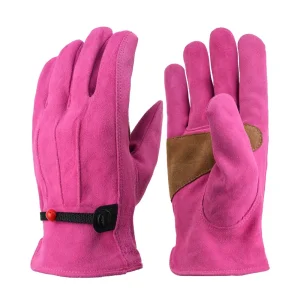
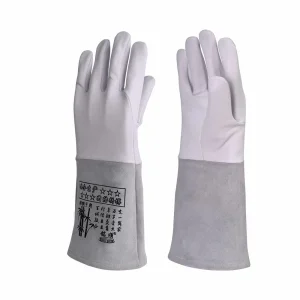
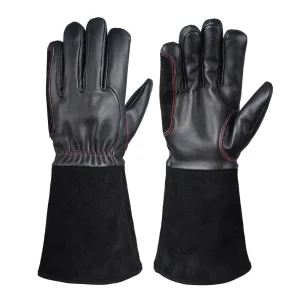
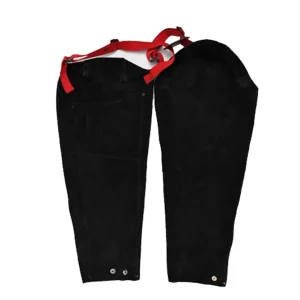
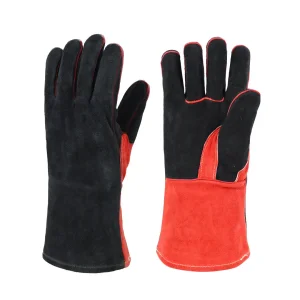
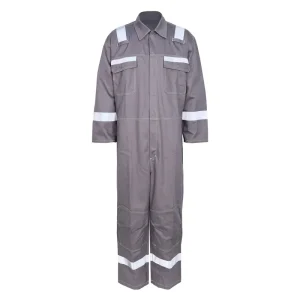
Built directly in our manufacturing facility, these select items provide extreme flame-retardant safety and equipment handling endurance for site engineers, line technicians, and workshop crews in Nairobi and Mombasa.
Kenya stands as the economic anchor and manufacturing powerhouse of East and Central Africa. Driven by the Vision 2030 development agenda, extensive infrastructure modernization is fueling unprecedented demand for robust electrical and mechanical cable protective solutions.
The Kenya Electricity Generating Company (KenGen) and independent power producers running deep drilling rigs in the Great Rift Valley subject electrical cables, hydraulic conduits, and instrumentation feeds to hydrogen sulfide (H2S) fumes, scalding geothermal brine, and abrasive silica soils. Ordinary PVC or non-reinforced conduits fail prematurely, making flame-retardant, chemical-resistant split cowhide and Kevlar-stitched cable covers mandatory for continuous uptime.
Under the LAPSSET corridor initiative and continuous expansion at the Kilindini Harbour, automated ship-to-shore gantry cranes, heavy welding barges, and repair shipyards operate 24/7. Cables dragging across rough concrete wharves undergo extreme friction and salt-spray UV degradation. Custom vulcanized ballistic sleeves and multi-layer cowhide cable sheathing mitigate expensive core line rupture risks.
The Standard Gauge Railway (SGR) connecting Mombasa, Nairobi, and Naivasha inland dry ports utilizes heavy maintenance rail-grinding and structural welding units. In open-air African sunlight with strong UV indices, conventional rubber sheathing succumbs to photo-oxidation, dry rot, and slag puncture. Industrial grade, flame-retardant flexible covers ensure long service life and high safety compliance.
A technical comparison of materials engineered to protect high-voltage welding power cables, hydraulic feed hoses, and automated production robot lines operating in harsh equatorial and dust-intensive environments.
| Material Class | Continuous Temp Range | Abrasion Resistance (Cycles) | Spatter & Flame Rating | Recommended Kenyan Application |
|---|---|---|---|---|
| Selected Split Cowhide Leather (1.2 - 1.4 mm) | -25°C to +260°C | > 12,000 cycles (ASTM D3884) | EN ISO 11611 Class 2 compliant | Structural welding yards in Nairobi, heavy shipyard fabrication in Mombasa |
| Ballistic High-Denier Cordura Nylon (1000D / 1680D) | -40°C to +130°C | > 25,000 cycles (ISO 12947) | FR treated, self-extinguishing (UL94 V-0) | Mobile cranes, logistics warehouse conveyors, robotic assembly cells |
| Aluminized Heat-Reflective Glass Composite | Up to +550°C radiant heat | Moderate (Requires outer split guard) | Non-combustible (ISO 15025 A) | Geothermal borehole heads, foundry taps, molten slag run-off zones |
| Hybrid FR Cotton / Leather Reinforced Sheaths | -10°C to +180°C | > 8,000 cycles | ISO 14116 Index 3 | Lightweight portable TIG/MIG torches, automotive body assembly shops |
Industrial-grade 50mm flame-retardant hook-and-loop fasteners allow retrofitting over installed cable runs without dismantling terminal lugs, while heavy-duty brass/nylon zipping provides sealed protection against the red volcanic dust prevalent in Nairobi and Thika.
All longitudinal and edge seams are stitched using 3-ply Kevlar heat-resistant thread (rated to 420°C). Ordinary polyester stitching unravels when hot molten globules land on cable bundles; Kevlar retains structural integrity across thousands of operating hours.
We manufacture continuous single-sleeve lengths from 3.8 meters (12.5 ft) up to 30 meters (100 ft), with internal diameters ranging from 25 mm (1") for handheld welding lines to 150 mm (6") for multi-conduit umbilical bundles used in drilling and deep-sea dredging.
Purchasing managers in Kenya face three relentless pain points: excessive shipping lead times, premature equipment degradation caused by counterfeit or sub-standard local market offerings, and cumbersome import verification procedures.
Replacing high-amperage, multi-core copper welding cables or multi-phase crane feed lines can cost thousands of USD per incident, not including the ruinous expense of facility downtime. A heavy-duty leather cable cover acts as an expendable, ultra-tough sacrificial barrier that extends internal cable life by 400% to 600%.
As a factory-direct manufacturer, we eliminate trading company markups and provide transparent freight logistics. We coordinate standard 20ft and 40ft containerized shipments direct from our deep-water port logistics partners to the Port of Mombasa, with direct rail transit inland to the Nairobi Embakasi Inland Container Depot (ICD).
We work closely with accredited international inspection agencies (such as SGS, Bureau Veritas, and Intertek) to execute the Pre-Export Verification of Conformity (PVoC) process required by the Kenya Bureau of Standards (KEBS). Shipments arrive with genuine Certificates of Conformity (CoC) to bypass customs bottlenecks.
From cement kilns in Athi River to tea factories in Kericho and naval ship repair in Mombasa, our custom cable covers deliver specialized protection where standard solutions fail.
Heavy clinker dust and high ambient kiln temperatures cause rapid abrasion to drag cables. Our 1.4mm chrome-tanned split cowhide sleeves feature tight-sealed hook-and-loop lips that prevent abrasive lime particles from penetrating into cable bundles.
High humidity and organic acid exposure in Western Kenya sugar mills (Muhoroni, Chemelil) and Kericho tea factories corrode electrical conduit joints. We manufacture water-repellent, oil-resistant ballistic nylon sheathing with sealed inner liners.
Open-pit mineral extraction involves jagged rocks and heavy vehicle runovers. Our multi-layer armored cable wraps combine an abrasion-resistant outer split cowhide layer with an interior cushioning elastomer, dramatically reducing pinch-point cable ruptures.
High-density SMAW and GMAW welding in industrial workshops creates high spatter density. Lightweight, flexible hybrid leather sleeves prevent weld spatter from fusing with ground and power leads, enhancing ergonomic operator mobility.
Our R&D engineering lab is pioneering new material composites and tracking integrations designed to withstand the increasingly automated future of African industrialization.
In response to international ESG directives and Kenyan environmental regulations overseen by NEMA (National Environment Management Authority), our facility is scaling trivalent-chromium-free and vegetable-retanned split hides, minimizing effluent footprint while increasing leather heat resilience.
For large contractors operating dozens of mobile generator banks and welding stations across major Kenyan construction corridors, our upcoming smart cable covers feature vulcanized UHF RFID tags for automated inventory tracking, inspection logging, and maintenance scheduling.
By infusing raw aramid fibers with microscopic ceramic particles, our latest developmental covers achieve an instantaneous temperature threshold exceeding 1,100°C. This breakthrough prevents burn-through even during high-amperage gouging and continuous plasma arc cutting operations.
Everything you need to know regarding custom sizing, material selection, KEBS compliance, shipping logistics to Mombasa, and OEM private-label production.
For custom cable covers and leather welding PPE, standard bulk manufacturing lead times run approximately 30 to 45 business days after prototype sample sign-off. Ocean transit from major Asian export terminals to the Port of Mombasa averages 18 to 24 days, with customs clearance typically taking 3 to 5 business days when utilizing our streamlined PVoC documentation package.
We coordinate directly with accredited inspection agencies including SGS, Intertek, and Bureau Veritas to perform Pre-Export Verification of Conformity (PVoC). We provide full laboratory test reports covering flammability resistance (EN ISO 11611), tensile strength, tear resistance, and non-toxicity to ensure issue of the mandatory Certificate of Conformity (CoC) prior to vessel departure.
Yes. As an OEM manufacturer, we tool custom cutting dies and patterns. We fabricate internal diameters from 20 mm up to 200 mm. Closure options include continuous 50mm flame-retardant hook-and-loop (Velcro), industrial-grade molded tooth zippers, corrosion-resistant brass press snaps, or lace-up eyelets for permanent heavy-duty bundle encapsulation.
Synthetic rubber and PVC harden, crack, and fail under intense equatorial ultraviolet radiation and ambient heat in open-air Kenyan job sites. When welding spatter lands on rubber, it burns through to the copper core immediately. Heavy split cowhide leather naturally insulates, resists burn-through up to 260°C continuous radiant heat, and withstands dragging over razor-sharp volcanic rock.
Our standard MOQ for custom dimension or branded cable covers (incorporating debossed leather logos, heat-transferred company emblems, or custom color fabric accents) starts at 300 to 500 meters depending on the material class. For mixed container orders containing welding PPE apparel and cable accessories, flexible tiered quantities are accommodated.
Yes. Through our freight forwarding partners, we provide comprehensive bill-of-lading solutions terminating at Mombasa (CIF Mombasa) or bonded multimodal transit via the Standard Gauge Railway direct to the Inland Container Depot (ICD) in Nairobi, as well as cross-border transshipment solutions into Uganda and Rwanda.
Integrate full-system safety gear alongside your custom cable cover order. Direct from our factory floor to your job sites in Nairobi, Kisumu, Eldoret, and Mombasa.