
Direct-from-factory protective gear built from Grade-A split suede cowhide, heat-shielded composites, and DuPont™ Kevlar® stitching.
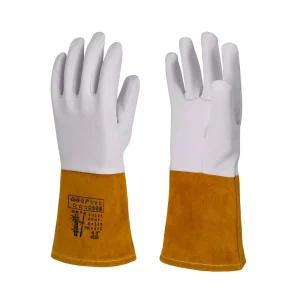
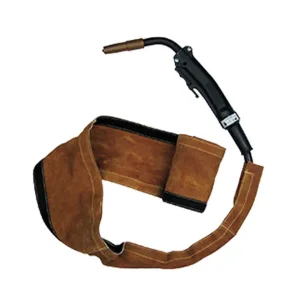
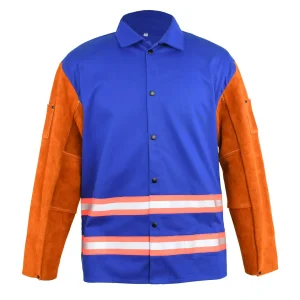
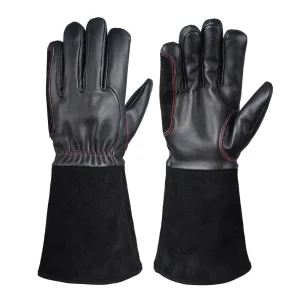
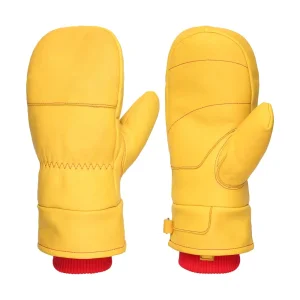
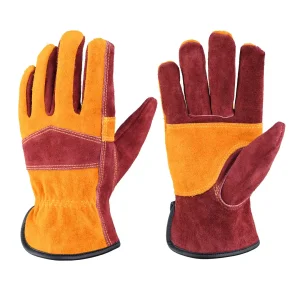
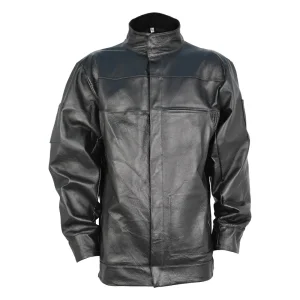
Understanding dermal fiber density, collagen interlocking, and spatter deflection physics in extreme welding environments.
Unlike grain leather that hardens and curls when exposed to intense radiative flash, split cowhide suede features an open fibrous mesh. This fibrous texture disperses molten globules instantly, creating zero bounce-back into operator neck crevices or lapel voids.
We enforce strict split caliper calibration. Our suede welding jackets never fall below 1.2mm in heavy impact sectors (chest, shoulders, forearm drapes). This provides critical delay times against heat transmission, surpassing EN ISO 11611 Class 2 parameters effortlessly.
Structural integrity depends on thread chemistry. Conventional nylon disintegrates at 210°C, causing seam blowouts. Ming Shun builds every suede garment with 3-ply and 4-ply DuPont™ Kevlar® bonded filaments resistant to carbonization up to 425°C.
| Performance Characteristic | Ming Shun Split Cowhide Suede | Standard Grain Cowhide | Flame-Retardant Cotton (9-11oz) |
|---|---|---|---|
| Spatter Roll-Off Resistance | Extreme (Micro-fibers catch & freeze drops) | Moderate (Can slide into folds) | Low (Subject to local pinhole burn-through) |
| Radiative Thermal Insulation | Superior (0.13 W/m·K low conductivity) | Moderate (Conducts faster once saturated) | Light (Requires active standoff space) |
| Tear & Tensile Strength (ISO 13934) | > 450 N (Multi-directional fiber tangle) | > 520 N (Unidirectional strength) | 120 - 180 N (Woven matrix constraints) |
| Target Industrial Worksite | Heavy Fabrication, Structural MIG, Shipyards | Moderate Fabrication, Automated Cells | Inspection, TIG, Ambient Warm Climates |
Real-world operational configurations where specialized suede welding outerwear delivers tangible risk mitigation.
Constrained hull spaces require overhead flux-cored arc welding (FCAW). In this posture, molten slag falls directly on the chest and arms. Suede jackets with standing mandarin collars prevent slag ingress into basal cervical skin.
Extreme field variations in the Permian Basin, North Sea, or Middle East demand jackets capable of withstanding rough pipe edges, grit, and repeated friction without delamination or premature tearing along sleeve seams.
Erecting massive I-beams and high-amperage submerged arc setups produces sustained intense radiant thermal energy. Suede cowhide provides natural UV insulation, completely preventing radiation erythema (arc eye/skin burn).
In furnace tapping environments where temperatures exceed 1,400°C, our suede jackets integrate under-arm gussets with aluminized heat shields (MS-106T compatibility) to deflect extreme infrared radiant load.
Eliminating trading intermediaries through complete vertical integration: From wet blue hide processing to robotic cutting and automated snap installation.
We avoid spot-market raw splits. In our Gaozhou production base, we monitor chromium tanning stages to preserve natural collagen integrity, ensuring pH neutrality (3.5 - 5.0) to prevent occupational dermatitis for welders.
Eliminate human variance in ergonomic panel fitting. Hydraulic traveling head cutting presses shape suede panels with 0.5mm tolerances. This avoids loose underarm bunched leather that can catch flying sparks.
With over 1,000 skilled line operators and our own raw material reserves, Ming Shun maintains dependable schedule certainty. We buffer container shipments reliably, mitigating raw hide price spikes for brand partners.
Delivering verifiable audit reports for strict import regimes in the EU, North America, Australia, and GCC nations.
Fully tested against small droplets of molten metal (≥ 25 drops for Class 2) and radiant heat transfer (RHTI 24 ≥ 16s). All non-conductive snaps are insulated with split leather under-flaps to meet EN standards.
Conforms with OSHA 1910.252 personal protective equipment directives for thermal resistance and electrical resistance (zero exposed exterior conductive hardware to prevent shock during arc initiation).
Total azo-dye ban adherence, aromatic amine testing below detection thresholds, and strict Hexavalent Chromium [Cr(VI)] containment below 3.0 mg/kg verified by third-party testing partners (SGS / Intertek).
How Ming Shun is solving traditional split leather weight, heat-retention, and ergonomics via modern composite engineering.
Combining 1.3mm suede in front impact zones with 9oz breathable, high-tear FR satin-weave cotton in back shoulders (as seen in our MS-1260 series) to decrease whole-body thermal fatigue by 38% during long shifts.
In development: micro-encapsulated ceramic surface treatments that resist repeated direct molten immersion, doubling the abrasion lifespan without increasing hide weight or diminishing pliability.
As heavy fabrication embraces passive lifting exoskeletons, our pattern division is updating shoulder pivots, sleeve tapers, and waist drawstrings to integrate smoothly over mechanical joints.
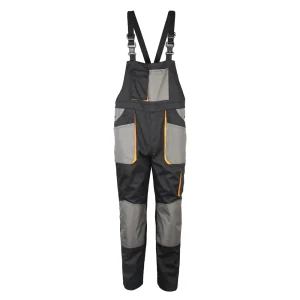
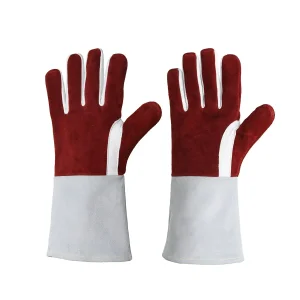
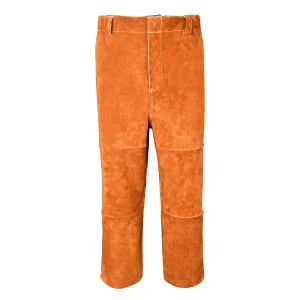
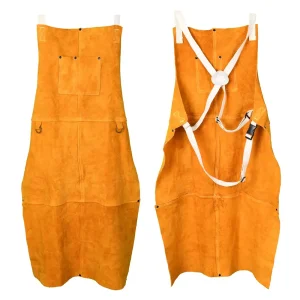
Complete head-to-toe welder protection from Ming Shun's dedicated production lines.
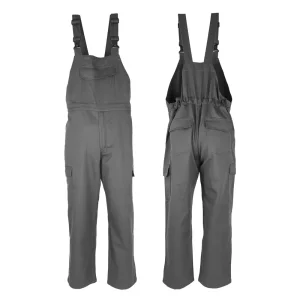
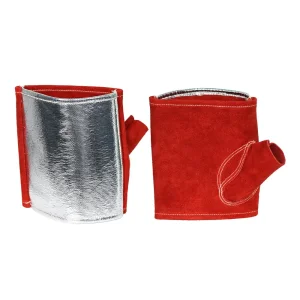
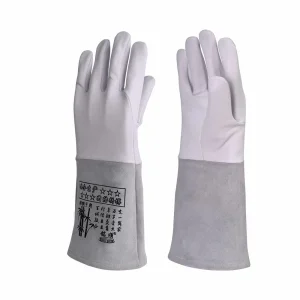
Clear answers on minimum orders, customized patterns, hide grading, and delivery logistics.
For OEM private-label production (custom cut, woven labels, heat-stamped brand embossing), our standard starting volume is 500 units per jacket style. For trial distributor orders containing mixed stock lines (aprons, gloves, hoods), we support flexible test batches starting at 200 units.
Caliper consistency is critical. Standard industry hides often vary unpredictably between 0.9mm and 1.6mm across a single garment. Ming Shun enforces precision drum milling to maintain an exact 1.2mm–1.4mm profile. This delivers optimal structural thermal protection while keeping the suede soft and pliable, minimizing shoulder and arm fatigue during multi-hour overhead jobs.
Yes. Our MS-1260 series utilizes split suede cowhide on the sleeves, shoulders, and chest bib—where hot spatter impacts most frequently—while employing 9oz or 7oz breathable flame-retardant cotton for the back panels. This reduces weight while ensuring adequate ventilation in tropical shipyards.
Following pre-production sample sign-off and tech-pack lock, a 40ft HQ container (approx. 4,500 to 6,000 complete suede welding jackets, or mixed container loads) completes manufacturing within 35 to 45 business days. FOB dispatch is handled swiftly via Shenzhen or Guangzhou ports.
