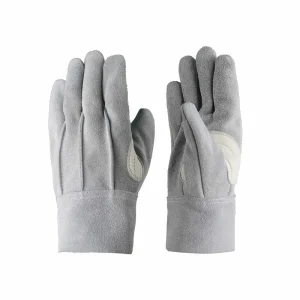
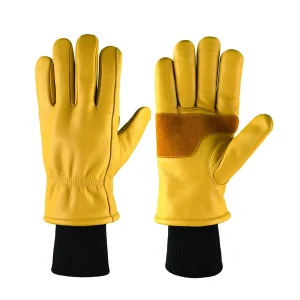
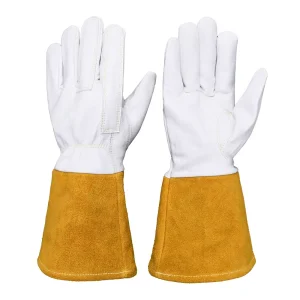
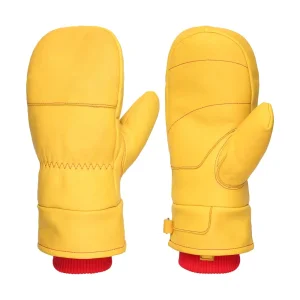
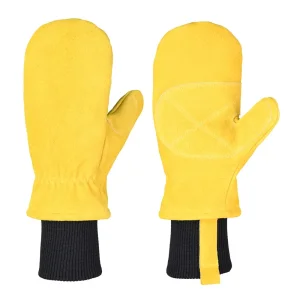
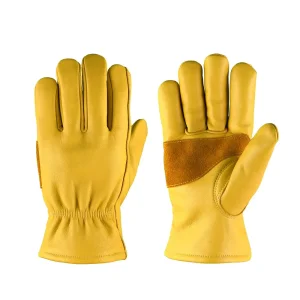
Explore our engineering-grade cold-resistant work mittens, winter cowhide protection, and heavy-duty leather safety solutions directly exported to worldwide enterprise partners.
Analyzing thermal dissipation barriers, contact chill transfer limits, and vapor-barrier engineering tailored to withstand extreme sub-zero ambient operating environments.
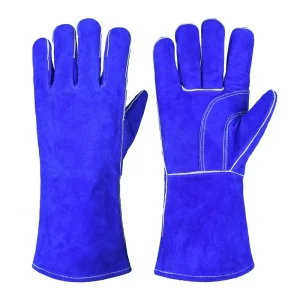
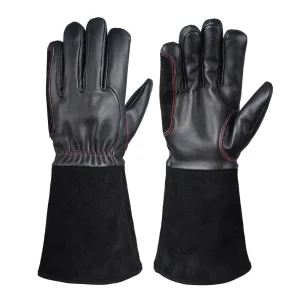
Cold-resistant safety gear requires impervious outer membranes. Using specialized water-resistant treated cowhide and goatskin, our gloves maintain high tactile sensitivity without absorbing moisture that leads to rapid convective freezing and structural leather brittleness.
Incorporating multi-denier aerated synthetic linings and 3M™ Thinsulate™ micro-matrix layers, thermal energy is isolated within micro-chambers. This prevents conductive loss when operators grip sub-zero metal pipes, tools, or cryogenic valves down to -50°C.
Every cold protection model strictly satisfies EN 511 standard testing across Convective Cold (0-4), Contact Cold (0-4), and Water Penetration (0-1). Seamless finger crotches combined with ergonomic keystone thumbs prevent operator hand fatigue during continuous 8-hour shifts.
Deploying application-matched thermal PPE tailored to the unique physical abrasion, contact chill, and oil/gas splash risks of modern heavy industries.
Handling liquefied nitrogen (-196°C) and LNG requires cryogenic protection equipped with vapor membranes that prevent splash ingress, frostbite blistering, and brittle structural tearing during valve transitions.
Automated refrigerated storage (-25°C to -35°C) demands tactile grip for barcode scanning and pallet manipulation. Fleece-lined cowhide construction balances thermal longevity with dexterity.
Offshore rigs and sub-polar mining environments expose work crews to wind chill, saltwater spray, and heavy mechanical impacts. Integrated Kevlar® stitching resists abrasive rock and hydraulic oil degrade.
Operating from our expansive industrial complex in Gaozhou, Guangdong, Guangdong Ming Shun Labour Protective Products Co., Ltd. eliminates intermediary risks through comprehensive vertical integration.
With an active workforce of 1,000+ skilled personnel, our manufacturing footprint includes dedicated raw hide sorting, in-house leather tanning and dyeing, automated laser cutting tables, and specialized thermal lamination machinery.
| Production Dimension | Ming Shun 4.0 Capability | Procurement Benefit |
|---|---|---|
| Leather Processing | 100% In-House Tanning & Dyeing | Zero batch-to-batch color or thickness delta |
| Glove Assembly Output | 500,000+ Pairs / Month | Guaranteed volume scalability for multi-branch distributors |
| Production Lead Time | Standard ~45 Days Post-Approval | Clear project timelines and scheduled quarterly shipments |
| Defect Prevention | 4-Stage In-Line Quality Gates | AQL 1.5 standard compliance on seam tension & insulation |
Our engineering division transforms complex buyer tech packs into production-ready patterns within 7 working days. By eliminating trading intermediaries, OEM buyers achieve up to 18-24% unit cost advantages while maintaining strict Western audit certifications.
Whether your distribution network requires customized thermal linings (fleece, acrylic, Thinsulate™), specific gauntlet safety lengths, or private-label embossing, our team delivers consistent quality.
Mitigate customs delays and regulatory liabilities. We supply complete CE Documentation, technical files, and authorized test certifications tailored to destination markets.
Full CE certification coverage for Category II PPE. In-house verification ensures non-detectable levels of Hexavalent Chromium (Cr VI), pH skin neutrality, and certified thermal insulation factors.
Thermal contact testing down to sub-zero conditions alongside ANSI puncture, abrasion, and cut performance ratings required by large American industrial procurement chains.
Our Gaozhou engineering and trade team provides English-native technical dialogue, real-time container packing updates, OEM barcodes, and accurate HS Code classification (e.g., Chapter 42).
Ming Shun's ongoing R&D investments target next-generation materials designed to eliminate bulk, maximize heat retention, and support corporate ESG decarbonization targets.
Integrating silica aerogel composite textiles into high-risk contact zones (palms and fingers) to achieve unparalleled thermal barrier protection with a 40% reduction in glove thickness, unlocking unprecedented finger dexterity.
Developing specialized carbon-infused leather grain finishes capable of activating industrial touch displays in cold storage hubs without requiring operators to take off their gloves and expose skin to thermal shock.
Advancing our proprietary chrome-free organic vegetable tanning technologies and water recycling loops to lower Scope 3 procurement emissions for multinational safety equipment brands.
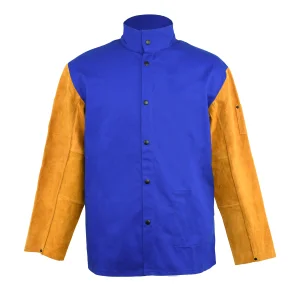
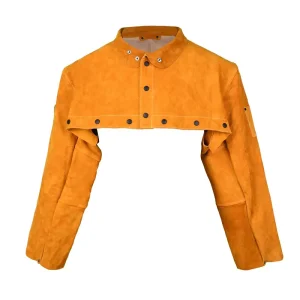
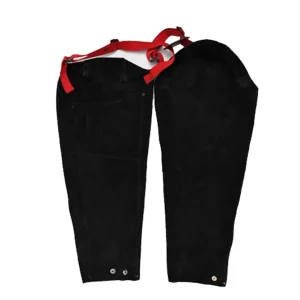
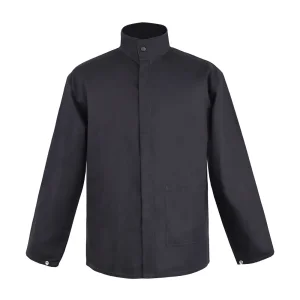
Order factory-direct thermal work gloves, heavy fabrication leather jackets, and multi-hazard FR clothing with customized bulk logistics.
In-depth responses covering quality control criteria, sample customization, supply chain transparency, and delivery assurances.
We combine high-tensile goatskin or soft split cowhide with zoned micro-fleece and 3M™ Thinsulate™ lining. By engineering thinner palm layers and thicker dorsal insulation, our gloves achieve verified EN 511 convective cold barrier protection while preserving the finger dexterity needed for tooling and hardware handling.
Every shipment is backed by verified CE EN 388 (mechanical risk), EN 511 (cold protection), and EN ISO 11611/EN 12477 test reports where applicable. Our products comply with REACH chemical limits (including Chromium VI <3ppm and azo dyes). Full compliance documentation is issued prior to container dispatch.
Yes. As a factory with dedicated patterning rooms, we support heat-transfer logos, leather debossing, woven branding, and retail hangtags. We also engineer custom size profiles (XS through 4XL) configured to regional ergonomic expectations (European vs. North American sizing standards).
Our glove manufacturing lines exceed 500,000 pairs monthly. Typical bulk production takes around 45 days after tech pack and sample sign-off. Standard MOQs start at 1,200 to 2,400 pairs per style, with sample development completed within 5-7 working days.