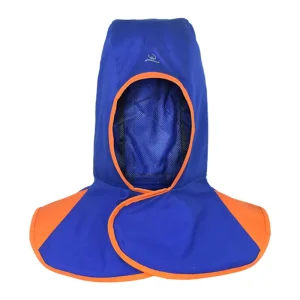
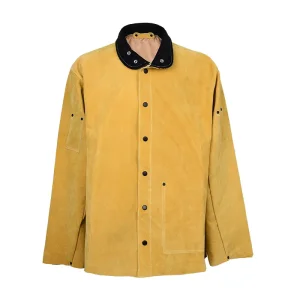
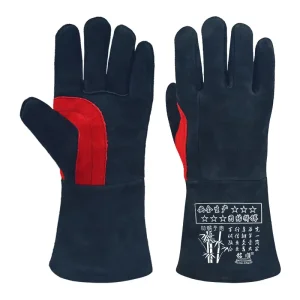
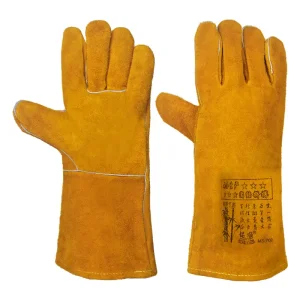
Direct contract manufacturing solutions designed for heavy-duty molten splash resistance, arc-flash barrier defense, and precision mechanical durability.
Eliminating historical safety liabilities caused by downscaled unisex garments through true anthropometric design, advanced thermal boundary physics, and ergonomic articulation.
Across modern heavy industrial ecosystems—ranging from commercial shipbuilding yards, nuclear pressure vessel construction, and automated automotive manufacturing to orbital aerospace fabrication—the participation of women in precision welding and technical hot work has escalated by more than 38% over the past decade. Despite this demographic evolution, a massive safety vulnerability has persisted across global supply chains: the systemic reliance on the outdated "shrink it and pink it" manufacturing mentality. Historically, procurement teams merely provisioned smaller-sized men's protective apparel, fundamentally misunderstanding the biomechanical and morphological distinctions of female welders.
When a female welder wears an ill-fitting unisex jacket, the consequences exceed aesthetic discomfort: loose shoulder draping causes the thermal barrier to shift, exposing the neck and clavicle to stray molten slag; excessive sleeve volume catches sparks inside folds; dropped armhole seams severely constrain overhead torch manipulation in 4G and 6G positions, accelerating physical fatigue and elevating musculoskeletal disorder risks; and boxy waistlines fail to seal around safety harnesses, allowing radiant arc heat to penetrate underlayers. Our dedicated engineering division solves this macro crisis through precision-tailored OEM Women's Welding Jackets, merging true anthropometric grading with heavy industrial compliance.
Engineered with targeted bust circumference darting, shortened torso drop lengths, and tapered waist contours that eliminate fabric pooling while accommodating chest curves without structural fabric tension.
Features curved sleeve profiling and underarm gussets configured for dynamic torch maneuvers. Allows full 180-degree overhead rotation without raising the bottom hem or exposing the abdominal midline.
Utilizes precision split cowhide (1.1–1.3 mm) reinforced along high-risk strike zones (chest, forearms, collar) paired with flame-retardant 9 oz/11 oz breathable sateen cotton on low-exposure dorsal zones.
In-depth technical overview of raw material grades, stitching tensile tolerances, dielectric closure hardware, and multi-risk barrier construction.
| Component Zone | Material Specification | Thermal & Mechanical Performance | OEM Customization Options |
|---|---|---|---|
| Primary Shell (Front/Arms) | A-Grade Heavy Split Cowhide (1.1 - 1.3 mm) or Lightweight Premium Pigskin | EN ISO 11611 Class 2 molten splash resistance; puncture resistance ≥ Level 3 | Custom drum dyeing (Graphite Grey, Safety Red, High-Viz Orange, Navy) |
| Secondary Shell (Dorsal) | Flame-Retardant 9 oz or 11 oz 100% Breathable Sateen Cotton Fabric | Self-extinguishing char length < 100 mm (ASTM D6413); arc rating 8.6 cal/cm² | Water-repellent coating, anti-static carbon filament weaving, hi-vis tape |
| Structural Seams | 100% Para-Aramid (Kevlar®) 3-Ply & 4-Ply Heavy-Duty Thread | Non-melting up to 450°C (842°F); superior seam tensile shear ≥ 400 N | Concealed safety welted seams, double-row edge lock reinforcement |
| Closure System | Black Oxidized Dielectric Metal Snaps with Insulated Leather Shield Flap | Zero electrical conductivity; prevents molten metal bridge ignition | Hook-and-loop secondary FR seal, heavy-duty brass YKK zipper insert |
| Collar & Cuffs | Dual-layer stand-up Mandarin collar; internal snap-adjustable wrist cuffs | 360-degree thyroid & carotid burn barrier; prevents slag ingress to forearms | FR knit moisture-wicking inner collar liner, spatter-resistant cuff gauntlets |
Comprehensive regulatory alignment safeguarding tier-1 contractors, EPC firms, and safety apparel distributors across key global commercial jurisdictions.
Full conformance with OSHA 1910.132 PPE standards, ANSI/ISEA 105 mechanical cut/puncture testing, and ASTM F1506 / NFPA 70E compliance for multi-hazard arc flash environments.
Certified under PPE Regulation (EU) 2016/425, complying with EN ISO 11611:2015 (Class 1 & Class 2 A1+A2) for thermal spatter, and EN ISO 11612 for radiant convective heat deflection.
Manufactured to fulfill AS/NZS 4824 protective clothing benchmarks and AS/NZS 4501.2 specifications for heavy industrial metallurgical operations, mining sites, and railway infrastructure.
Operates under verified ISO 9001:2015 quality frameworks. Comprehensive traceability with batch testing of dye crocking, leather pH balance, chromium VI thresholds, and dimensional stability.
Addressing distinct thermal profiles, physical friction variables, and mobility needs across specialized commercial production fields.
High-volume robotic cell integration requiring agile torch access, arm flex resistance, and lightweight hybrid torso construction for continuous repetitive duty cycles.
High-amperage flux-cored arc welding (FCAW) in tight double-bottom tanks, requiring heavy-duty split cowhide collars, abrasion resistance, and anti-corrosive brass snaps.
Micro-TIG and orbital welding of titanium and Inconel ducting. Prioritizes ultra-clean pigskin leather sleeves to prevent static transfer, shedding, or surface contamination.
On-site pipeline maintenance characterized by dual risks of hydrocarbon flash fire and molten sparks, demanding NFPA 2112/70E-certified hybrid garments with quick-release snaps.
Exposed high-altitude wind and overhead gouging conditions. Equipped with drop-tail lumbar panels and harness pass-through slots engineered for secure fall-arrest lanyard tie-offs.
How our advanced R&D initiatives are incorporating graphene thermodynamics, modular active cooling, and circular chrome-free recycling systems.
Developing lightweight hybrid weave blends embedding exfoliated graphene nanoplatelets to dramatically elevate conductive heat dissipation while dropping overall garment weight by up to 32%.
Investing in heavy-metal-free vegetable-synthetic re-tanning that eliminates Hexavalent Chromium risks, coupled with zero-landfill scrap downcycling programs for composite leather backing pads.
Field-testing integrated low-profile passive biometric sensor channels that monitor skin microclimate temperature and humidity in real-time, communicating critical heat-stress alerts via worker smart beacons.
Comprehensive procurement, compliance, and custom design details for B2B importers, safety brands, and commercial supply chain directors.
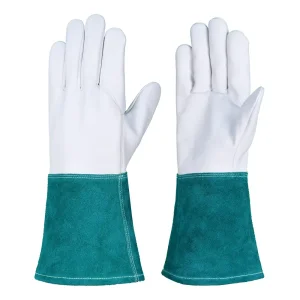
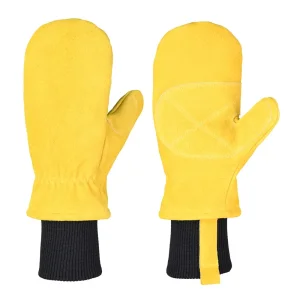
Comprehensive secondary protective gear, protective sleeves, cold-weather options, and hand protection systems for integrated industrial supply lines.