Precision gauntlet solutions, flame-retardant hybrid fabrications, and full-grain cowhide systems manufactured under direct factory ISO 9001 quality management.
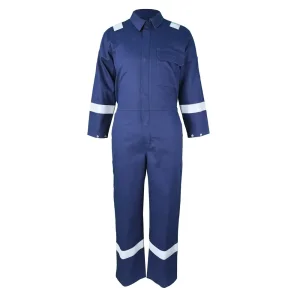
OEM MS-315 Navy 7 oz AR/FR Cotton Coverall Manufacturer, Supplier
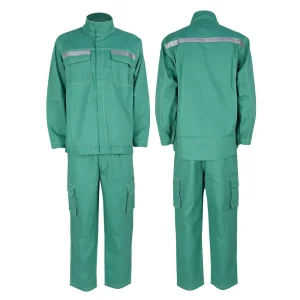
Wholesale MS-F313 FR Welding Suit Set with Reflective Tape Supplier, Suppliers
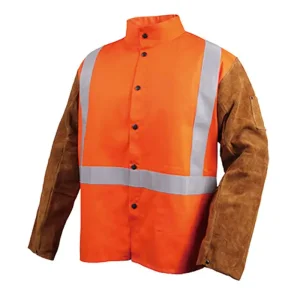
OEM MS-324 Hi-Vis FR Cotton & Cowhide Hybrid Welding Jacket Manufacturer, Factories
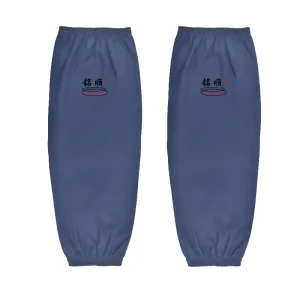
Wholesale MS-180B FR Welding Sleeves with Elastic Cuffs and Snaps Supplier, Suppliers
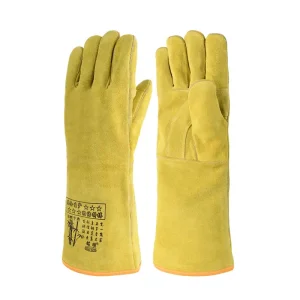
Wholesale MS-808 Heavy-Duty Split Cowhide Welding Gloves, Long Gauntlet Supplier, Factories
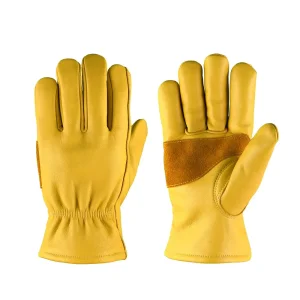
Custom MS-935 Water-Resistant Leather Work Gloves with Slip-On Cuff Manufacturers, Factories
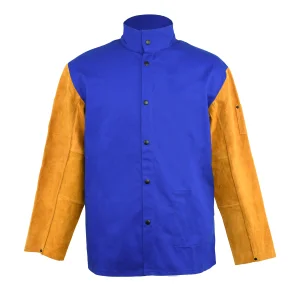
Wholesale MS-1260 9oz FR Cotton Hybrid Leather Sleeve Welding Jacket Manufacturers, Factories
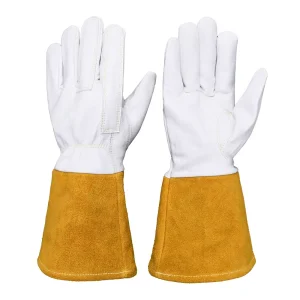
Wholesale MS-862 Premium Goatskin TIG Welding Gloves Factories, Factory
Integrating vertical tanning infrastructure, automated cutting systems, and real-time inventory buffers to eliminate delivery volatility for tier-1 distributors.
By housing raw hide sorting, chrome-free retanning, and aniline-grade drum dyeing within regional production hubs in Gaozhou, Guangdong, our OEM operations remove 15-20% lead-time variance common with multi-tier broker sourcing models. Tensile integrity, pH balance, and moisture metrics remain locked across production years.
Tensile: >15MPa | Shrink Temp: >100°CAutomated hydraulic clicking presses and digital oscillating knife plotters guarantee dimensional accuracy across thumb keystones, gunn-cut palms, and extended gauntlet cuffs. Eliminating manual shear variances ensures exact thread seam allowances, directly preventing micro-tears under high mechanical stress.
Tolerance: ±0.5mm Pattern PrecisionWe retain multi-container inventories of calibrated A/B-grade cowhide splits, goat grain skins, and DuPont Kevlar stitching threads directly on-site. Global procurement managers mitigate raw hide market price volatility through customized 6-to-12 month delivery call-off arrangements with locked cost baselines.
Dual-Warehouse Staging SystemWelding PPE selection is driven by energy transfer rates, secondary molten metal splash potential, and duty cycles across distinct heavy-industrial sectors.
Sustained high-amperage Submerged Arc Welding (SAW) and Flux-Cored Arc Welding (FCAW) generate massive radiant heat. Recommended: 1.3-1.5mm cow split gauntlets with aluminized back-hand shields and full Kevlar welting to prevent seam ignition from continuous sparks.
Confined-space hull repair demands moisture-resistant finishes paired with extreme cut protection. Gauntlets feature oil-tanned water-repellent leather shells, flame-resistant fleece interior linings, and extended 200mm split cowhide cuffs protecting radial arteries.
Manual touch-up stations along automated MIG lines require dexterous handling of thin-gauge components. Hybrid cowhide/grain goatskin models allow micro-control of the torch trigger while retaining an ANSI Level 3 abrasion barrier against stamped metal burrs.
TIG root runs demand absolute tactile sensitivity. Gauntlet architectures feature premium top-grain goatskin index and thumb sections joined to rigid split cowhide gauntlet sleeves that stand open to vent convective heat and allow instant emergency egress.
Material engineering thresholds and future-facing compliance criteria designed for procurement specifications.
| Evaluation Parameter | Standard Split Cowhide | Premium Grain Goatskin Hybrid | Aluminized Radiant Shield Tier | Next-Gen FR Nanofiber Composite |
|---|---|---|---|---|
| Primary Target Process | SMAW (Stick), Heavy MIG (GMAW) | High-Precision GTAW (TIG) | Heavy Foundry, High-Amp SAW | Robotic Plasma / Laser Welding |
| Contact Heat Threshold | 250°C (EN 407 Level 2) | 100°C (EN 407 Level 1) | 500°C (EN 407 Level 4) | 350°C (EN 407 Level 3) |
| Radiant Heat Reflection | Low (~15-20% attenuation) | Minimal (<10%) | Ultra-High (>92% Ray Reflection) | High (~65% Ceramic Diffusion) |
| EN 388 Mechanical Profile | 4-1-4-3-X (High Tear Resistance) | 2-1-2-1-X (Extreme Dexterity) | 4-2-4-4-X (Structural Density) | 4-X-4-3-D (Cut Level D Integration) |
| Stitching Tensile Integrity | 3-Ply Kevlar® Welted Seams | Para-Aramid Core-Spun Threads | Kevlar® Wrapped Stainless Wire | Laser-Welded Ceramic Polymer Hybrid |
| Ergonomic Dexterity Index | Level 1 - Level 2 (Stiff Shield) | Level 4 - Level 5 (Fingertip Touch) | Level 1 (Rigid Deflection) | Level 4 (High Articulation) |
Eliminate supply risks through verifiable, certified PPE manufacturing adhering to key international legal benchmarks.
All welding gauntlets designated for EU markets hold Module B Type-Examination Certificates from accredited notified bodies (e.g., SATRA, CTC). Compliant with EN 12477:2001+A1:2005 (Type A & B classification), EN ISO 11611, and strict REACH Annex XVII restrictions on Chromium VI, Azo dyes, and extractable heavy metals.
Product designs conform to ANSI/ISEA 105 standards covering puncture resistance, thermal degradation, and ASTM F1060 conductive heat transfer resistance. Chemical testing ensures total compliance with California Proposition 65 thresholds for clear domestic container customs clearance.
Our manufacturing footprint maintains ongoing SEDEX (SMETA 4-Pillar) and BSCI compliance. International brand owners receive batch-level leather lot tracking, ethical labor verification, and full documentation to support their corporate Environmental, Social, and Governance (ESG) mandates.
From initial 3D digital patterns to custom-branded retail packaging, our OEM process accommodates large-scale private label programs.
CAD tailoring ensures compliance with international sizing models (EU 7-12, US S-XXXL) with customized keystone or wing-thumb layouts designed to eliminate seam rub.
Rapid physical prototyping with verified leather thickness gauges, thread tensile verification, and customized brand debossing completed in 7-10 business days.
Direct thermal transfer, foil stamping, high-density woven labeling, silicon grip imprints, and customized multi-lingual retail header cards configured for retail display.
Formal AQL 1.5/2.5 inspection protocols verify leather grain consistency, seam density (4-5 stitches/cm), pull-tab strength, and gauntlet cuff stiffness before carton packing.
Consolidated palletization, moisture-barrier poly-bagging, desiccant integration, barcoded master cartons, and direct customs coordination for hassle-free port arrivals.
Clear technical insights directly from our lead production engineers and global account management specialists.
Shoulder-split cowhide provides an ideal balance of dense fiber structure, abrasion resistance, and flexibility, making it the industry standard for general MIG/stick welding. Belly splits are softer but display loose fiber density, shortening life under intense spatter. Premium grain goatskin offers superior tactile control for TIG wire feeding, but must be paired with cowhide gauntlet cuffs to protect forearms from ambient heat and UV rays.
Standard nylon and polyester threads melt around 200°C-250°C, leading to structural seam separation in the field. Our welding gauntlets are stitched with 100% genuine DuPont Kevlar® or equivalent para-aramid continuous filament threads, which remain stable up to 425°C without carbonizing. Leather welting is inserted across all high-wear seams to shield the stitching from direct contact with slag and molten sparks.
Yes. Our OEM division handles private-label production programs for prominent global brands. We offer customized heat-embossing, laser etching, screen printing, woven brand labels, and custom-designed hanging cards or individual retail polybags. Outer shipping cartons can be pre-printed with your exact barcodes, QR tracking labels, and internal inventory stock codes.
Standard factory MOQ is 1,200 pairs per style/size for custom-branded orders, which aligns with optimal leather hide yield and dyeing runs. For existing standard designs in our catalog, lower trial minimums can be arranged. Bulk container shipments typically ship within 40 to 50 days following sample sign-off and deposit receipt.
Heavy aluminized heat shields, precision TIG cowhide configurations, and full head-to-toe flame-resistant protective equipment.
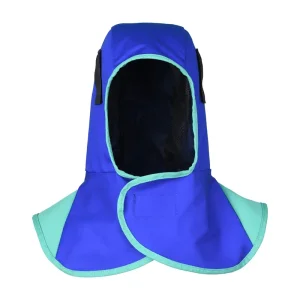
Custom MS-303B FR Welding Hood with Full Neck Flap Protection Suppliers, Factory
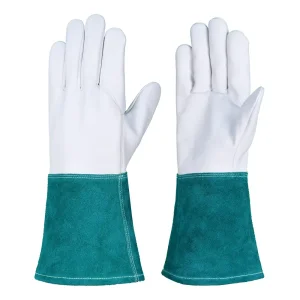
OEM MS-W874G Premium TIG Welder Gloves for Precision Control Manufacturers, Factory
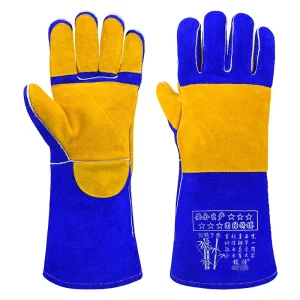
Custom MS-815 16" Cowhide Welding Gloves with Double Palm Manufacturer, Supplier
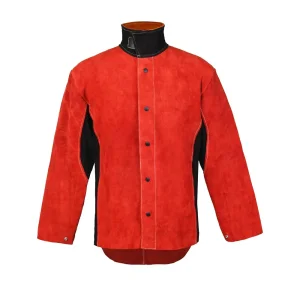
OEM MS-281 Red Split Cowhide Leather Welding Jacket Manufacturers, Suppliers
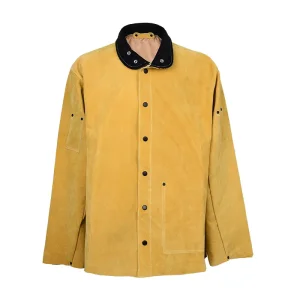
Wholesale MS-406 Lightweight Pigskin Leather Welding Jacket Manufacturer, Factory
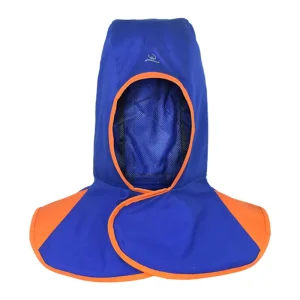
Custom MS-303O Flame-Resistant Cotton Welding Hood with Neck Coverage Manufacturer, Factories
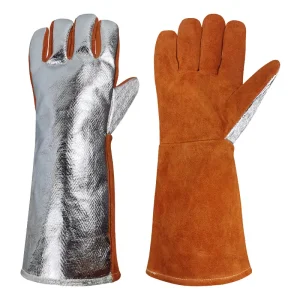
Custom MS-738O Aluminized Leather Heat Resistant Welding Gloves Supplier, Suppliers
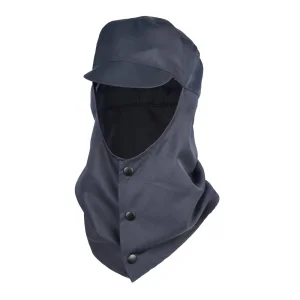
Wholesale MS-301L FR Welding Hat with Extended Neck Protection Manufacturers, Factory

