Engineered for extreme thermal resistance, molten spatter deflection, and precise ergonomic compliance under high-amperage environments.
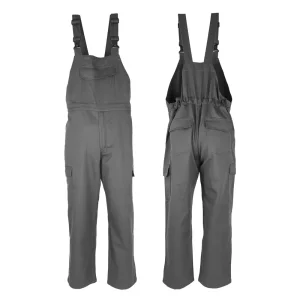
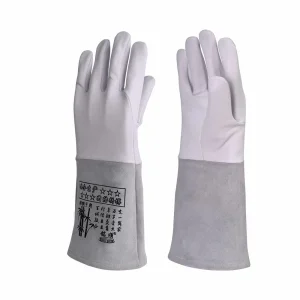
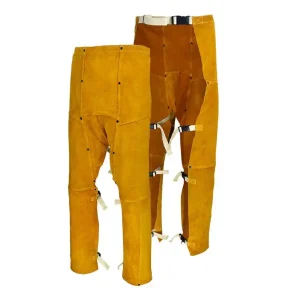
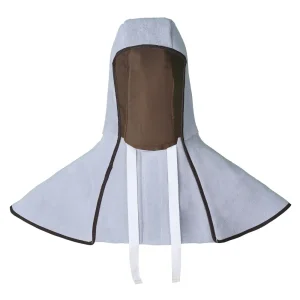
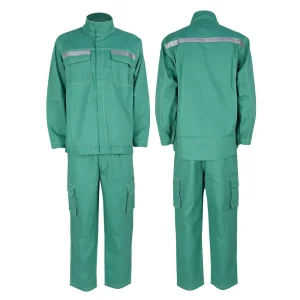
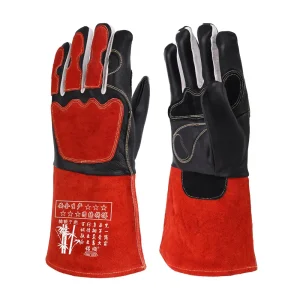
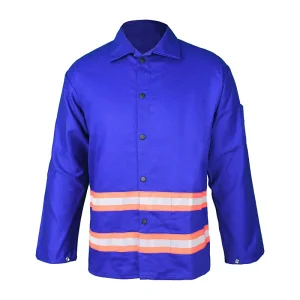
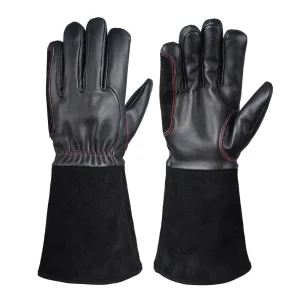
Evaluating the direct macroeconomic and technical advantages of vertically integrated leather production hubs in Guangdong, China.
Unlike third-party stitchers, sourcing directly from Gaozhou manufacturers provides raw hide selection, precision splitting (1.1mm to 1.4mm grade A split cowhide), and proprietary chrome or vegetable tanning within the same facility footprint. This eliminates tensile shear variance and batch discolouration entirely.
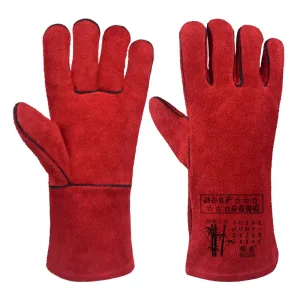
Every gauntlet cuff features engineered rigidity—from rubberized safety cuffs to laminated split-leather sleeves—stitched completely with DuPont™ Kevlar® heat-resistant filament. Stress-bearing seams integrate leather welting to shield thread integrity from continuous direct flame and molten spatter exposure.
Direct Chinese enterprise production is optimized to meet the most stringent compliance benchmarks in North America and the European Economic Area: ISO 9001 quality infrastructure, EN 388:2016 (abrasion, cut, tear, puncture), and EN 12477:2001 Type A and Type B standards for heavy welding execution.
Analyzing the shifts from basic hand protection to advanced, multi-hazard, ergonomically responsive leather gauntlet systems.
Modern industrial gauntlets fuse durable split cowhide cuffs with goatskin or deerskin palms, balancing intense forearm slag deflection with fingertip tactility demanded by high-frequency TIG automation operations.
Shifting away from coarse unlined interiors, modern specifications demand non-woven flame-retardant fleece, aluminized back-hand heat shields, and moisture-wicking antimicrobial air-mesh inner layers.
Eliminating continuous worker hand fatigue, new OEM gauntlets leverage continuous thumb, 3D pre-curved finger cuts, and extended seamless palm designs that conform directly to natural muscular resting states.
International environmental regulatory standards (EU REACH Annex XVII) mandate trivalent chromium passivation, SVHC-free leather dyeing, and strictly monitored total immersion wastewater extraction.
Technical performance configurations mapped across hazardous operational parameters.
| Industrial Sector | Primary Thermal / Kinetic Threat | Recommended Leather & Cuff Geometry | Protective Reinforcement Layer | Regulatory Target |
|---|---|---|---|---|
| Heavy Steel Fabrication & Shipyards | Extreme molten splash, continuous slag, mechanical abrasion | 1.3mm Premium Split Cowhide with 14"-16" Rigid Gauntlet | Full Welted Seams, Kevlar® 4-Ply Stitching | EN 12477 Type A |
| Automated Pipe Welding & Pressure Vessels | Sustained radiant arc heat, sharp-edge bevel contact | Grade-A Grain Cowhide Palm + Split Leather Cuff Extension | Aluminized Back Hand Pad Integration | EN 407 413X4X |
| Precision Aerospace TIG Welding | Fine electrical arc, high radiant heat, dexterity sensitivity | Top-Grain Goatskin with Lightweight Leather Gauntlet Cuff | Wrapped Index Finger, Unlined Interior | EN 12477 Type B |
| Foundry Operations & Casting Forges | Extreme convective thermal exposure (>350°C), metal splash | Extra-Heavy Shoulder Split Cowhide + Extended 18" Gauntlet | Wool / FR Cotton Laminated Inner Composite | ANSI Cut A3 / Heat 4 |
Direct answers addressing technical specifications, sample iterations, factory audits, and OEM scaling parameters.
Type A gauntlet gloves offer higher heat, tear, and puncture resistance at the expense of lower flexibility, engineered specifically for heavy stick (SMAW) and MIG operations. Type B provides exceptional finger dexterity and tactile sensitivity with moderate heat thresholds, designed specifically for precision TIG procedures.
Seam failure typically occurs due to uneven hide hydration and chromium salt imbalance, which causes leather shrinkage under rapid thermal flash. By controlling our own tannery, oil balance and tensile stabilization are calibrated precisely to ensure thermal elongation stability up to 250°C continuous heat exposure.
Standard OEM custom configurations (custom embossing, specified cuff geometry, specialized composite linings) require an MOQ of 1,200 to 2,400 pairs per specification. Prototype turnaround is completed within 7–10 days, while bulk sea-freight container orders are finalized within 35–45 days post sign-off.
Yes. Full OEM industrial packaging support includes hydraulic blind-leather embossing, laser-etched cuff logos, flame-resistant interior compliance labels, EAN-13 / UPC barcode application, and specialized shelf-ready packaging for European and North American industrial supply distributors.
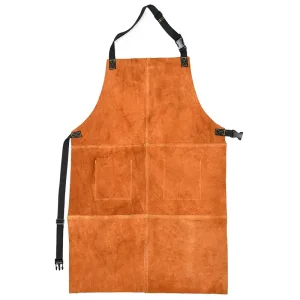
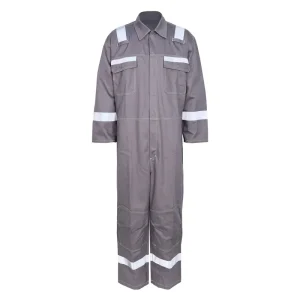
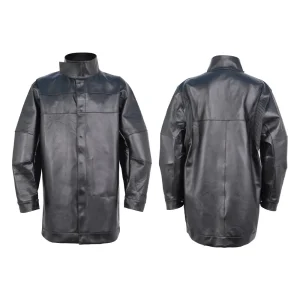
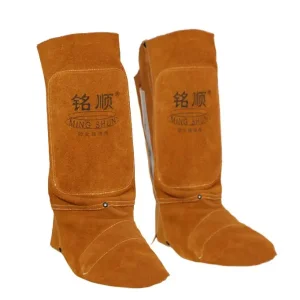
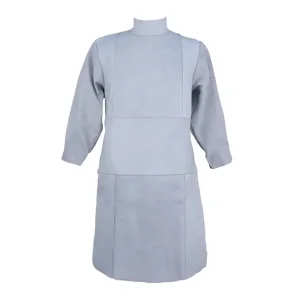
Browse our full factory suite of protective workwear, extended leather welding jackets, thermal spats, and composite aprons.