
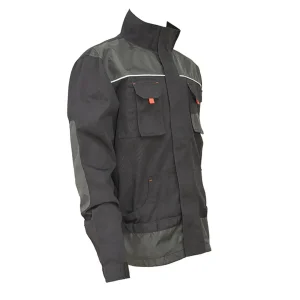
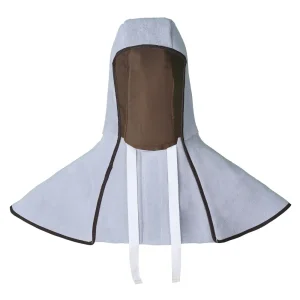
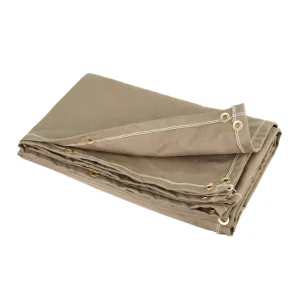
Original factory-spec workwear, split cowhide welding hoods, fiberglass spark blankets, and goatskin metal-handling gloves engineered for global import distributors.
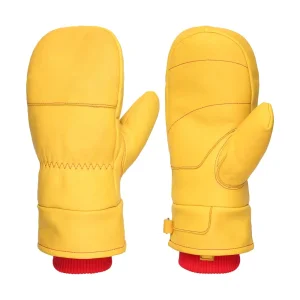
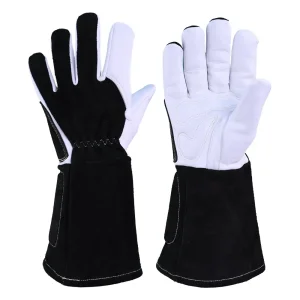

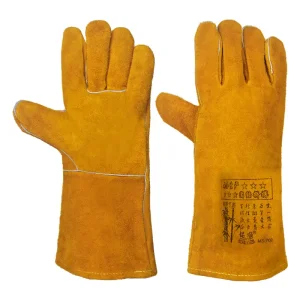
In high-hazard metalworking environments, protective gloves cannot be treated as commoditized expendables. Sourcing directly from an integrated Gaozhou manufacturer establishes a verifiable baseline of metallurgical cut-resistance, heat reflection, and consistent mechanical integrity.
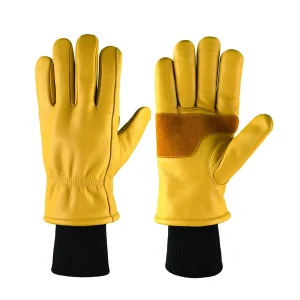
By operating internal beamhouses, chrome-tanning drums, and custom fatliquoring vats in Gaozhou, Guangdong, Ming Shun achieves uniform leather thickness (1.2mm–1.4mm grade-A split cowhide) without relying on secondary leather brokers. This eliminates oil saturation discrepancies, dry-cracking defects, and premature thermal shrinkage under metal-spatter load.
Standard stitching disintegrates within minutes of contact with molten slag. Our metal working handwear integrates 100% DuPont™ Kevlar® 4-ply or 5-ply heat-resistant thread. Every critical abrasion zone features leather-welted seams to isolate the thread from external shear friction and incandescent slag ingress.
Every bulk lot undergoes batch-level testing aligned with EN 388:2016 (4544FP mechanical score) and EN 12477:2001 Type A & B thermal criteria. From convective heat resistance at 350°C to extreme molten metal spatter deflection, our factory guarantees verifiable traceability back to raw rawhide batches.
Driven by ISO compliance mandates, industrial automation, and ergonomic workforce retention demands, metal working glove manufacturing is shifting rapidly from primitive heavy mittens to high-performance, hybrid-engineered tactical protection.
Replacing bulky multi-layer cowhide with lightweight 13-gauge/18-gauge High-Performance Polyethylene (HPPE) liners combined with split goatskin palm zones. Yields ANSI Cut Level A6 resistance with the precision tactile sensitivity required for robotic weld cell feeding.
Structural steel framing and automated sheet metal stamper operators face severe dorsal crush hazards. Modern production incorporates thermoset TPR or smart-molecule fluid dissipation pads directly over carpal bones to satisfy ANSI/ISEA 138 Level 3 impact protocols.
EU markets strictly monitor Hexavalent Chromium [Cr(VI)] content under Regulation (EC) No 1907/2006. Our environmentally controlled tanneries utilize vegetable pre-tanning and specialized redox stabilization chemistry to maintain Cr(VI) detection below quantifiable thresholds (<3.0 mg/kg).
Eliminating worker hand fatigue via digital 3D pattern digitization. Featuring 87-degree pre-curved gunn-cut fingers, seamless keystone thumb gussets, and moisture-wicking FR bamboo mesh liners designed for 10-hour continuous structural manufacturing shifts.
Matching specific metallurgical processing conditions to the exact leather grain, cut-proof reinforcement layer, and thermal barrier formula.
| Industrial Scenario | Operational Thermal & Mechanical Stressors | Recommended Leather & Fiber Construction | Key Standard Threshold |
|---|---|---|---|
| Heavy Sheet Metal Stamping & Laser Slitting | Razor-sharp burred edges, intense continuous abrasion, hydraulic oil saturation, minimal extreme heat. | Grain pigskin palm (naturally porous/oil-shedding) over seamless 18-gauge steel-reinforced HPPE liner; double-stitched index cuff. | EN 388: 4X43F ANSI Cut A7 |
| Heavy Fabrication & High-Amperage MIG/Flux-Core | Heavy radiant heat, continuous molten spatter splash, slag entrapment, rough structural I-beam handling. | Heavy-split cowhide (1.3mm), fully welted seams with 100% Kevlar thread, aluminized back-hand heat reflection pad, fleece lining. | EN 12477 Type A EN 407: 433X4X |
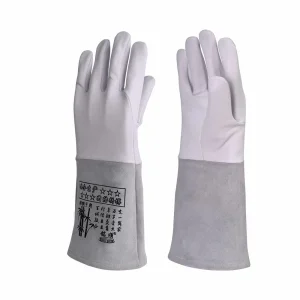
| High-Purity Aerospace TIG Welding (Orbital & Manual) | Precision filler rod feeding, high tactile dexterity requirement, negligible weld spatter, moderate radiant heat. | Grade-A unlined white goatskin, seamless index finger wrap, extended split cowhide 4-inch protective gauntlet cuff. | EN 12477 Type B Dexterity Level 5 |
| Hot-Dip Galvanizing & Foundries / Forge Hot Work | Intermittent contact heat (>350°C), hazardous zinc fumes, severe radiant blast, heavy drop-impact hazards. | Heavy chrome-split leather shell backed by aramid non-woven thermal felt, integrated high-density TPR dorsal impact cushions. | EN 407: 44XXXX ANSI Impact Level 2 |
| Automotive Chassis Robotic Welding Enclosures | Pinch points, sharp sheet stamped components, intermittent MIG spot spatter, constant tool maneuvering. | Kevlar/composite yarn knit palm with micro-foam nitrile coating; cowhide leather knuckle strap and thumb crotch patch reinforcement. | EN 388: 4543D ANSI Contact Heat L3 |
How multi-national PPE brands, EPC contractors, and government supply aggregators de-risk private-label safety manufacturing via Ming Shun's factory platform.
We translate engineering CAD drawings and target ASTM/EN criteria into production-grade tech packs. Customizing leather grain coloration, heat-embossed trademark emblems, woven satin specification tags, QR barcode tracking labels, and shelf-ready retail master cartons tailored for global industrial supply chains.
Quality assurance is not treated as a post-manufacturing formality. Our quality inspection regime enforces internal ISO 9001 inspections across 4 distinct phases: Rawhide grading > Die-cut pattern precision audit > Seam tensility and thread thermal integrity verification > 100% pre-packaging cosmetic and dimension conformity checks.
Situated in close proximity to major deep-water ports including Guangzhou, Shenzhen (Yantian/Shekou), and Hong Kong. Our logistics division delivers optimized high-cube container packing algorithms, phytosanitary fumigation compliance, export licensing, and localized customs clearance support for North American and European ports.
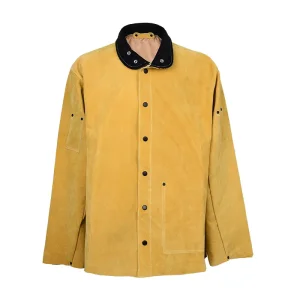
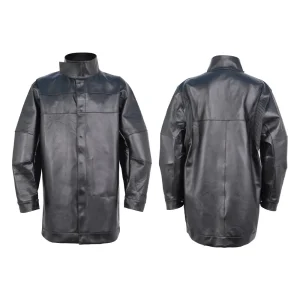
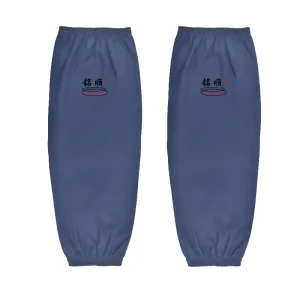
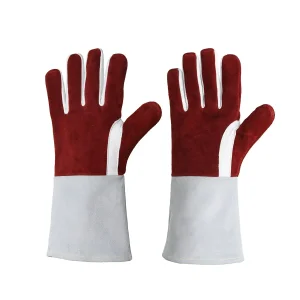
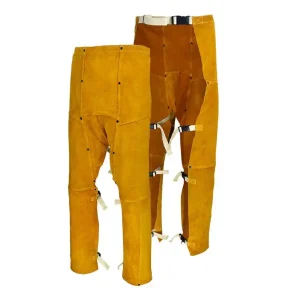
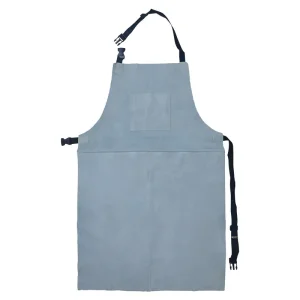
Premium pigskin welding jackets, reversible MIG gauntlets, split cowhide chaps, and heavy-duty aprons direct from our Gaozhou manufacturing facilities.
Technical, logistical, and compliance clarifications provided by Ming Shun's chief protective equipment engineers and international sales directors.
