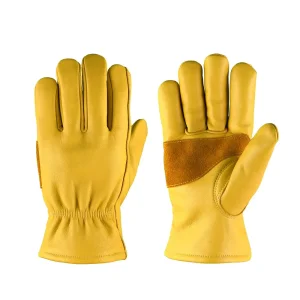
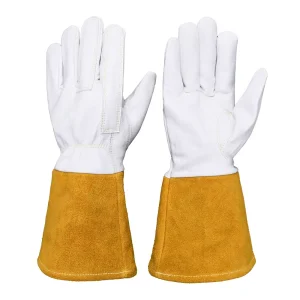
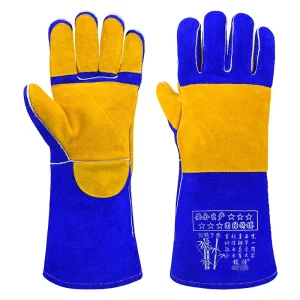
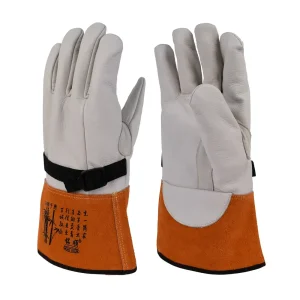
Direct manufacturing output featuring certified split cowhide, top grain goatskin, and flame-retardant hybrid configurations.
Addressing supply chain volatility, compliance harmonization, and total cost of ownership across heavy industrial operations.
Enterprise safety directors and global EPC procurement leads face increasingly complex challenges in outfitting workforces operating in heavy fabrication, naval dockyards, mining infrastructure, and petrochemical processing. High-risk industrial workplaces demand leather heavy-duty gloves that balance mechanical durability, high-temperature thermal barrier performance, ergonomic dexterity, and strict environmental compliance.
Generic trading intermediaries often rely on fragmented subcontracting workshops, resulting in inconsistent split-leather tensile strengths, erratic chromium VI leaching levels, and variable seam failure rates under extreme thermal exposure. Industrial safety managers require guaranteed material traceability, ISO 9001 certified batch reproducibility, and proven compliance with both European EN and North American ANSI/ISEA standards.
| Standardization Authority | Standard Code | Core Testing Dimension | Critical Performance Threshold |
|---|---|---|---|
| European Union (CE) | EN 388:2016+A1:2018 | Abrasion, Blade Cut, Tear, Puncture | Level 4 Abrasion (≥8,000 cycles), Level 4 Tear (≥75N) |
| European Union (CE) | EN 12477:2001/A1:2005 | Protective Gloves for Welders (Type A & B) | Type A: Heavy spatter resistance & thermal insulation |
| North America (ANSI) | ANSI/ISEA 105:2024 | Hand Protection Mechanical & Thermal Risk | Level 3+ Puncture Resistance, Contact Heat Levels 3-5 |
| Global Chemical Compliance | EU REACH Regulation | Chromium VI (Cr VI) & Azo Dyes Analysis | Cr(VI) < 3 mg/kg detected limit (EN 17075 method) |
Internalized beamhouse and retanning processes verify split cowhide density, collagen fiber integrity, and uniform moisture levels across production lots.
Every structural seam is secured with DuPont Kevlar aramid threads, providing thermal structural integrity without ignition or melting under spatter.
Dedicated monthly output surpassing 500,000 pairs of industrial gloves stabilizes lead times and eliminates inventory volatility for regional distributors.
Model-specific laboratory test certifications, material safety data sheets, and verified CE Declarations of Conformity protect commercial brand partners.
Examining the structural mechanics of bovine hide grades and multi-axial composite liner integration.
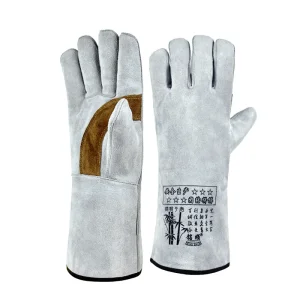
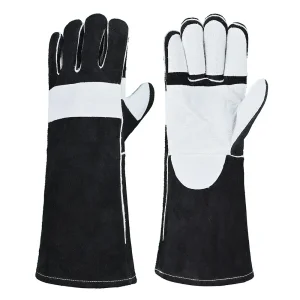
Formulated from prime shoulder and side splits featuring tight collagen interlacing. Suede finishing retains maximum surface friction and abrasion performance while resisting burn-through from molten slag droplets exceeding 800°C.
For applications where tactile sensitivity is paramount (such as GTAW/TIG welding and precision maintenance), top-grain goatskin offers natural lanolin lubricants that provide cut resilience and high flexibility without leather stiffening.
From moisture-wicking brushed cotton jersey to cut-resistant HPPE (High-Performance Polyethylene) and para-aramid knitted sleeves, gloves are engineered with targeted barrier defense suited for cold-weather work or sharp stamping flash.
Pioneering sustainable tanning, smart automation, and hybrid defensive architectures for next-generation workforces.
Scale adoption of organic vegetable retanning and modified aldehyde tanning chemistries to guarantee Cr(VI) non-detection while minimizing water footprint and wastewater chemical oxygen demand (COD).
Merging high-abrasion leather palms with ultra-breathable, arc-rated 4-way stretch aramid backs. Transitioning patterns to automated CAD-directed CNC laser nesting to minimize scrap and maximize seam strength.
Embedding temperature-resistant RFID inventory chips and microscopic thermal exposure tags directly into glove gauntlets to enable automated tool-crib tracking and predictive lifecycle monitoring in smart factories.
Custom-engineered formulations built for the rigorous operating conditions of heavy manufacturing and infrastructure.
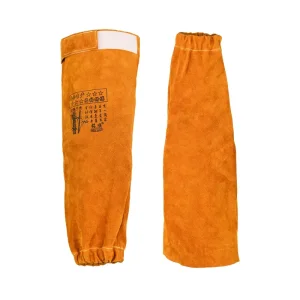
Submerged arc welding, flux-cored arc welding (FCAW), and heavy flame gouging generate extreme spatter. Our 16-inch split cowhide gauntlets prevent wrist burns and sleeve ignition during extended arc times.
High-friction crane handling, structural beam bolting, and rough rebar positioning require Level 4 puncture-resistant split leather with reinforced palm saddles to resist premature tear-out.
Extreme environmental temperature variations demand water-resistant tanning technologies and specialized fleece or Thinsulate thermal linings for Arctic and subsea pipeline fabrication operations.
Combining mechanical oil-resistant leather grips with internal cut-resistant para-aramid linings protects punch-press operators from sharp sheet-metal shear lines and burrs without compromising finger movement.
From custom tech-pack prototyping to verifiable containerized audit trails.
Custom palm reinforcement geometry, contrasting piping, debossed leather logos, high-definition woven tags, and retail hanging cards designed exactly to your brand guidelines.
Our Gaozhou facility adheres strictly to international social labor standards, fair wages, zero child labor policies, and environmental wastewater mitigation protocols verified by independent audits.
Streamlined FOB, CIF, or DDP direct-to-distribution center shipping. Multi-point carton barcoding, palletization to regional specifications, and complete customs documentation ensure smooth border clearance.
Technical and commercial answers addressing real procurement evaluation criteria.
Our standard manufacturing MOQ is generally 1,200 to 2,400 pairs per style and color configuration, depending on specialized leather dye matches or custom-knitted cut-resistant liners. For initial baseline validation orders, flexible batch sizes can be arranged upon commercial review.
Through our dedicated tannery drum retanning formulas, our technicians utilize specialized fat-liquoring oils that nourish inner collagen fibers. This delivers a supple hand-feel that prevents operator hand fatigue while maintaining the compact hide density needed to exceed EN 388 Level 4 tear thresholds.
Yes. We partner with internationally accredited testing bodies including SATRA, CTC, and SGS. In addition to formal CE Type Examination Certificates, we supply internal batch inspection data sheets recording tensile breaking strength, seam rupture load, and dimensional tolerance checks prior to container loading.
Standard physical prototype samples are crafted and dispatched within 7 to 10 working days. If custom tanned pantone hues or unique branded silicone grips are specified, tooling and dye preparation typically requires 14 days before courier dispatch.
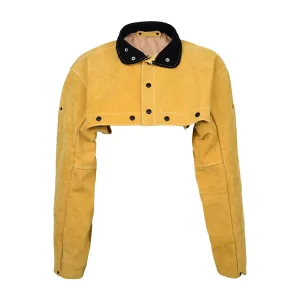
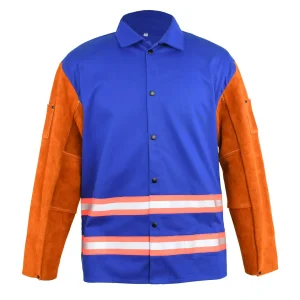
Comprehensive welding PPE gear engineered to ensure complete anatomical coverage under severe spatter and radiant heat.