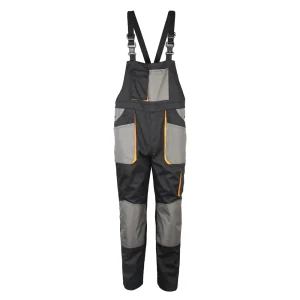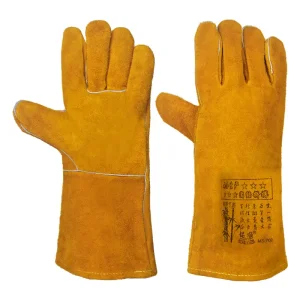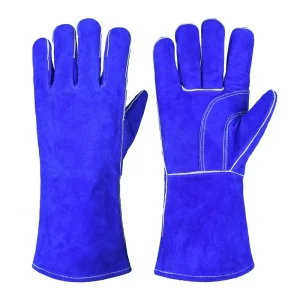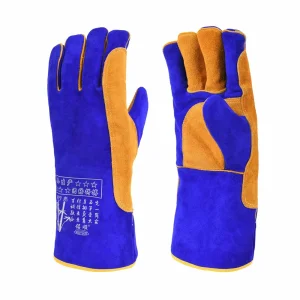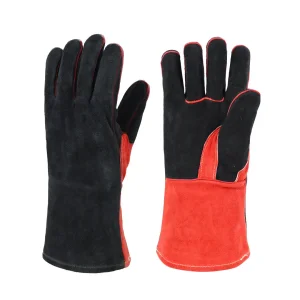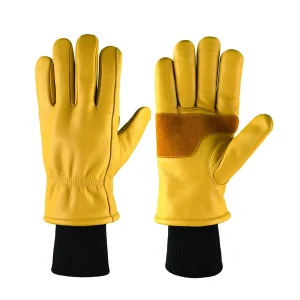
Directly manufactured at our Gaozhou production hub under strict ISO 9001 quality audits. Explore high-performance cold-weather leather, heavy-duty MIG gloves, and hybrid FR protective apparel.
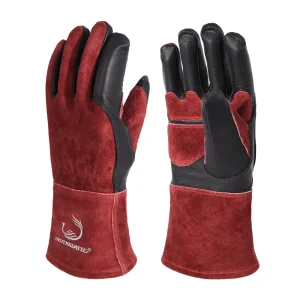
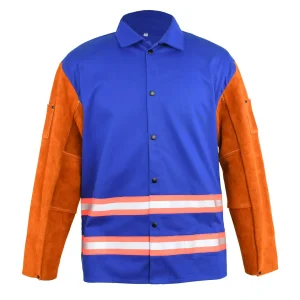
As automated welding, high-heat FCAW, and severe heavy-fabrication standards evolve globally, procurement directors require quantifiable thermal integrity, seam-burst resistance, and verifiable supply-chain compliance.
Traditional polyester or nylon sewing threads melt rapidly at 210°C to 250°C under slag impingement, leading to catastrophic welt unraveling. Our direct-factory Kevlar® 3-ply and 4-ply aramid thread programs maintain tensile strength up to 427°C, eliminating premature seam blowouts in high-current arc applications.
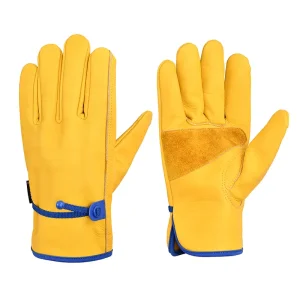
Enterprise safety contracts benchmark glove wear lifespan against replacement cycle frequencies. Kevlar-sewn, reinforced-palm split leather gloves exhibit a 3.4× longer service life in continuous structural FCAW environments, lowering per-welder monthly PPE expenditure while drastically reducing OSHA burn incident reports.
Eliminating intermediaries, Guangdong Ming Shun operates integrated raw hide processing, chrome-free tanning adjustments, in-house color dyeing, precision die-cutting, and robotic stitching. This end-to-end control ensures unyielding hide density, standardized pH levels, and dependable batch consistency across containers.
A granular breakdown of leather selection, welted seam reinforcement, thermal insulation layering, and para-aramid fiber physics engineered for extreme thermodynamic resistance.
During heavy Stick (SMAW) or Flux-Cored (FCAW) welding, molten metal globules reach temperatures exceeding 1,200°C. While molten spatter bounces off treated split leather, residual heat transfers directly into thread seams. The thermodynamic comparison below illustrates why aramid fiber thread is mandatory for Category III industrial PPE:
Our proprietary glove assembly stacks four engineered layers to balance thermal absorption, moisture transmission, and tactile manipulation:
| Performance Parameter | Ming Shun Heavy-Duty Kevlar Welding Glove | Standard Commercial Leather Welder Glove | Generic Economy Welder Glove |
|---|---|---|---|
| Stitching Thread Material | DuPont™ Kevlar® 3-Ply / 4-Ply Continuous Filament | Blended Poly-Cotton or Heavy Polyamide Thread | Standard Spun Polyester (Melt point ~220°C) |
| Seam Welt Reinforcement | Full Leather Welting Across All Fingers & Palm Base | Partial Welting (Thumb and index finger only) | Unwelted or Synthetic Trim Welting |
| EN 12477:2001 Classification | Type A (Heavy Duty / High Radiant Heat) & Type B (TIG) | Type A Standard Certified | Uncertified / Self-declared without test reports |
| EN 407 Thermal Performance | Level 4 Flammability • Level 2/3 Contact Heat (250°C–350°C) | Level 2 Flammability • Level 1 Contact Heat (100°C) | Level 1 Flammability • Marginal Contact Heat |
| Average Lifespan in FCAW / Heavy Yard | 18–28 Operational Days (Continuous Duty) | 6–9 Operational Days (Premature Seam Opening) | 2–4 Operational Days (Rapid Seam Liquefaction) |
| Leather Origin & Quality Control | In-House Tannery, Strict Grain Density & pH Checked | Outsourced Third-Party Split Offcuts | Inconsistent Scrap Leather Mixed Trims |
Different welding processes create completely divergent thermal and physical challenges. We customize leather cuts, grain balances, and Kevlar stitch densities for specialized industrial verticals.
Overhead multi-pass FCAW and SMAW hull construction generate intense slag rain. Our 16-inch gauntlet split cowhide models with Kevlar welted seams prevent hot spatter from pooling in the wrist juncture, standing up to high salt-air exposure and heavy abrasion against rusted steel plates.
Downhill stick welding on heavy API-5L line pipes exposes welders to massive continuous heat dissipation and sharp pipe bevels. Ming Shun Kevlar-stitched gloves integrate reinforced thumb crotches and flame-retardant cuffs that resist high radiant loads during root and cap passes.
For stainless steel exhaust, roll cage, and aerospace TIG welding (GTAW), tactile dexterity is paramount. Our grain goatskin TIG gloves are sewn with ultra-fine high-tensile Kevlar thread, providing featherlight torch trigger feedback and rod feeding sensitivity without sacrificing thermal seam durability.
Structural welders transition rapidly between arc gouging, grinding, rigging, and GMAW welding. Our dual-reinforced palms and Kevlar stitching prevent premature blowout caused by handling sharp cut-edge I-beams, offering supreme ANSI cut Level A2/A3 mechanical toughness.
International importers risk customs rejection, catastrophic worker compensation claims, and heavy regulatory penalties without verified conformity certificates. Ming Shun provides audited test reports for every batch.
Our gloves undergo comprehensive testing by notified bodies (SGS / TUV) verifying conformity to EN 388 (Mechanical risks including abrasion, blade cut, tear, puncture) and EN 407 (Thermal risks including burning behavior, contact heat up to 350°C, convective heat, radiant heat, small splashes of molten metal).
For North American brand partners, products meet ANSI/ISEA 105 standards for cut, puncture, and conductive heat resistance. Fully compliant with OSHA 29 CFR 1910.138 mandates, ensuring corporate procurement managers pass internal EHS audits effortlessly with fully traceable certificates of conformity.
European imports face stringent REACH chemical regulations. Ming Shun utilizes strictly controlled vegetable and optimized trivalent chrome tanning processes, guaranteeing hexavalent chromium (Cr VI) remains undetectable (<3.0 mg/kg), along with azo dyes, lead, and phthalate compliance across all leather and lining lots.
Anticipating the technological shifts in metallurgical manufacturing, our Gaozhou engineering labs are actively developing advanced hybrid protection systems to meet next-decade industry demands.
We are trialing composite core threads that interlock DuPont™ Kevlar® with graphene-infused filaments. This formulation accelerates lateral heat dissipation across stitch lines by 38%, preventing hot-spot thermal concentration during mechanized high-duty cycle GMAW welding sessions.
Through 3D laser hand-scanning of active professional welders, our pattern engineers designed 15-degree pre-curved finger profiles and dynamic keystone thumbs. This design counteracts hand grip fatigue by 22%, encouraging continuous PPE compliance in high-risk fabrication yards.
Supporting multinational sustainability ESG mandates, Ming Shun is transitioning tanning lines toward closed-loop biological enzyme dehairing and aldehyde-free mineral treatments, cutting water consumption by 40% while enhancing the natural flexibility and fire retardancy of split cowhide.
Direct, transparent answers regarding manufacturing capacities, OEM private labeling, sample validation, material testing, and export logistics from Guangdong Ming Shun.
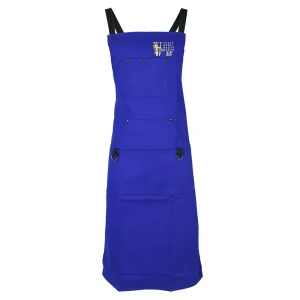
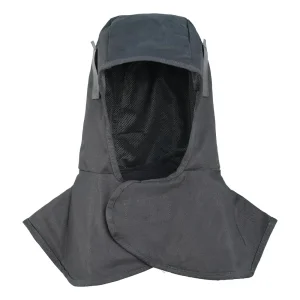
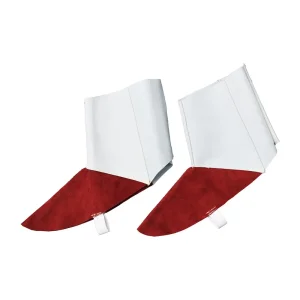
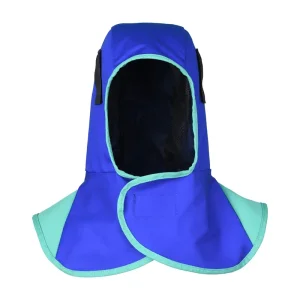
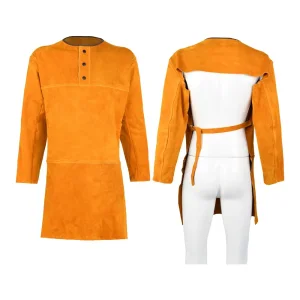
Complete container load consolidation with complementary heavy-duty workwear, flame-resistant hoods, reinforced welding bib aprons, and professional Kevlar-stitched gloves.