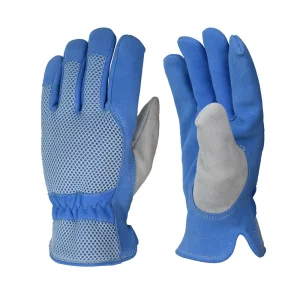
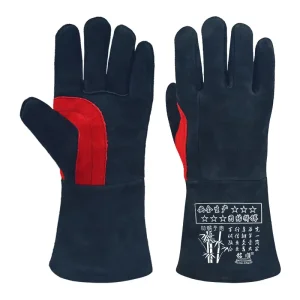
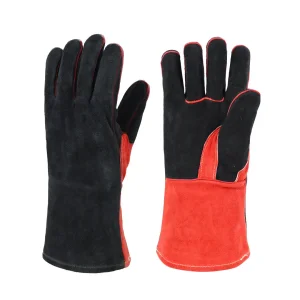
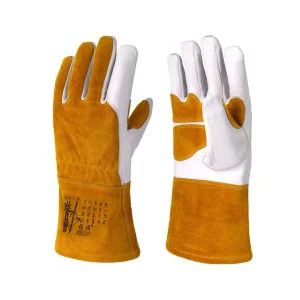
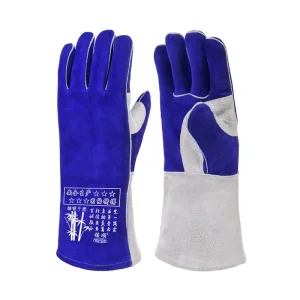
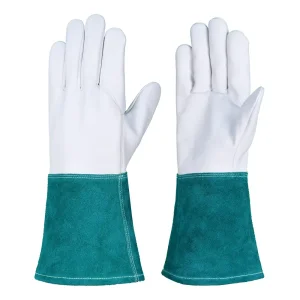
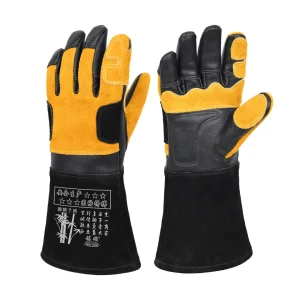
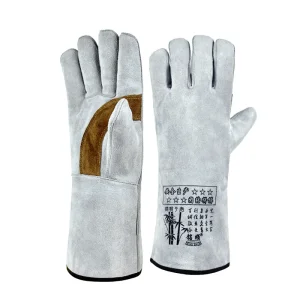
Factory-calibrated personal protective equipment tested for heavy molten slag, dielectric stability, and mechanical endurance.
Assessing supply chain vulnerabilities, multi-jurisdictional compliance mandates, and macroscopic procurement dynamics.
Global fabricators must navigate EN ISO 11611, EN 12477 (Type A & B), and ANSI/ISEA 105 requirements. Substandard barrier PPE exposes industrial enterprises to liability risks and severe workplace injury compensation overheads.
Tannery consistency dictates thermal protection outcomes. Tier-1 wholesale suppliers differentiate through fully vertically integrated hides processing, guaranteeing precise tensile strength, uniform grain thickness, and stable dye retention across bulk lots.
Robotic welding systems shift the human operator role toward high-intensity positioning, fine seam adjustment, and extreme thermal maintenance, escalating the demand for ergonomically articulated, high-tactility gauntlet gloves.
A multi-layered dissection of the specialized gauntlet construction protecting wrist and forearm anatomy against thermal convection, conductive energy, and mechanical laceration.
| Functional Zone | Material Engineering | Protection Target | Operational Paradigm |
|---|---|---|---|
| Rigid Gauntlet Cuff | Split Cowhide / Fire-Retardant Fabric Lining | Forearm Radiated Heat & Downward Slag | MIG, Flux-Cored Arc & Heavy Stick Welding |
| Palm & Finger Grip | A-Grade Grain Goatskin / Reversed Cowhide | Micro-tactile TIG rod feed & trigger ergonomics | High-precision Pipe & Aerospace TIG |
| Reinforced Keystones | Ergonomic Keystone / Wing Thumb with Welted Inseams | Friction wear, stress splits, and gripping exhaustion | Heavy fabrication, offshore pipe yards & dry docks |
| Internal Micro-Climate | Laminated Foam Core + 100% Breathable Cotton / Mesh | Conductive heat spikes, perspiration accumulation | High-amperage continuous structural joins |
| Interlocking Seams | DuPont™ Kevlar® 4-Ply / 5-Ply Thread Stitched | Direct spark burn-through, mechanical seam rupture | Foundry pour, heavy gouging & plasma cutting |
Reinforcing palm beds with woven aramid interfacings to achieve ISO level 4-5 abrasion defenses without sacrificing tactile flexibility.
Aluminized backhand deflective shields mitigate up to 95% of radiant heat waves generated during high-duty-cycle automated processes.
Eco-conscious trivalent chrome limits and vegetable retanning methodologies mitigate skin sensitivities and comply with strict European REACH mandates.
Biomechanical CAD hand profiling eliminates bunching across the metacarpal joints, cutting hand fatigue rates by up to 34% over 8-hour work shifts.
How distinct manufacturing sectors implement gauntlet-cuff welding gloves to satisfy localized safety audits and operating conditions.
High salinity and damp weather demand premium cowhide gauntlets resistant to moisture-induced stiffening. Thick 14-inch to 16-inch split cuffs protect pipe fitters from high-heat slag inside cramped naval bulkheads.
High-volume robotic cell monitoring and spot welding require tactile agility. Goatskin palms mated to stiff split cowhide gauntlets prevent forearm contact with sharp stamped sheet edges and hot sparks.
Root-pass pipe welders endure open weather and continuous radiant heat. Kevlar®-stitched, fleece-insulated gauntlet configurations shield hands during high-amperage, all-position downhill stick welding.
Turnkey solutions for industrial importers, safety distributors, and private-label PPE brands.
We translate custom customer CAD specs into verified patterns, balancing hide usage efficiency, cuff stiffener options, and stitch tolerances to optimize production costs.
Every dye-lot and split layer undergoes tear resistance, pH neutral balancing, and flame immersion testing. Full trace reports are furnished alongside master bill-of-lading documents.
Direct branding solutions include heat debossing, reflective woven labelling, retail display hangtags, and moisture-sealed inner bags optimized for international container shipments.
Core engineering criteria, compliance frameworks, and logistics answers for professional safety procurement executives.
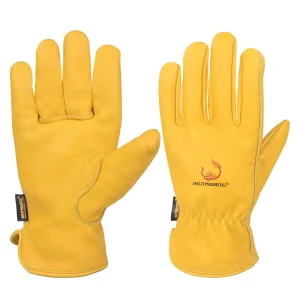
A gauntlet cuff extends 4 to 8 inches up the forearm with an open flare geometry. This allows instant glove ejection if hot slag enters the aperture, overlaps snugly with protective jacket sleeves, and shields vulnerable radial arteries from direct radiant heat.
Type A represents heavy-duty stick and MIG welding gloves offering elevated heat protection but reduced dexterity. Type B represents high-dexterity gloves (such as TIG gloves) with thinner, supple leathers that meet lower thermal requirements.
Standard polyester or cotton threads disintegrate rapidly under direct spark impact and temperatures above 200°C. Kevlar® thread will not melt, resists chemical breakdown, and maintains seam integrity under extreme cyclical heat and friction stresses.
Split cowhide offers high abrasion and radiant heat resistance across the backhand and cuff. Premium top-grain goatskin provides an optimal tensile-to-thickness ratio for the palm and fingers, providing smooth wire feeding in precision TIG work.
Standard OEM glove runs range around ~45 days following tech-pack and prototype sign-off. Bulk scaling accommodates private labeling, brand color-matching, custom die cuts, and containerized dispatch.
In-house computerized splitters calibrate leather hide thickness to ±0.05 mm tolerances. Every production lot undergoes multi-point micrometer checks before die cutting to eliminate thin-spot failures.
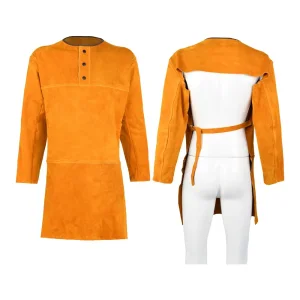
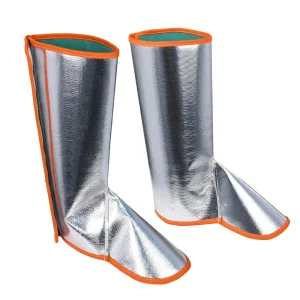
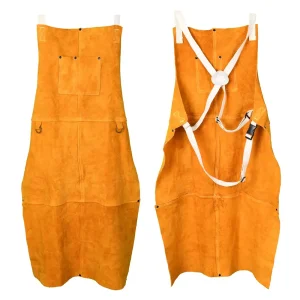
Complete workshop safety: from aluminized heat pads and leather aprons to heavy-duty welding spats and long gauntlets.