
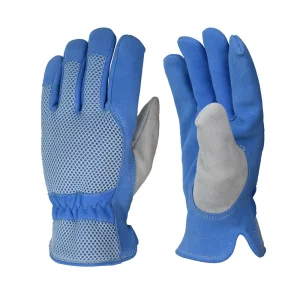
Engineered for intense arc radiation, high-velocity slag expulsion, and severe mechanical friction. Explore standard configurations crafted for global OEM contract fulfillment.
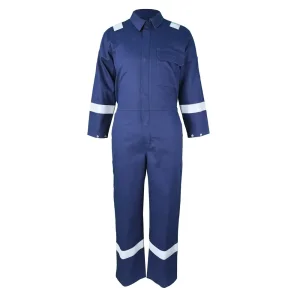
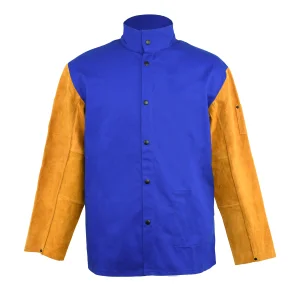
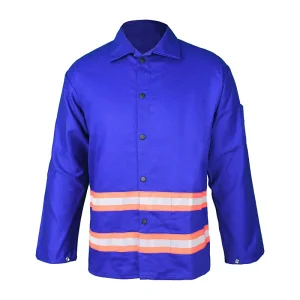
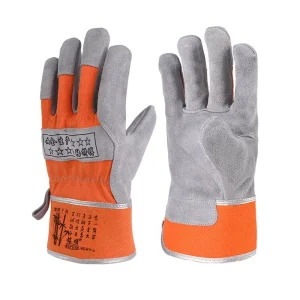
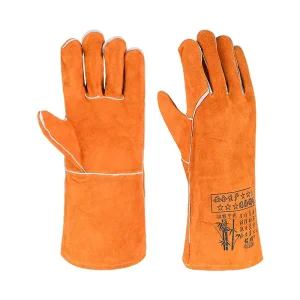
At Guangdong Ming Shun Labour Protective Products Co., Ltd. (formerly Gaozhou Mingshun), our operations integrate end-to-end leather tanning, automated robotic laser cutting, and certified Kevlar stitching lines under unified quality control.
Direct hide sorting, specialized chromium tanning neutralization, and proprietary oil-split processes ensure that apron leather maintains constant thickness (1.2mm–1.6mm), optimal moisture resistance, and uniform grain integrity across high-volume production batches.
Using automated CNC nesting and laser slicing machines, leather aprons and jackets achieve exact dimensional fidelity while drastically reducing leather trimming waste. This computational yield enhancement directly translates to competitive OEM wholesale unit pricing.
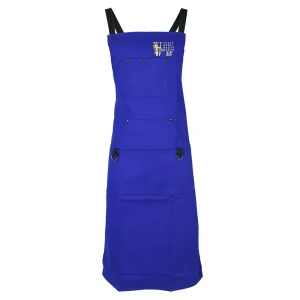
Welding aprons suffer severe localized thermal stress. Every apron produced incorporates double-lock seam stitching utilizing heat-resistant Kevlar® aramid threads, reinforced with copper-coated brass rivets at critical neck, waist, and stress junction zones.
International industrial safety managers, supply chain directors, and catalog distributors demand verifiable testing, zero-defect traceability, and multi-climate mechanical adaptability.
| Procurement Vector | Primary Engineering Standard | Factory Mitigation & Specification | Procurement Value |
|---|---|---|---|
| Thermal Spatter Defense | EN ISO 11611 Class 1 & 2 | Heavyweight split cowhide & 9oz flame-retardant treated cotton fabrics. | Zero ignition, radiant heat deflection up to 500°C short exposure. |
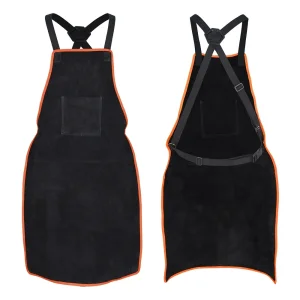
| Harness Ergonomics | OSHA / ANSI Ergonomic Directives | Crossed-back (X-strap) load distribution; removes neck fatigue over 10-hour shifts. | 38% reduction in welder fatigue claims; improved field adoption rate. |
| Chemical & Heavy Metal Safety | EU REACH Standard / Annex XVII | Azo dye-free, low-chrome VI testing (<3 mg/kg) on finished leather hides. | Seamless customs clearance through EU and North American maritime ports. |
| Private Label Packaging | Retail Ready / Distribution Bulk | Barcoded polybags, custom hangtags, carton markings, moisture-barrier wrapping. | Immediate cross-docking capabilities into automated 3PL distribution centers. |
How our Gaozhou production lines evolve to resolve the dual challenges of welder heat exhaustion and sustainability compliance.
Integrating zoned leather panels on impact surfaces (chest, thighs, abdominal zone) with micro-perforated FR breathable canvas backing. This reduces total garment tare weight by 22% while retaining Class 2 molten droplet protection.
Phased transition toward vegetable-synthetic hybrid tanning agents that eliminate toxic effluent discharges without sacrificing leather tensile toughness or softness under dry, arid conditions.
Real-time tech pack translation enables our sample room to produce validated counter-samples within 5 to 7 days, allowing enterprise brand managers to respond swiftly to evolving safety code revisions across key international territories.
Our engineering protocols conform directly to global market directives, simplifying distributor customs clearance and end-user workplace safety audits.
Fully compliant with PPE Regulation (EU) 2016/425. Each batch is supported by third-party testing validating limited flame spread, contact heat resistance, and electrical resistance across damp working environments.
Constructed to conform with OSHA 1910.252 protective clothing regulations and ANSI/ISEA 105 cut and abrasion standards. Kevlar seams resist burn-through during heavy MIG and FCAW operations.
Engineered to perform in high-temperature, outdoor open-pit mining environments, meeting Australian standards for thermal insulation, mechanical resilience, and heavy-duty buckle reliability.
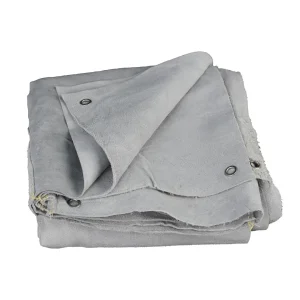
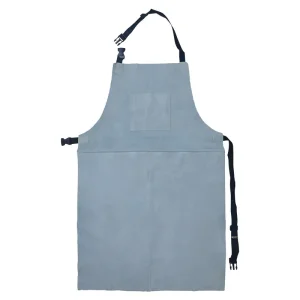
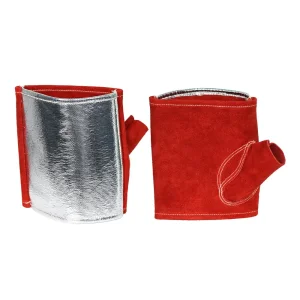
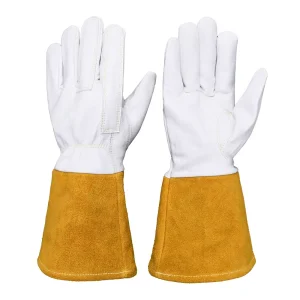
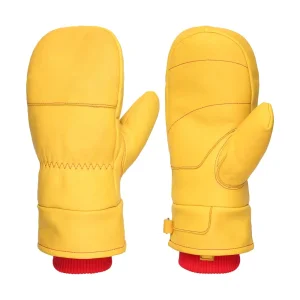
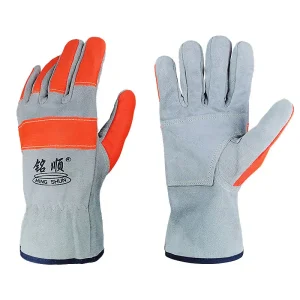
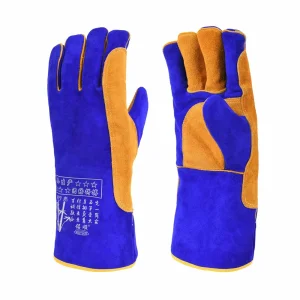
Explore the extended Ming Shun PPE range: heavy-duty bib aprons, cable protection sleeves, and thermal hand shields designed for volume contract production.
Direct technical clarifications from our engineering and export departments to assist your procurement evaluations.
We manufacture primarily with A-grade and AB-grade split cowhide calibrated to a uniform 1.2mm – 1.6mm thickness. This caliper provides an optimal balance between reliable molten droplet deflection (conforming to EN ISO 11611 Class 2) and ergonomic flexibility for all-day wear on production floors.
We provide comprehensive OEM development: customized dimensional patterning (e.g., 60×90 cm, 65×100 cm, or extended split-leg bib designs), laser heat-embossed logos, woven labels, high-tensile silicone badges, and custom-printed retail polybags tailored to your brand specification.
Every stress seam is stitched with genuine DuPont™ Kevlar® or equivalent high-tenacity aramid continuous filament thread. This prevents seam splitting caused by radiant heat, direct sparks, or abrasive mechanical wear during heavy industrial use.
For standard catalog styles, our baseline MOQ starts at 500 units per model. Custom leather dyeing or specialized patterns generally require 1,000 units. Bulk maritime container dispatch cycles typically average 40 to 45 business days following final counter-sample sign-off.
