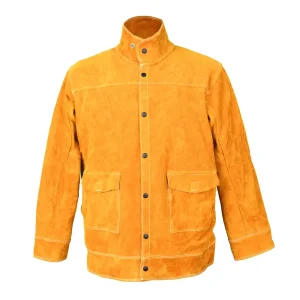
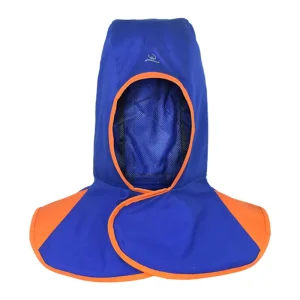
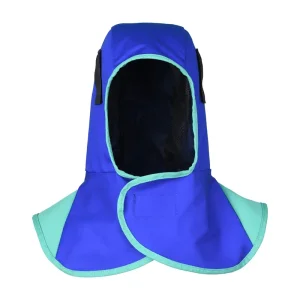
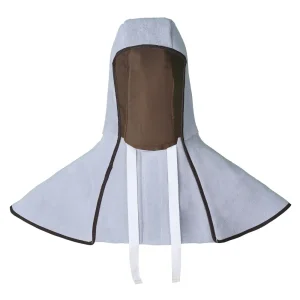
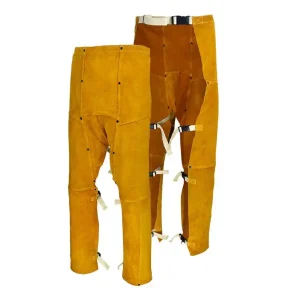
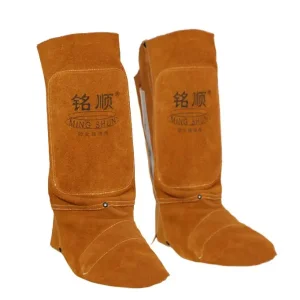
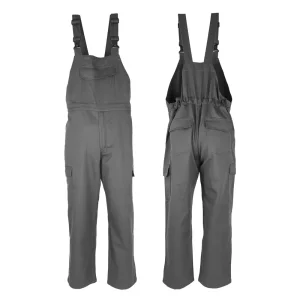
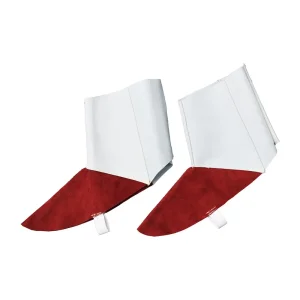
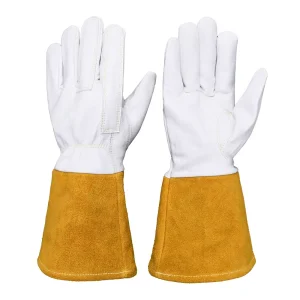
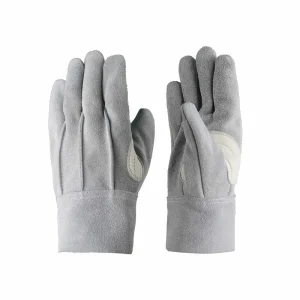
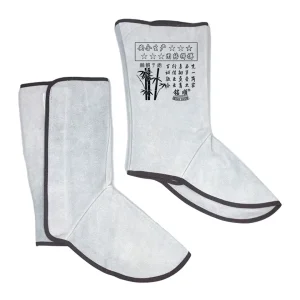
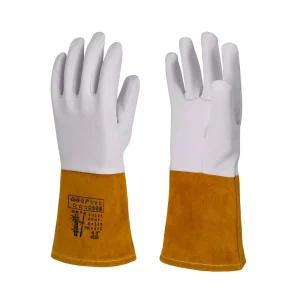
Explore our precision-crafted protective line available for OEM white-label integration and high-volume enterprise procurement.
Welding protective clothing is a mission-critical thermal barrier. As industrial operating temperatures increase and multi-hazard environments become standard, contract manufacturing must transcend traditional garment assembly.
Coveralls must shield operators from convective thermal transfer, radiant heat flux, and projectile slag exceeding 1400°C. By deploying chemically treated heavy-density cotton (9 oz to 12 oz) paired with strategic grade-A cow split leather over the torso and thighs, our designs achieve zero molten metal penetration while preventing second-degree burns.
Welding positions require heavy contortion across abrasive steel profiles. Ming Shun incorporates high-tenacity DuPont™ Kevlar® continuous-filament aramid stitching. Triple-needle felled seams at the gusset, crotch, and shoulder nodes yield burst strengths exceeding 850 Newtons, preventing seam blowouts under acute structural stress.
Fatigue directly impairs industrial safety compliance. Our pattern master team leverages full-motion bi-swing pleated action backs, articulated knee darts, and underarm diamond gussets. This engineering allows overhead FCAW and positional pipe welding without pulling cuffs, exposing wrists, or riding up along the lumbar region.
Selecting the ideal textile composite determines protective performance, thermal comfort, product longevity, and procurement cost-efficiency across international markets.
| Material Configuration | Areal Weight | Thermal & Spatter Resistance | Dexterity & Ergonomics | Certified Standards | Optimal Deployment |
|---|---|---|---|---|---|
| Selected Split Cowhide Leather | 1.2 mm - 1.4 mm | Maximum Barrier (Class 2) | Moderate (Structured) | EN ISO 11611 Cl. 2, ISO 9150 | Heavy Gouging, High-Amp MIG, Plasma Cutting |
| Hybrid FR Cotton / Leather Panels | 9 oz FR + 1.2 mm Leather | High Targeted Protection | High (Hybrid Flex) | EN ISO 11611 Cl. 1 & 2 | Shipyard Seam Welding, Pressure Vessel Assembly |
| 100% FR Cotton Sateen (Treated) | 9.0 oz / 305 gsm | Medium (Class 1) | Superior Breathability | NFPA 2112, ASTM F1506, Cl. 1 | Structural Assembly, TIG/GTAW, Warm Climates |
| AR / FR Cotton-Rich Twill Blend | 7.0 oz / 240 gsm | Moderate (Dual Hazard Arc/FR) | Maximum Flexibility | ASTM F1959 (ATPV 8.6 cal/cm²) | Utility Welding, Electrical Maintenance Cells |
| Inherent Aramid / Antistatic Matrix | 6.5 oz / 220 gsm | High Thermal Threshold | High Tear Resistance | EN 1149-5, NFPA 70E, Cl. 1 | Offshore Oil & Gas Platforms, Petrochem Tankers |
How Guangdong Ming Shun Labour Protective Products leverages deep vertical integration to secure cost leadership, consistent leather grading, and rapid scale for worldwide distributors.
Unlike trading houses that source piecemeal hides, we control tanning, chemical chroming, and mechanical softening under one roof. This stabilizes hide thickness (±0.1 mm tolerance), preserves uniform dye retention, and eliminates chemical odor.
Full raw material ownership removes tier-2 broker markups. Global procurement directors benefit from an 18% to 26% margin efficiency compared to European or North American assembly plants, without sacrificing compliance standards.
Computerized multi-layer CNC cutting heads minimize fabric scrap down to 4.2%, maximizing hide yield. Precise CAD digital files guarantee that repeat orders 36 months apart preserve exact millimeter tolerances across chest and inseam specs.
Quality assurance occurs across 4 operational gates: raw material spectral testing, post-cutting dimensional check, in-line stitching tension inspection, and 100% end-of-line metal-detector / finishing audits before export packing.
International protective wear compliance leaves no margin for error. We safeguard your import business with documented conformity trails and multi-jurisdictional testing.
Complete conformity with PPE Regulation (EU) 2016/425. Our coveralls meet EN ISO 11611 (Class 1 & Class 2 for flame spread, radiant heat, and small molten splashes) and EN ISO 11612 (A1, B1, C1, E2, F1). Module B Type-Examination and Module D factory audit certificates available upon request.
Engineered for compliance with NFPA 2112 (Standard on Flame-Resistant Clothing for Protection of Industrial Personnel Against Short-Duration Thermal Exposures from Fire) and ASTM F1506. Third-party testing verifies afterflame under 2.0 seconds and char lengths well below the 102 mm threshold.
Every shipment carries lot-numbered textile test certificates. We provide Limiting Oxygen Index (LOI) documentation, pH skin compatibility records, and Chrome VI-free certification (<3.0 ppm under ISO 17075) to protect importers from border seizures and regulatory penalties.
Where our contract-manufactured protective welding coveralls and PPE accessories operate across global heavy industries.
Submerged ballast tanks and double hulls present intense positional flux-core welding. Hybrid leather-front coveralls resist localized high-temperature slag, continuous crawl friction, and high marine humidity.
High-speed downhill stick welding (SMAW) generates fierce radiant heat and showers of molten beads. Full split leather or heavy 12 oz FR cotton coveralls deliver all-day protection across open-air trench operations.
Robotic cell operators and manual jig tack-welders demand high dexterity and snag-free profiles. Concealed hardware prevents scratch defects on sensitive exterior metal vehicle body panels.
Confined maintenance demands certified dual-hazard protection: flame spread prevention combined with anti-static charge dissipation (EN 1149-5) to eliminate spark risks in volatile vapor atmospheres.
The PPE sector is undergoing a technology-driven evolution. As your contract OEM partner, Ming Shun leads the integration of sustainability, ergonomics, and intelligent industrial tracking.
European REACH restrictions and global ESG mandates are phasing out conventional fluorocarbon repellents and hazardous tanning chemicals. Ming Shun utilizes closed-loop bio-based vegetable chrome-reduced tanning systems and zero-PFAS moisture-wicking FR chemistries that maintain wash durability past 50 industrial cycles.
Heat stress remains the leading operational risk for heavy welders. Next-gen coveralls deploy engineered vent channels across the scapula, lined with flame-resistant micro-mesh. These chimney-style drafts purge hot air without offering entry angles for overhead spatter droplets.
Large EPC enterprises increasingly rent workwear through commercial laundry circuits. We embed ultra-high-frequency (UHF) flexible silicon RFID microchips into interior seam plackets, enabling computerized tracking of industrial wash counts, repairs, and recertification cycles.
From technical spec sheet to standard 40ft high-cube container dispatch, our audited development cycle eliminates project risk.
We review CAD patterns, bill of materials (BOM), regional sizing standards (US ANSI vs. Euro slim fit), and seam construction specifications.
Our dedicated sample room produces golden samples with fully customized leather embossing, branded silicone patches, and spec conformity sheets.
A controlled 500-unit pilot run validates needle heat limits on aramid thread, snap closure pull-strengths, and laundry dimensional stability.
Full-scale manufacturing across dedicated lines. Export cartons are vacuum-sealed, barcoded, palletized, and prepared for FOB/CIF shipping.
Clear, direct answers regarding production lead times, minimum order quantities (MOQ), custom branding tooling, and compliance documentation.
We are a direct manufacturer. Our 25+ year factory campus is situated in Pukang Industrial Park, Gaozhou City, Guangdong, China. With over 1,000 on-site personnel and integrated leather tanning facilities, our buyers negotiate directly with the factory engineering and production leadership.
For standard production designs in standard colors (Navy, Royal Blue, Khaki), our MOQ is typically 500 units per style. For fully custom color dye lots, custom leather finishings, or specialized multi-hazard fabric weaves (e.g., Modacrylic/Aramid), our MOQ is 1,200 units to ensure spinning and dyeing efficiency.
Following approved pre-production samples and fabric lab dips, standard mass manufacturing requires 40 to 50 days. Repeat continuous replenishment orders operate under scheduled buffer stocks with expedited dispatch in as little as 25 to 30 days.
Our FR cotton textiles utilize covalent chemical phosphorus-nitrogen cross-linking (similar to Proban® and Pyrovatex® mechanisms). We perform batch testing up to 50 and 100 industrial wash cycles at 60°C and 75°C per ISO 15797 to verify zero degradation in char length and self-extinguishing behavior.
We offer comprehensive private-label OEM services: high-density heat transfer logos, direct aramid embroidery, fire-retardant woven neck labels, laser-etched leather shoulder badges, individual retail polybags with EAN/UPC barcodes, and custom inner carton packing according to your warehouse specs.
Yes. We cooperate with notified bodies and test labs including SGS, TUV, Intertek, and SATRA. We can provide full test reports and certificates of conformity for EN ISO 11611, EN ISO 11612, NFPA 2112, ASTM F1506, and EN 388 tailored to your target import destination.
Complete your wholesale protective lineup with our full-spectrum protective solutions built for severe industrial fabrication environments.