Engineered for mission-critical hot work environments. Full-run OEM and bulk distribution direct from our Gaozhou processing centers.
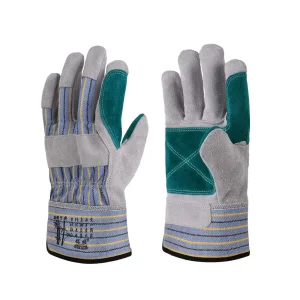
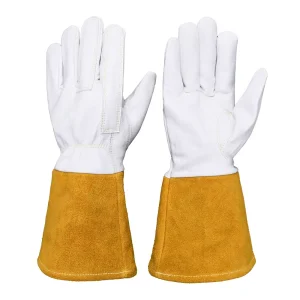
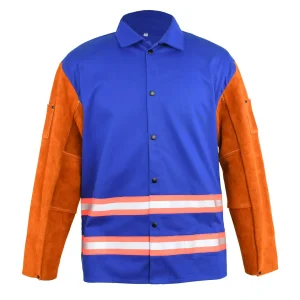
Gas Tungsten Arc Welding represents the precision apex of metal joining. As automated orbital welding, exotic superalloys, and stringent metallurgical cleanliness dominate modern fabrication, hand protection requirements must pivot from crude thermal mass to micro-tactile dexterity and hyper-stable barrier integrity.
Unlike SMAW or GMAW processes where electrodes feed continuously or feature heavy coatings, GTAW requires manual rod manipulators to advance thin filler wires (0.8mm to 2.4mm) seamlessly. Gloves must provide zero surface stick-slip and friction-free cutaneous feel.
TIG arc physics emit extreme radiant ultraviolet wavelengths. Conventional unlined pigskin degrades prematurely under high argon-arc intensity. Modern formulations demand proprietary chromium tanning chemistry combined with natural collagen density to block actinic erythema.
High-frequency arc-starting circuits generate electrical pulses upward of 10,000 volts. Gloves with unshielded or hygroscopic internal components can trigger micro-shocks to the torch operator. Premium dielectric leather matching and moisture-free tannery protocols mitigate parasitic discharge.
Tier-1 procurement organizations within aerospace manufacturing, cryogenic engineering, pharmaceutical pipefitting, and nuclear energy facilities do not purchase generic industrial gloves. They procure certified failure-mitigation solutions that safeguard operational uptime and preserve the welder's fine motor skills.
From pressure vessel fabrication under ASME Boiler & Pressure Vessel Code (BPVC) standards to hyper-clean semiconductor exhaust lines, each industrial domain poses unique metallurgical and tactile constraints.
Joining Inconel, Monel, and Grade 5 Titanium demands absolute torch stability without hand tremor caused by stiff gloves. Our butter-soft goatskin provides tactile feedback identical to bare-hand dexterity, allowing micro-amperage pedal coordination and smooth filler movement.
Orbital and manual GTAW pipe joints in breweries, dairy, and pharmaceuticals require zero transfer of free iron particles or surface oils. Our vacuum-degreased, dry-finish leather prevents hydrocarbon transfer onto purge gas joints, preserving purge weld integrity.
Fabrication under strict Section IX radiographic criteria cannot tolerate slag inclusions or spatter burns that force welder repositioning. Extended safety cuffs made from 1.3mm heavy split cowhide prevent forearm wrist gaps and shield against incidental reflective heat.
25+ years of specialized PPE manufacturing infrastructure, supporting private label clients across North America, the European Union, Australia, and the Middle East.
Pairs Monthly Glove Capacity
Skilled Assembly Technicians
Years Industrial Manufacturing
Days Typical Custom Order Lead Time
Operating without certified compliance invites border impoundments, legal liability, and brand equity damage. We enforce an uncompromised testing infrastructure validated by third-party notified bodies.
Designated specifically for TIG welding where high dexterity and lower heat levels are present. Certified flexibility, abrasion resistance, and stitch strength.
Calibrated for North American enterprise bids, verifying mechanical cut levels, puncture resistance, and conductive heat transfer up to 200°C.
Strictly controlled chemical inputs. Laboratory verified <3 mg/kg Chromium VI content, zero azo dyes, and low aromatic amines for skin-contact safety.
Complete traceability back to the raw tannery hide lot, recorded tensile testing, and documented batch inspection reports delivered with every container.
A transparent, standardized manufacturing lifecycle built to reduce lead-time variability and ensure flawless repeat orders.
We analyze your technical spec sheet, CAD drawing, or physical benchmark sample. Patterns are digitized to calculate yield and optimize stitch geometry.
Sample units are produced within 7–10 days using dedicated goatskin lots, branded pull tabs, personalized heat stamps, and custom seam piping.
Laser and hydraulic clicker presses cut matching pairs with balanced tensile orientation. Dedicated sewing lines run Kevlar threads at calibrated stitch tension.
100% inline seam inspection, dimensional verification, iron pressing, moisture-barrier packaging, and export crate consolidation for sea or air logistics.
Welding metallurgy is accelerating. Ming Shun invests heavily into composite leather hybrids to meet evolving technical challenges across automated and high-frequency welding applications.
Integrating sub-micron graphene dispersions into the underside of the grain leather to double conductive heat dissipation without adding bulk, preserving tactile touch while elevating thermal contact ratings.
TIG fabricators frequently deburr sharp plate edges and cut wire ends. We are weaving seamless HPPE/steel-fiber interlock linings onto the palm area, securing Level 4 cut safety while maintaining thin fingertip feel.
Transitioning toward aldehyde-free, plant-based synthetic tanning polymers that reduce water footprint by 40% and ensure rapid leather biodegradability at end-of-life, supporting corporate ESG compliance mandates.
Direct answers for purchasing directors, supply chain leads, and industrial distributor product managers.
Goatskin contains a higher natural lanolin content and a dense, interlocking collagen fiber structure. This allows the leather to be shaved to 0.7mm–0.9mm for featherlight fingertip control while retaining high tensile strength and puncture resistance that would fail in thin cowhide.
Type B mandates higher dexterity (minimum level 4 or 5 in finger pin-pickup tests) but permits slightly lower thermal insulation limits compared to heavy MIG Type A gloves. This specifically caters to GTAW's requirement for nimble torch angle control and rod feeding.
Our standard production MOQ for custom logo debossing, private-label woven tags, and custom retail packaging is 1,200 pairs per size/style. For stock catalog designs under Ming Shun branding, trial orders from 300 pairs can be accommodated.
We own and supervise the leather tanning and preparation steps in Gaozhou. Rather than buying variable scrap leather from third-party markets, we retain standardized master recipe chemical profiles and sort raw hides by electronic thickness sensors before clicker cutting.
Integrate comprehensive workshop protection with fully compatible heavy cowhide accessories, flame-retardant headwear, and specialty cushions.