Discover factory-direct welding personal protective gear built to withstand severe splatter, high amperages, and aggressive abrasion profiles across global worksites.
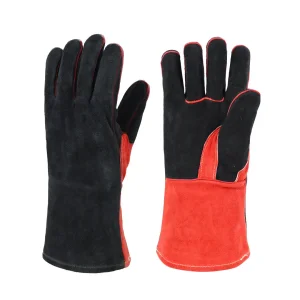
In advanced robotic welding cells, shipbuilding docks, and pipeline construction, traditional golden or gray split leather is rapidly giving way to deep black split cowhide and top-grain leather solutions. The shift is not purely aesthetic—it is rooted in surface thermodynamics, contamination masking, and proprietary chromium-complex dyeing techniques.
Heavy MIG, FCAW (Flux-Cored Arc Welding), and stick welding generate dense carbonaceous soot, iron oxides, and anti-spatter chemical residue. Conventional light-colored leathers soil within hours, triggering premature disposal by operators. OEM black split leather retains an intact, clean visual profile across hundreds of thermal cycles, drastically reducing perceived wear and lowering PPE replacement turnover by up to 28%.
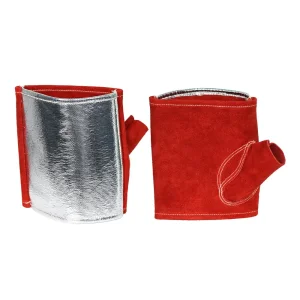
Our proprietary drumming and black aniline/mineral pigmentation treatments alter the thermal emissivity of the split leather. When paired with secondary aluminized heat-shield inserts or dense 320gsm flame-retardant fleece, the outer black split cowhide layer dissipates convective thermal spikes faster than untreated rough-split leather, protecting metacarpal tendons during continuous high-amperage torch handling.
High temperatures and sharp structural steel edges destroy regular polyester thread. Every OEM black welding glove engineered in our factory utilizes 100% DuPont™ Kevlar® 4-ply or 5-ply heat-resistant structural stitching. All critical stress nexuses—including the thumb crotch, base of the palm, and finger welts—feature cowhide split welting that shields the thread from direct molten spatter exposure.
Guangdong Ming Shun Labour Protective Products Co., Ltd. operates in Gaozhou, the epicenter of global leather safety manufacturing. Unlike traders who broker cut panels between disparate vendors, our single-roof manufacturing infrastructure gives worldwide private brands unmatched economies of scale.
We tan, lime, split, retan, and dye raw cowhides on site. Controlling fat-liquoring and chrome-tanning baths guarantees uniform split thickness (1.2mm – 1.4mm), elimination of oily efflorescence, and strict compliance with European REACH standards regarding Hexavalent Chromium (Cr VI < 3 ppm).
With over 1,000 experienced factory technicians, hydraulic die-cutting clickers, and computerized sewing lines across Plant 2, Pukang Industrial Park, we execute high-volume runs without bottlenecking. Importers secure guaranteed delivery windows even during peak global procurement cycles.
Zero middleman margins. From rawhide batch procurement from international audited slaughterhouses to final carton barcode printing and palletization, our integrated cost structure delivers up to 18-24% margin improvement for overseas brand owners and Tier-1 hardware distributors.
All products undergo strict laboratory testing according to EN 12477 (Type A & B), EN 388 (Abrasion, Cut, Tear, Puncture), EN 407 (Flammability, Contact Heat, Convective Heat, Small Splashes of Molten Metal), and ANSI/ISEA 105 specifications before export clearance.
A single welding glove model cannot satisfy shipyard stick welding and clean-room precision aerospace TIG operations. Our OEM development matrix configures anatomical cuts, thermal liners, and cuff structures to specific operational profiles.
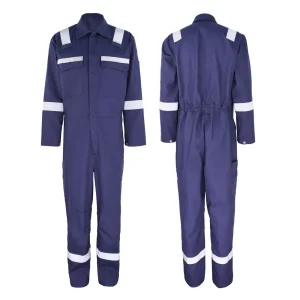
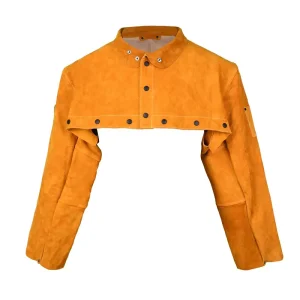
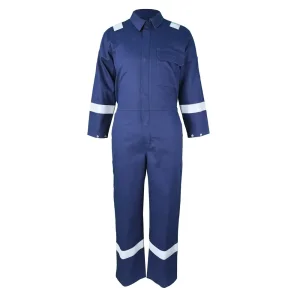
Marine construction involves prolonged exposure to salt mist, wind chill, and multi-position stick (SMAW) or flux-core welding. We equip black cowhide with hydrophobic leather tanning treatments, full cotton-fleece or aramid composite thermal barriers, and extended 14-inch to 16-inch safety gauntlets that overlap snugly over leather cape sleeves and FR work coveralls.
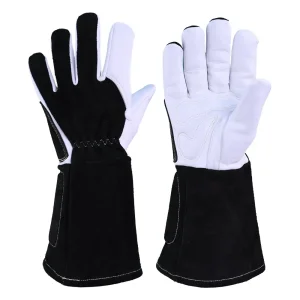
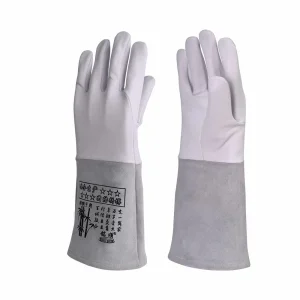
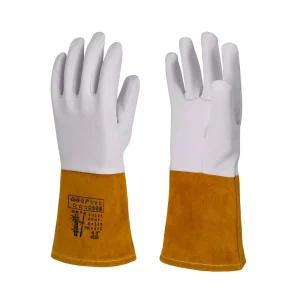
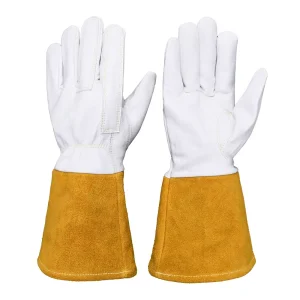
High-speed assembly plants demand gloves that allow operators to transition seamlessly between handling stamped sheet metal panels, operating MIG guns, and toggling digital touchscreens. Our hybrid goat-grain palm paired with black split cowhide cuffs delivers precision tactile dexterity (EN 12477 Type B standard) while preventing cut lacerations from raw sheet metal burrs.
Pipeline downhill welding entails relentless radiant heat and prolonged gripping of high-vibration grinding wheels. We integrate winged or keystone thumb ergonomics, palm-reinforcement patches crafted from high-density split leather, and localized vibration-absorbing silicone or foam inserts to combat hand-arm vibration syndrome (HAVS) on long shifts.
Procurement officers must calibrate testing thresholds to exact shop operations. Our OEM production lines custom-build black leather welding gloves to certified compliance tiers:
| Performance Characteristic | Test Standard | EN 12477 Type A (Heavy MIG/Stick) | EN 12477 Type B (High Dexterity TIG) | Ming Shun OEM Factory Capability |
|---|---|---|---|---|
| Abrasion Resistance | EN 388 (Cycles) | Level 2 (500 Cycles) | Level 1 (100 Cycles) | Up to Level 4 (8,000 Cycles) with reinforced palm |
| Blade Cut Resistance | EN 388 (Index) | Level 1 (Index 1.2) | Level 1 (Index 1.2) | Level 3 to Level 5 with Para-aramid Kevlar® knit lining |
| Tear Resistance | EN 388 (Newtons) | Level 2 (25 N) | Level 1 (10 N) | Level 4 (> 75 N) using Grade-A shoulder split cowhide |
| Puncture Resistance | EN 388 (Newtons) | Level 2 (60 N) | Level 1 (20 N) | Level 3 to 4 (> 100 N) optimized for handling wire slag |
| Contact Heat Threshold | EN 407 (Threshold Time) | 100°C for ≥ 15 seconds | 100°C for ≥ 15 seconds | Up to 350°C for ≥ 15s using multilayer insulation |
| Small Molten Metal Splashes | EN 407 (Number of Drops) | Level 3 (≥ 25 Drops) | Level 1 (≥ 15 Drops) | Exceeds 35 drops with mineral-treated black cowhide |
| Finger Dexterity Pin Test | EN 420 (Smallest Pin Ø) | Level 1 (≤ 11 mm) | Level 4 (≤ 6.5 mm) | Precision seamless trigger cuts achieving ≤ 5.0 mm |
In an era of rising freight costs and stringent supply chain ESG compliance, chief procurement officers are actively replacing fragmented trading agents with direct factory contracts. Here is how Ming Shun addresses modern enterprise procurement requirements.
Third-party traders depend on secondary workshops that halt production during seasonal labor shifts. Ming Shun’s 1,000+ permanent staff, based in Gaozhou's stable manufacturing corridor, guarantees predictable 40- to 45-day cycle times from purchase order issuance to Free-on-Board (FOB) dispatch at Shenzhen, Guangzhou, or Hong Kong ports.
International regulatory compliance no longer tolerates unvetted chemical agents. Our tanneries maintain full water treatment systems, zero aromatic amines, and verified Azo dye-free certifications. Every batch of dyed black cowhide is documented with lot numbers, ensuring compliance with EU Timber/Leather regulations and US EPA guidelines.
We provide complete OEM personalization: hot-foil leather branding, high-frequency embossing, woven wrist badges, custom rubberized cuff logos, multilingual cardboard hangtags, and retail-ready polybags with custom barcode mapping tailored for automated warehouse distribution systems.
Everything you need to know about lead times, customization, minimum order quantities, and test certifications before issuing a formal Request for Quotation (RFQ).
For custom-branded production runs requiring dedicated hide dyeing, customized size grading (Sizes 8/M to 12/XXL), and branded hangtags, our standard MOQ is typically 1,200 to 2,400 pairs per style. For catalog standard designs with your brand logo stamped on the cuff, smaller initial trial orders can be evaluated.
Split cowhide is derived from the fibrous lower layer of the hide after the top grain is separated. It offers superior resistance against mechanical puncture and direct flame shrinkage compared to grain leather, which can harden when exposed to extreme radiant heat. Grain leather (such as goatskin) is preferred on TIG gloves for tactile dexterity, whereas split cowhide is the industry gold standard for MIG and Stick welding.
Yes. We collaborate directly with certified European notified testing bodies (such as CTC, SATRA, and SGS). Brand owners can register as secondary license holders of our existing CE Type Examination Certificates, or we can submit production samples under your private brand name for independent testing protocols prior to commercial export.
Upon receipt of your tech pack, physical reference sample, or design brief, our pattern department drafts digital templates within 48 hours. Counter-samples with designated leather thicknesses, Kevlar® stitching, and inner linings are fabricated and dispatched via express courier within 7 to 10 working days for buyer fitment and arc trials.
In our in-house dye house, leather drum dye formulations use specialized metal-complex dyestuffs and penetrating fat-liquors, followed by cationic fixation rinsing. This ensures an ISO 105-X12 crocking test rating of Level 4 or higher for dry rubbing and Level 3-4 for wet rubbing, guaranteeing zero dye leaching under heavy perspiration.
We support FOB (Shenzhen, Guangzhou, Foshan), CIF, and CFR sea freight operations, as well as EXW factory dispatch. Standard financial terms for confirmed OEM contracts include T/T (30% deposit with balance upon presentation of Bill of Lading copy) and Irrevocable Letters of Credit (L/C at sight) for established industrial volume buyers.
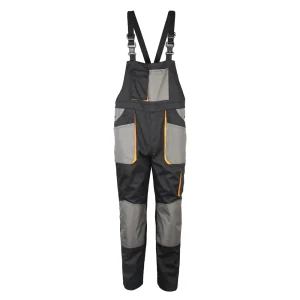
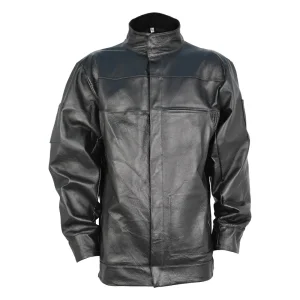
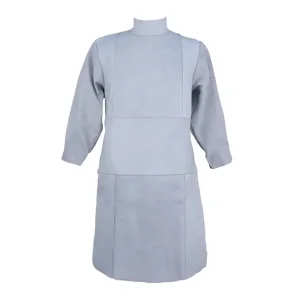
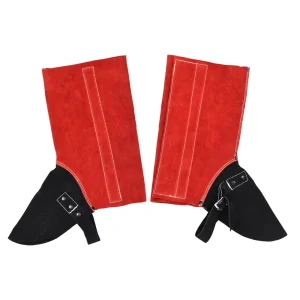
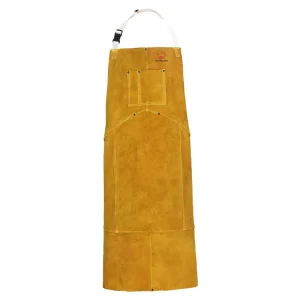
Expand your brand catalog with our complete line of heavy-duty welding jackets, split leather aprons, protective spats, and specialized accessories manufactured to the same exacting standards.