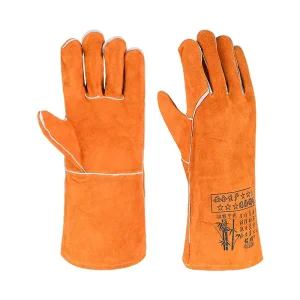
Explore heavy-duty PPE units manufactured directly inside our integrated Gaozhou facility with high-density Kevlar stitching and split-cowhide architecture.

Why modern multi-process fabrication yards are retiring single-application welding gauntlets in favor of engineered all-around thermal systems.
Modern pipe welding and structural fabrication rarely isolate SMAW (Stick), GMAW (MIG), and GTAW (TIG). Welder-fitters continuously switch between tacking, root-pass welding, heavy capping, and angle-grinder beveling. OEM all-round welding gloves eliminate continuous glove changeouts, significantly reducing micro-downtime across assembly lines.
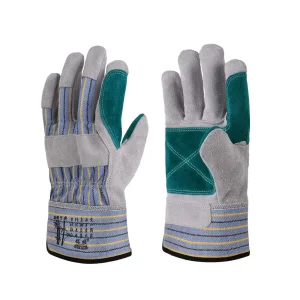
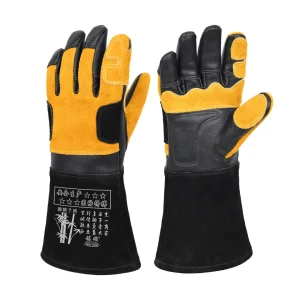
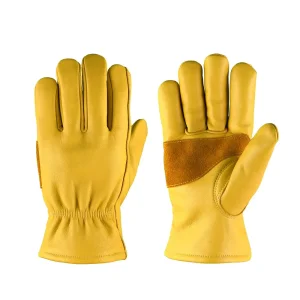
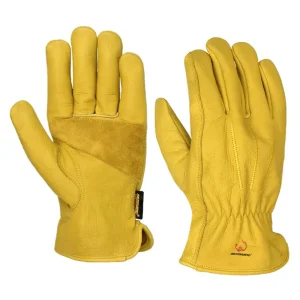
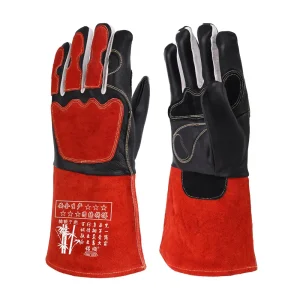
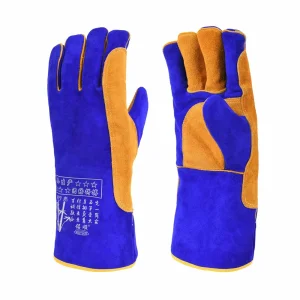
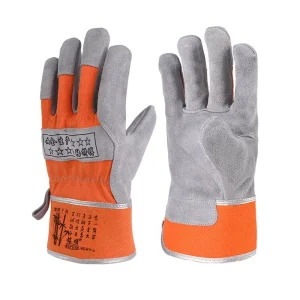
Traditional welding gloves utilized uniform split leather, sacrificing tactility for burn protection. Next-generation all-round gloves utilize a hybrid architecture: ultra-supple Grade-A grain goatskin palms for wire-feed sensitivity, reinforced split-cowhide dorsal zones for radiant heat dissipation, and aluminized backing inserts for high-amp reflection.
Welding PPE is no longer assessed solely under EN 407/EN 12477 thermal parameters. Sheet metal handling, plasma slag chipping, and deburring require cut resistance up to ANSI A4 / EN 388 Level D. Integrating Para-Aramid/Kevlar knitted liners provides full mechanical cut defense without compromising dexterity.
Our OEM gloves undergo accredited third-party validation under both European CE and North American ANSI regimes, bridging the gap between Type A (Heavy Heat) and Type B (High Dexterity).
| Testing Standard | Parameter Evaluated | Industry Standard (Type A) | Ming Shun All-Round Spec | Operational Compliance Impact |
|---|---|---|---|---|
| EN 12477:2001+A1:2005 | Welding PPE Classification | Type A or Type B Isolated | Dual Type A & B Compliant | Enables both root-pass finger touch and heavy multi-pass thermal endurance |
| EN 407:2020 | Contact Heat Resistance | 100°C for ≥ 15 seconds | 250°C for ≥ 18 seconds (Level 2) | Prevents conductive burns during continuous hot-pipe stabilization |
| EN 388:2016+A1:2018 | Abrasion & Blade Cut | Abrasion Level 2, Cut Level 1 | Abrasion 4, Cut Level C / ANSI A3 | Resists razor-sharp laser-cut edges and abrasive slag debris |
| ISO 13997 / ASTM F2992 | Seam Thermal Integrity | Standard Cotton/Nylon Thread | Dupont™ Kevlar® 4-Ply Lockstitch | Seams do not burst when exposed directly to molten spatter and sparks |
| ISO 17075-1:2017 | Chromium VI Chemical Safety | < 3.0 mg/kg Threshold | ND (Non-Detectable < 0.5) | Prevents occupational dermatitis under heavy sweat conditions |
Why Guangdong Ming Shun's vertical integration in Pukang Industrial Park, Gaozhou establishes unbeatable consistency and margin protection for international brand owners.
Unlike assembly-only cut-and-sew workshops that purchase inconsistent leather lots, we control fat-liquoring, chrome tanning, and water-repellent conditioning from raw hide intake. Every hide's tensile strength and pH value is standardized.
Pattern deviations translate into hand fatigue. Our digital nesting and computer-controlled CNC oscillating knife cutting lines eliminate dimensional variance across tens of thousands of glove finger gussets and keystone thumbs.
Every pair is inspected across 5 checkpoints: raw hide fiber density, seam tension, welt completeness, Kevlar thread lock verification, and inner lining adhesive integrity before retail-ready barcode packaging.
With 1,000+ factory staff and 500,000+ monthly glove pairs, our typical order fulfillment averages 45 days. We cushion international buyers against global shipping bottlenecks through structured buffer inventory programs.
Specific performance formulations matched to environmental friction, localized heat dissipation, and micro-dexterity demands across heavy industry sectors.
Water-resistant tanned cowhide coupled with oil-repellent grain finishes prevents salt-mist embrittlement on deep-sea rig jacket welds and high-pressure steam pipelines.
Continuous pre-heat environments up to 200°C require radiated heat shielding. Reinforced aluminized dorsal inserts prevent radiant skin scalding during 100% X-ray certified root passes.
High-tactility goatskin grain thumbs allow operators to rapidly switch between robotic fixture clamping, MIG seam tracking, and thin-gauge metal bracket fitting without glove removal.
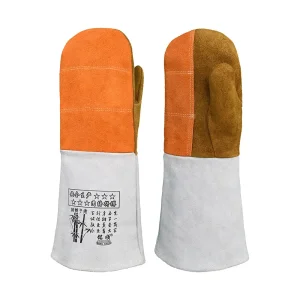
Heavy split cowhide cuffs with full leather welted seams withstand falling overhead spatter, flux chipping hammer impacts, and gouging slag across double-bottom tank fabrication.
Full Kevlar stitching throughout the fingers prevents blowouts when gripping abrasive I-beams, while ANSI Cut Level 3 liners shield fitters against rough torch-cut edge lacerations.
How our OEM/ODM infrastructure empowers hardware chains, safety distributors, and private brands to capture market share with reliable unit economics.
A glove failure on an industrial site results in catastrophic liability and brand damage. Our standardized production parameters, documented batch-lot retention samples, and CE/ANSI test certificates protect distributor reputations in mature Western regulatory jurisdictions.
By integrating tannery operations, automated cutting, and direct logistics, we compress product costs by 15-28% compared to multi-tier trading entities. Importers achieve higher distributor gross margins while delivering competitively priced PPE to tier-1 contractors.
From embossed wrist logos, high-contrast silicone palm grips, custom Pantone leather dyeing, and ergonomic keystone thumb re-engineering to bilingual hangtags and retail-shelf master cartons, our technical pack department turns your brand sketches into reality in under 7 business days.
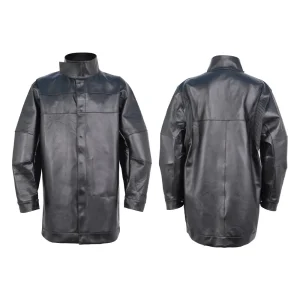
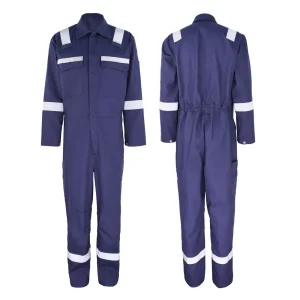
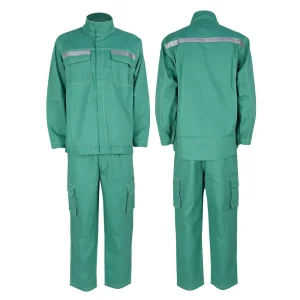
Complete your catalog with high-performance FR coveralls, split-leather jackets, water-resistant utility gloves, and heavy-duty workwear.
Direct technical answers addressing the critical parameters procurement heads and commercial buyers evaluate before issuing requests for quotation (RFQs).
Dedicated Stick gloves utilize thick (1.2–1.4mm) split cowhide with heavy fleece linings, providing high heat isolation but zero finger tactility. TIG gloves use thin (0.7–0.9mm) goatskin without lining, which scorches instantly under heavy MIG or stick slag. An all-round glove blends a 0.9–1.0mm premium grain goatskin or pigskin palm for wire-feed feel with a heat-dissipating split cowhide back, full Kevlar welting, and a flame-retardant cotton lining, allowing welders to perform multi-process welding and grinding safely without changing gear.
Conventional nylon or polyester sewing threads combust at 180°C–220°C, leading to catastrophic glove seam separation during spatter contact. Ming Shun exclusively deploys 100% genuine DuPont™ Kevlar® 3-ply and 4-ply aramid thread with concealed full-leather welts along every finger seam. Kevlar resists decomposition up to 450°C and does not melt, ensuring structurally intact glove geometry even under extreme droplet impingement.
Yes. Because we control internal leather processing in Gaozhou, our chemical tanning engineers formulate specialized batches: silicone-tanned water-resistant leather for wet shipyard applications, fat-liquored conditioning to maintain pliability down to -25°C for Nordic/Canadian winter job sites, or chrome-free (aldehyde-tanned) leathers for sensitive skin programs.
Our standard OEM sampling turnaround is 5 to 7 business days against an approved tech pack or customer counter-sample. For customized private-label production (custom color leather, branded heat stamps, woven wash tags, and retail blister cards), our production line MOQ begins at 1,200 pairs per size/style, with full-container 20GP/40HQ volume pricing available for wholesale distributors.
Every leather lot undergoes rigorous batch testing in accordance with ISO 17075-1:2017 for Chromium VI content, verifying non-detectable levels (<0.5 mg/kg), along with azo dyes, formaldehyde, and pH tests according to EU REACH Regulation (EC) No 1907/2006. Accredited test reports from SGS, TÜV, or SATRA are provided directly with pre-shipment quality inspection files.
We strongly recommend our Keystone Thumb or 3D Ergonomic Wing Thumb designs with seamless index finger construction. The keystone thumb follows the natural anatomical curvature of the human resting grip, eliminating seam pressure points along the inside crotch when holding torch handles or electrode stingers for extended 8-hour welding shifts.

