
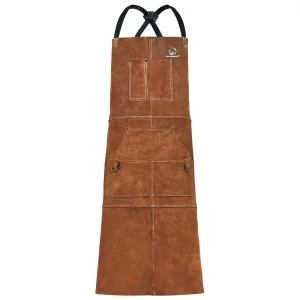
Direct manufacturing solutions covering multi-tier personal protective equipment, extreme weather hand safety, and flame-retardant welding configurations ready for bulk institutional procurement.
The industrial hand protection sector has long struggled with the fundamental trade-off between convective thermal insulation and manual dexterity. Traditional heavy-loft insulation packs inhibit palmar tactile sensitivity, increasing worker fatigue and driving compliance failure in sub-zero operational environments.
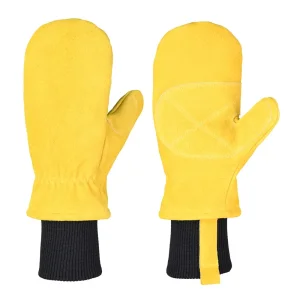
As a leading custom winter work gloves manufacturer, our engineering department integrates multi-layered membrane architectures. By pairing hydrophobic-treated grain goat or split cowhide with micro-thin, dense synthetic insulations (such as 100g–200g Thinsulate™ formulations) and windproof-breathable TPU inserts, we prevent moisture freeze-out without sacrificing grip efficiency.
Human blood circulation in extremities decreases rapidly when ambient temperatures fall below 10°C (50°F), dropping grip strength by up to 55%. Industrial gloves must defend against three specific heat-loss vectors:
Operating from our integrated Gaozhou industrial base, we blend 25+ years of tanner craft with automated nesting algorithms, high-efficiency cutting tables, and real-time production analytics.
By controlling raw leather tanning, split selection, dye baths, and fatliquor stabilization internally, we eliminate third-party supply delays and guarantee batch-to-batch leather tensile strength and cold crack resistance down to -40°C.
Our advanced sewing cells integrate computerized Kevlar® and Dyneema® stitching. Structural wear points, thumb crotches, and fingertip seams are reinforced using high-precision CNC lockstitch machines to avoid stress blowouts.
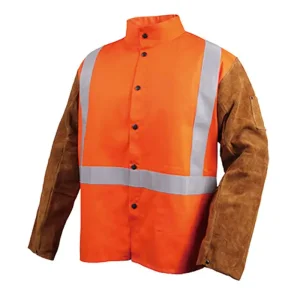
Tech packs are converted into production prototypes in 5–7 days. We engineer bespoke TPR impact exo-skeletons, custom high-visibility color blocks, customized cuff lengths, and private branding for global importers and distributors.
Navigating cross-border compliance demands rigorous testing parameters. Our production protocols conform to both European and North American industrial PPE directives.
| Performance Criterion | EN 511 (European Directive) | ANSI/ISEA 105 (North American) | Ming Shun Engineering Standard |
|---|---|---|---|
| Convective Cold Insulation | Level 0–4 (Thermal resistance ITR) | Conductive Thermal Resistance | Level 3–4 High Convective Rating |
| Contact Cold Resistance | Level 0–4 (Thermal resistance R) | ASTM F1060 Surface Contact | Tested to -30°C / -40°C Continuous |
| Water Permeability | Level 0 (Failed) or 1 (No penetration 30m) | Waterproof / Water-repellent Hydrostatic | Pass Level 1 (5,000mm Breathable TPU) |
| Mechanical Abrasion & Tear | EN 388:2016 (4X43EP) | ASTM D3884 / D2261 Standards | Grade-A Heavy Cowhide / Reinforced Palm |
| Pinch & Metacarpal Impact | EN 13594:2015 6.8.2 Attenuation | ANSI/ISEA 138 Levels 1–3 | Custom Low-Temp Flexible Sonic TPR |
From Nordic offshore gas platforms to North American intermodal cold-chain warehousing, our thermal workwear is specified where standard commercial gloves fail.
Oil-resistant hydrocarbon proofing on grain leather shells combined with high-impact metacarpal bumpers. Remains elastic and crack-proof at extreme -40°C wind-chill ratings.
Optimized for high-cadence barcode scanning, pallet handling, and sub-zero blast freezer operations (-25°C to -30°C). Incorporates anti-slip siliconised leather grip patterns.
Cut-resistant A5/A6 inner liners protect structural ironworkers and rebar crews against jagged metal corners, icy steel beams, and heavy abrasive aggregate impacts.
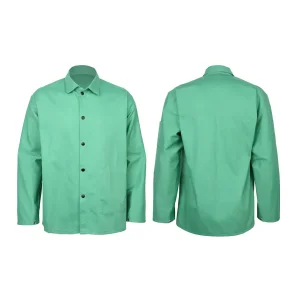
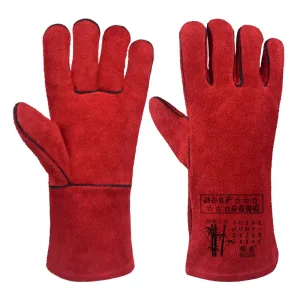
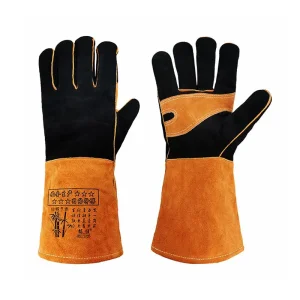
Specialized hybrid mitts and gauntlets using flame-resistant split cowhide lined with flame-retardant wool-cotton blends to defend against simultaneous molten spatter and freezing air.
Authoritative insights addressing MOQs, technical test protocols, material choices, and private label customization for safety procurement directors.
For standard customized winter work glove configurations (using in-stock tanned cowhide or goatskin), our baseline MOQ starts at 1,200 to 2,400 pairs per style. Bespoke colorways, custom rubberized TPR mold tooling, or specialized proprietary membrane integrations generally require an MOQ of 3,600 pairs.
We apply specialized synthetic fatliquors and chromium/synthetic tanning cocktails in our in-house drum cycles. This prevents the leather collagen fibers from crystallization and micro-cracking when exposed to severe sub-zero thermal cycling, preserving flexibility down to -40°C.
Yes. As an established OEM/ODM contract manufacturer, we facilitate third-party laboratory verification (via CTC, SATRA, or SGS). We supply formal Declaration of Conformity (DoC), technical construction files (TCF), CE certificates, and customized label placement matching destination customs criteria.
Pre-production sample sign-offs are completed within 5–7 business days. Bulk production for full container load (FCL) orders typically spans 35 to 45 calendar days following lab-dip and spec approval, backed by our ERP capacity forecasting systems.
Review the remainder of our specialized leather apparel, insulated mittens, and high-abrasion accessories manufactured directly for worldwide distribution partners.
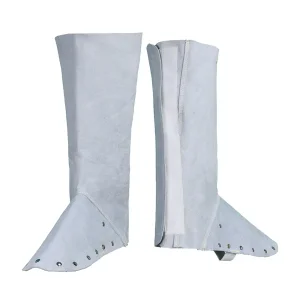
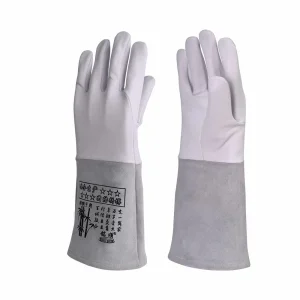
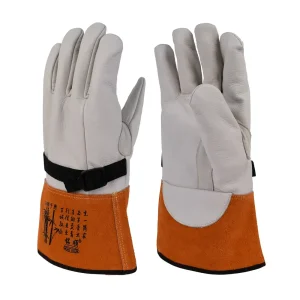
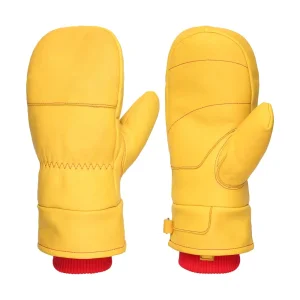
Request certified material swatches, 3D technical prototyping, and comprehensive wholesale export quotes directly from Guangdong Ming Shun's engineering team.
