Precision-manufactured in our integrated facility with audited raw hide selection, EN ISO standard adherence, and OEM custom private labeling.
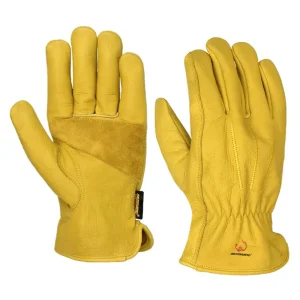
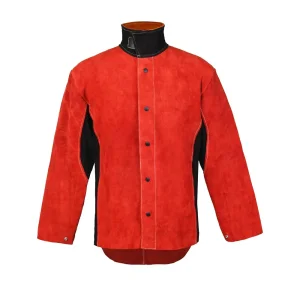
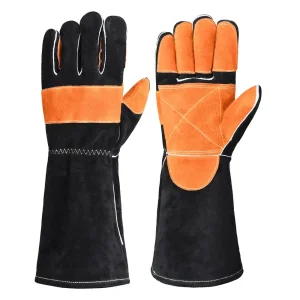
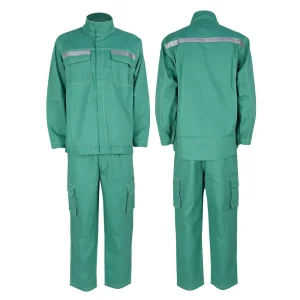
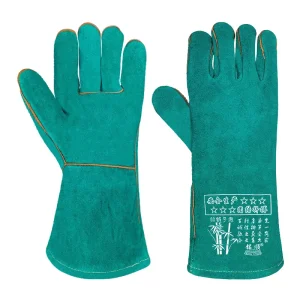
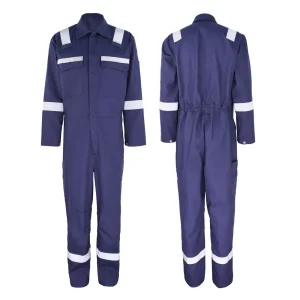
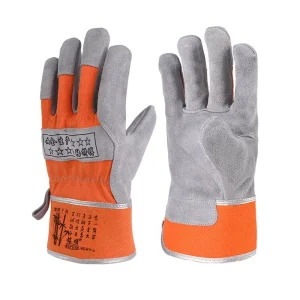
Evaluating molten droplet kinetic deflections, thermal radiant thresholds, and the ergonomic ergonomics of modular welding sleeve PPE systems across heavy automated and manual welding lines.
Forearm exposure during multi-position gas metal arc welding (GMAW) and flux-cored arc welding (FCAW) exposes operators to radiant temperatures exceeding 1,400°C in hot spatter zones. In vertical-up (3G/3F) and overhead (4G/4F) joints, gravitational splatter roll-off directly strikes the bicep-forearm juncture.
Our custom welding safety sleeves utilize premium selected 1.2mm–1.4mm cowhide split grain tanned with high heat-resisting chromium salts. The natural fibrous collagen network acts as a sacrificial ablation barrier, preventing droplet adhesion and eliminating localized skin burn trauma.
In tropical shipyards, high-ambient fabrication bays, and desert pipeline projects, heat exhaustion accounts for over 38% of non-impact downtime. Enforcing full leather jackets frequently triggers compliance failure, where welders roll sleeves up or shed upper armor entirely.
Modular custom welding safety sleeves bridge this critical behavioral gap. Paired with lightweight breathable 9 oz FR flame-retardant cotton vests or coveralls, our sleeves deliver targeted Class 2 protection exactly where spatter impinges while maximizing convective torso cooling and core thermal dissipation.
Fabrication shop operations demand rigorous contact with abrasive bevel edges, sharp plasma-cut web plates, and cold structural steel. Ordinary flame-retardant synthetic knit tubes degrade rapidly under structural shear friction.
Ming Shun split leather sleeves feature an engineered tensile resistance reaching Level 4 under EN 388 puncture and abrasion testing. Sewn exclusively with multi-filament DuPont™ Kevlar® thread, the seams withstand intense molten slag strikes without structural burst or premature thread embrittlement.
International industrial safety protocols require procurement heads to align sleeve specifications with divergent regional statutory and operational frameworks.
Governed by OSHA 29 CFR 1910.252 hot work regulations and ANSI/ISEA 105 cut/abrasion matrices. US fabricators prioritize heavy 18" to 23" split leather sleeves with bicep harness attachments to prevent slippage during continuous crane-girder stick welding.
Strict enforcement under PPE Regulation (EU) 2016/425. Demands CE certification covering EN ISO 11611 Class 1 and Class 2 (spatter test with >25 drops of molten metal). REACH compliance mandating strict zero-detectable hexavalent chromium (Cr-VI) in leather substrate.
Extreme desert conditions require hybrid composite arm protection: heavy leather panels guarding the radial exterior forearm paired with breathable flame-retardant treated gussets to sustain internal arm microclimates without heat rash formation.
Driven by high-duty flux-cored arc welding in double bottoms and cargo holds. Volume buyers demand direct-factory container logistics, batch-tested flame latency reports, and customized gauntlet overlap profiles.
At Ming Shun, every batch of cowhide split leather and FR substrate undergoes calibrated internal and third-party laboratory verification before batch release.
| Testing Standard & Clause | Target Parameter | Ming Shun Engineering Standard | Compliance Classification |
|---|---|---|---|
| EN ISO 11611:2015 Clause 6.7 | Impact of Molten Drops (Spatter) | Resists >28 drops of molten metal before 40K sensor rise (Requirement: ≥25 drops) | Class 2 Verified |
| ISO 15025:2016 Method A | Limited Flame Spread (Surface Ignition) | Afterflame time ≤ 0.5s; afterglow time ≤ 1.0s; zero burn-through or hole formation | Pass (Index 3) |
| EN 388:2016+A1:2018 Clause 6.1 | Abrasion & Tear Resistance | Split hide exceeds 8,000 cycles (Level 4); tear strength exceeding 110N across grain axes | Level 4 Max Tier |
| ISO 17075-1:2017 | Chemical Safety: Hexavalent Chromium | Non-detectable (<3.0 mg/kg limit of detection); REACH Annex XVII compliant | Zero Cr-VI Pass |
| ASTM F1060 / NFPA 2112 | Conductive & Contact Heat Resistance | Time to 2nd-degree burn exceeds 14.8 seconds under 250°C contact pressure | Industrial Heavy Tier |
Engineered sleeve adaptations developed for specialized hot-work operating theaters worldwide.
Confined void spaces require ultra-durable leather arm guards with elastic cinch rings that prevent sparks from falling inside gloves during overhead 4G butt-welding.
Robotic cell operators handling weld spatter cleanouts require lightweight hybrid cowhide/FR cotton sleeves offering supreme wrist articulation and touch-up speed.
Cellulosic stick downhill welding creates torrential spark showers. Extended 23-inch cowhide split sleeves with brass hook-and-loop neck drapes ensure full arm-to-collar protection.
Precision GTAW welding on Inconel and titanium requires non-linting, supple top-grain goatskin or lightweight split leather sleeves providing zero tactile resistance.
Carbon arc gouging produces severe molten metal blowback. Extra-thick 1.4mm split hide sleeves with double Kevlar® reinforced seams are essential to prevent blow-through.
Leading the transition from traditional passive barrier leather towards high-ergonomic, climate-adaptive hot-work extremity protection.
Closed-loop in-house leather tanning ensuring uniform density, chrome-stabilization, and customized pre-stretch treatments that stop shrinkage after intense thermal exposure.
Curved 3D sleeve patterning matching natural human elbow flexion angles, reducing operator fatigue during 10-hour structural assembly shifts.
Integration of micro-encapsulated PCM (phase change material) interior linings that absorb body heat, keeping skin temperatures up to 4°C cooler under heavy radiant welding arc flux.
100% chrome-free vegetable/synthetic hybrid tanning matrices meeting stringent future EU environmental zero-discharge mandates without degrading thermal ablation resistance.
Straight answers regarding customized welding safety sleeves, minimum order volumes, material grades, and private-label programs from Ming Shun engineering staff.
Split cowhide (1.2mm–1.4mm) offers heavy physical molten splatter deflection and mechanical cut/tear resistance rated to EN ISO 11611 Class 2. Molten droplets roll off without scorching through. FR cotton (9 oz to 11 oz) is lighter and more breathable (Class 1), making it ideal for lighter TIG or low-amperage MIG welding in hot environments. For heavy MIG, stick (SMAW), or gouging, split cowhide or hybrid leather-front/FR-back sleeves are strongly recommended.
Yes. We specialize in custom OEM/ODM production. Standard sleeve lengths range from 18 inches (45 cm) to 23 inches (58 cm). Closures can be engineered with heavy-duty elasticated bands, non-conductive flame-resistant hook-and-loop straps, adjustable metal snap fasteners, or crossover shoulder harness suspenders. Wrists can be built with elastic gathers, split cowhide gauntlet bell cuts, or soft ribbed FR knit cuffs based on your tech pack.
All Ming Shun leather welding protective gear is stitched with genuine 3-ply or 4-ply Kevlar® para-aramid thread. Kevlar® does not melt, conduct flame, or degrade until temperatures exceed 427°C (800°F). In high-stress zones, we incorporate leather welt seams that enclose the thread inside the hide layers, preventing direct molten metal contact from severing the stitch line.
We provide complete technical files and accredited test reports for CE certification under PPE Regulation (EU) 2016/425, specifically EN ISO 11611 (protective clothing for welding) and EN 388 (mechanical risks). For North American buyers, our lab verifies conformance with ANSI/ISEA 105 and ASTM hot-work performance specifications. We also provide REACH chemical conformity documents proving zero detectable Hexavalent Chromium (Cr-VI) and azo dyes.
Standard MOQ for customized sleeve designs with private logo branding (embossing, woven label, or silk-screen heat transfer) is typically 1,200 pairs. Prototype counter-samples from your tech pack are dispatched in 7–10 days. Bulk production lead time is approximately 35–45 days post sample approval, backed by our monthly manufacturing capacity exceeding 500,000 glove and sleeve pairs.
Direct-factory industrial protective gear engineered to complement your arm safety program with coordinated spats, jackets, overalls, and high-temp gloves.
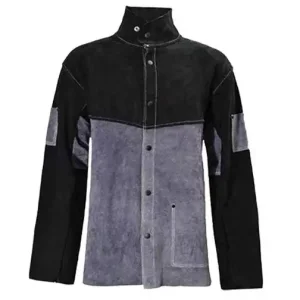
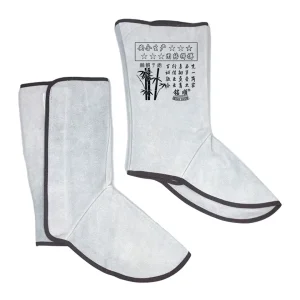
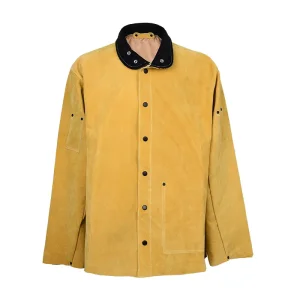
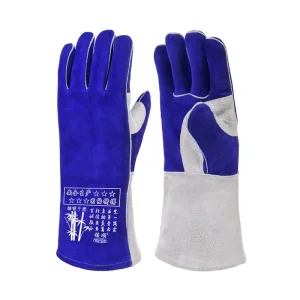
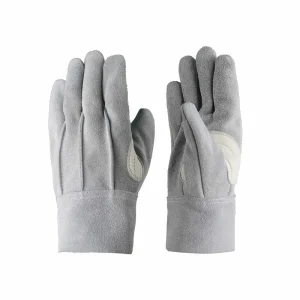

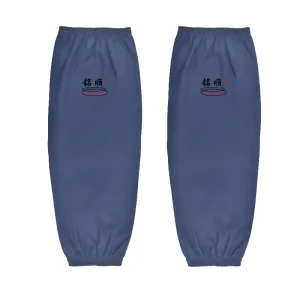
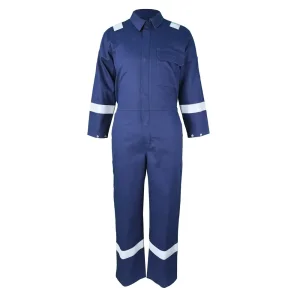
Partner directly with a 25-year PPE manufacturer. From raw split leather selection and custom pattern CAD adjustments to verified CE/ANSI compliance and container-load exports, our engineering team is ready to scale your private-label program.
Request Quotation & Prototype Samples
