Engineered from premium split cowhide, top-grain goatskin, and flame-retardant composites. Certified to EN 388, EN 407, and EN 12477 heavy fabrication thresholds.
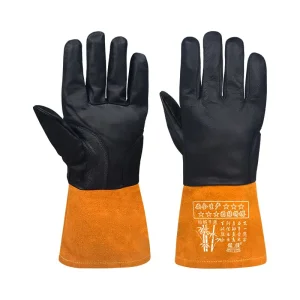
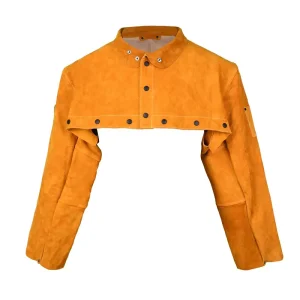
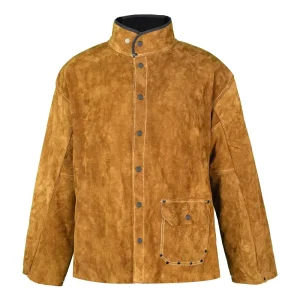
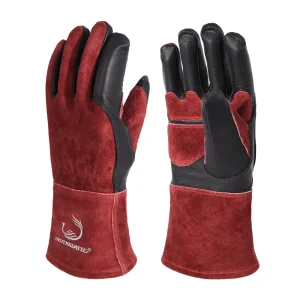
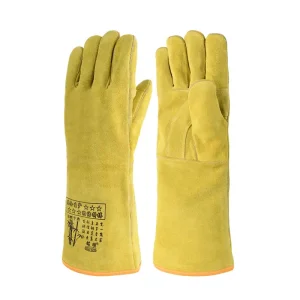
The global industrial hand protection market is undergoing a structural transition from commoditized throwaway equipment to engineered, task-customized Personal Protective Equipment (PPE). Driven by stringent workplace safety mandates and ergonomic standards, multinational enterprises demand quantifiable protection coefficients.
Global regulatory enforcement under OSHA (USA), EU PPE Regulation 2016/425 (Category II and III), and Safe Work Australia has eliminated gray-market sourcing. Safety hand gloves suppliers must provide authenticated CE Declarations of Conformity, EN 388:2016+A1:2018 mechanical wear certifications, and EN 407:2020 contact heat data.
Modern hand safety engineering balances tensile leather integrity with ultra-high molecular weight polyethylene (UHMWPE) and aramid fiber engineering. While chrome-tanned split cowhide remains indispensable for molten spatter barrier defenses, goatskin blends allow micro-tactility necessary for high-amperage TIG/MIG automation lines.
Procurement directors are shifting from unit-purchase-price evaluation to wear-life lifecycle assessments. By adopting reinforced DuPont™ Kevlar® stitching, welted seam architecture, and reinforced palm patches, enterprise buyers achieve a 40% reduction in annual glove turnover and significant injury reduction.
Operating from the Pukang Industrial Park in Gaozhou, Guangdong—the heart of the world's premier leather processing and protective gear cluster—Guangdong Ming Shun Labour Protective Products Co., Ltd. delivers distinct supply chain advantages.
The Gaozhou Vertical Advantage: By operating our own specialized tanneries, precision computerized dye baths, automated hydraulic die-cutting tables, and over 1,000 skilled sewing artisans under unified quality protocols, Ming Shun controls the physical attributes of protective gear from green hide to carton packaging.
We source Grade-A cattle, goat, and pig hides, categorizing raw stock by grain density, tensile flex, and fiber thickness (1.1mm to 1.4mm calibration) to eliminate structural soft spots prior to cutting.
Advanced retanning baths yield low-chromium, neutral-pH leathers that comply with strict EU REACH restrictions (specifically Hexavalent Chromium Cr VI < 3ppm), ensuring dermatological safety for operators.
Automated nesting software optimizes yield and panel cutting precision down to fractions of a millimeter. Every finger panel, thumb gusset, and reinforcement patch conforms to ergonomic patterns.
Quality checks are executed at material intake, post-cut sizing, in-line stitching validation, and pre-shipment container audits, ensuring AQL 1.5 / 2.5 acceptance thresholds for international export.
When enterprise procurement officers source custom safety hand gloves, compliance documentation must be verifiable. Below is an engineering comparison of protective glove standards deployed in our laboratory testing.
| Regulatory Standard | Target Protection Factor | Performance Metrics / Test Methods | Target Industrial Domain | Ming Shun Engineering Standard |
|---|---|---|---|---|
| EN 388:2016+A1:2018 | Mechanical Hazards | Abrasion (1-4), Blade Cut (1-5 / TDM A-F), Tear (1-4), Puncture (1-4), Impact | Metal Stamping, Fabrication, Heavy Rigging | Level 4443D Available |
| EN 407:2020 | Thermal Hazards & Fire | Burning Behavior, Contact Heat (100°C - 500°C), Convective, Radiant, Molten Splash | Foundry, Arc Welding, Smelting Operations | Contact Heat Level 1-4 |
| EN 12477:2001+A1:2005 | Welder Hand Protection | Classifies Type A (Heavy MIG/Stick, High Heat) vs. Type B (High Dexterity TIG) | Structural Steel, Pipeline, Shipyards | Full Type A & B Pass |
| ANSI/ISEA 105-2024 | North American Mechanical | ASTM F2992-15 Cut Resistance (A1-A9), Abrasion (0-6), Puncture (0-5) | Automotive Tier-1, Oil & Gas Extraction | Cut Levels A2 to A6 |
| EN ISO 21420:2020 | General Glove Requirements | Ergonomics, Dexterity Levels (1-5), Sizing, Innocent pH (3.5-9.5), Cr VI < 3mg/kg | All Industrial Sectors | Full Neutral Verification |
One single glove design cannot mitigate diverse worksite risks. As an OEM and ODM supplier, Ming Shun tailors patterns, thicknesses, linings, and gauntlets to distinct operating conditions.
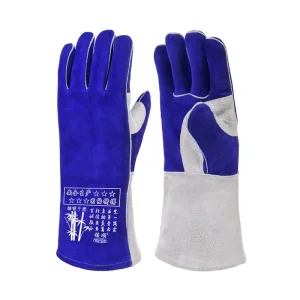
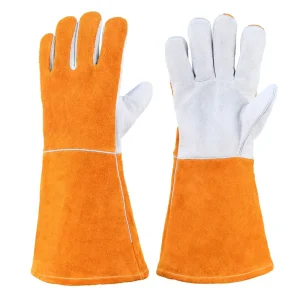
Environment: Intense slag expulsion, continuous 250A+ GMAW/FCAW arc exposure, handling burred edges.
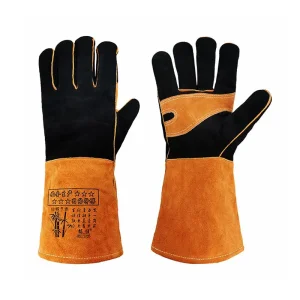
Glove Configuration: Premium heavyweight split cowhide, fully welted seams sewn with 4-ply Kevlar® thread, aluminized back-of-hand radiant inserts, and extended 14-inch to 16-inch split leather gauntlets.
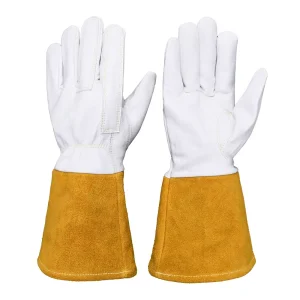
Environment: Thin alloy joining, low heat, demanding tactile filler rod feeding and torch stability.
Glove Configuration: Top-grain Grade-A goatskin palm with unlined seamless index finger construction, keystone thumb ergonomics, and pliable split cowhide safety cuffs for forearm protection without wrist restriction.
Environment: Windchill exposure, icy steel tubulars, open-flame root passes, high humidity.
Glove Configuration: Water-repellent oil-tanned split cowhide outer shell, laminated microporous thermal barriers, dense fleece or sherpa fur lining, and reinforced double-layer thumb saddles to resist rope abrasion.
From global safety equipment distributors to private labels, our production facility transforms tech packs and sample specs into scalable bulk manufacturing runs.
Select grain cowhide, split shoulder cowhide, grain pigskin, goatskin, or deerskin. Match tensile thickness (1.0mm - 1.5mm) and custom Pantone brand dye formulations.
Specify Gunn cut or Clute patterns; Keystone, Wing, or Straight thumb configurations; and seamless trigger finger profiles to reduce musculoskeletal hand strain.
Select internal liner composites: moisture-absorbing cotton jersey, brushed flame-retardant fleece, 3M Thinsulate™, or knitted Aramid / HPPE cut-resistant inner sleeves.
Apply your brand via heat transfer, high-pressure leather debossing, woven satin side tags, custom barcode hangtags, and retail-ready polybags with export master cartons.
Experienced Chief Procurement Officers evaluate beyond unit cost. Ming Shun provides transparent auditing protocols that de-risk long-distance industrial procurement.
Many cheap industrial gloves fail imported safety screenings due to residual chromium tanning agents. Ming Shun tests all leather batches for pH balance, banned azo colorants, Pentachlorophenol (PCP), and Hexavalent Chromium (Cr VI) to ensure customs compliance.
Glove failure typically begins at seam burn-through. We exclusively utilize multi-ply continuous filament para-aramid (Kevlar®) thread that withstands 400°C temperatures without melting, paired with full leather welting to shield stitches against radiant slag erosion.
Located adjacent to major deep-water ports in Guangzhou and Shenzhen, our shipping department coordinates full-container loads (20GP, 40HQ), moisture-barrier pallet packaging, and rapid air-cargo prototyping to keep your distribution warehouses stocked year-round.
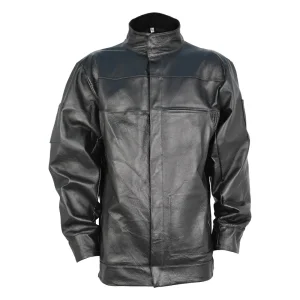
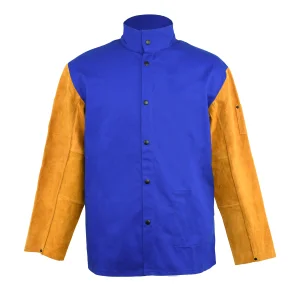
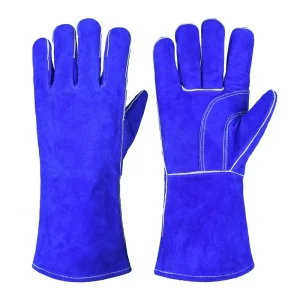
Expand your protective program with stick welding gloves, fleece-lined cold climate gear, FR hybrid jackets, and industrial mechanic workwear.
The personal protective equipment industry is evolving rapidly with modern ergonomic science, cleaner material processing, and digital supply tracking.
Traditional 2D flat glove cuts require hand muscles to fight leather resistance when gripping tools. Next-generation pre-curved fingers, 3D fourchette patterns, and accordion knuckle flex zones reduce operator grip strain by up to 28%, significantly lowering repetitive strain injuries (RSI).
Environmental, Social, and Governance (ESG) standards are moving through heavy manufacturing supply chains. Ming Shun is investing in closed-loop water recycling within our Gaozhou tanneries, vegetable-tanned alternatives, and organic leather finishes that lower chemical discharge.
Integrating molded thermoplastic rubber (TPR) along the dorsal hand surface shields metatarsal bones from crushing impacts in offshore and mining jobs, certified to ANSI/ISEA 138. Combining TPR with heat-resistant split cowhide creates versatile hybrid protection.
Clear, definitive technical answers to assist procurement directors, importers, and brand owners in vetting Ming Shun as their primary custom safety glove supplier.
Guangdong Ming Shun Labour Protective Products Co., Ltd. (formerly Gaozhou Mingshun Labor Protection Products Co., Ltd.) is an authentic source manufacturer operating in Plant 2, Industrial Avenue, Pukang Industrial Park, Gaozhou City, Guangdong. We manage over 1,000 workers, dedicated tanning drums, precision laser cutters, and over 500,000 pairs of gloves per month under our own facility roof.
For standard production runs, our typical MOQ starts at 1,200 to 3,000 pairs depending on leather grade and customization requirements. Standard production turnarounds average approximately 45 calendar days after pre-production sample sign-off. High-volume container programs (20GP/40HQ) benefit from staged monthly dispatch schedules.
Yes. We regularly supply safety gloves engineered to meet CE EN 388 (mechanical risks), EN 407 (thermal hazards), EN 12477 (welding Types A & B), and ANSI/ISEA 105 criteria. Model-specific test reports and CE type-examination certificates from notified testing bodies (such as CTC, SATRA, or SGS) are coordinated during product development.
Because we operate our own specialized tanning drums and leather processing lines in Gaozhou, our technicians control tanning chemistry, dye concentrations, and hide splitting thicknesses in-house. This internal control prevents the color shifts and texture variations common with trading firms that rely on fragmented open-market scrap leather.
We offer comprehensive private-label integration: deep-strike leather embossing, durable heat transfers, silk-screen printing, woven brand labels along the safety cuff seams, custom multilingual instruction manuals, barcode hangtags, and retail-ready polybags or carton packaging engineered to your branding guidelines.
Clients provide a technical tech pack, CAD drawing, or physical benchmark sample. Our master pattern cutters construct a prototype within 7 to 10 working days, accompanied by full material specification sheets. Once physical fit, seam positioning, and tactile dexterity are approved, production commences.

