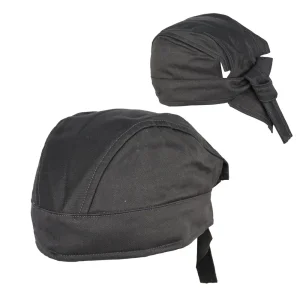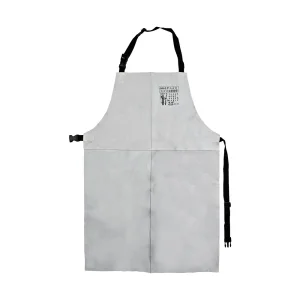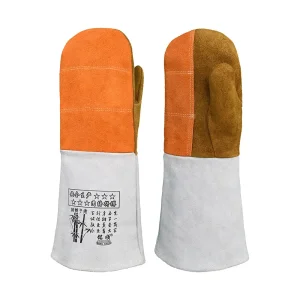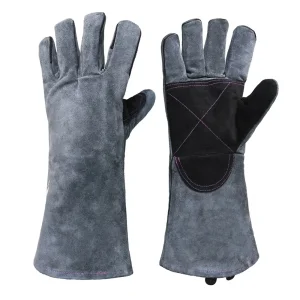
Engineered across ISO 9001 and EN 12477 Class A/B certified production lines. Explore factory-direct product variants designed for MIG, TIG, heavy stick welding, and multi-risk foundry metallurgy.
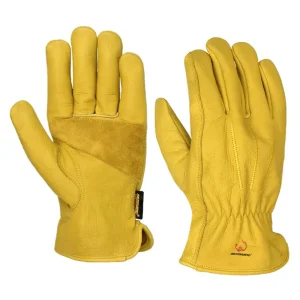
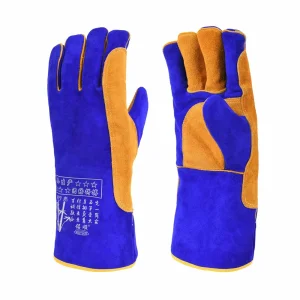
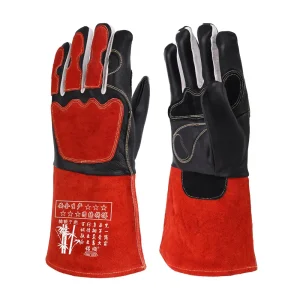
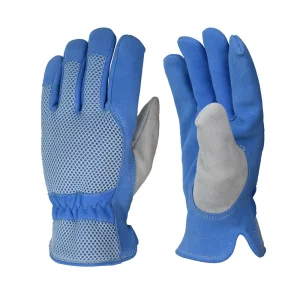
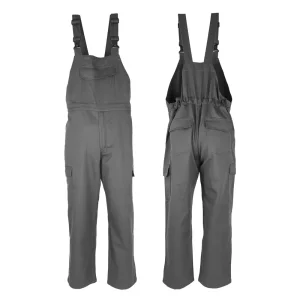
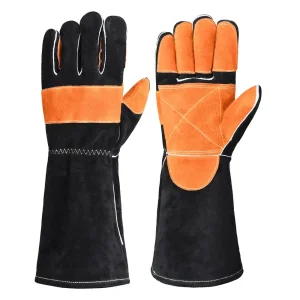
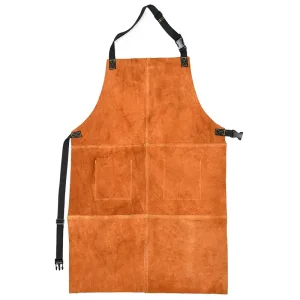
As automated welding lines, offshore maritime structures, and aerospace engineering demand higher safety metrics, the global market for specialized thermal protective equipment has shifted towards high-density grain leathers, multi-layer composite insulations, and strict traceability protocols.
Global supply chains require scalable direct-source factories capable of absorbing raw material volatility. Direct tannery integration enables high-volume manufacturing without compromising hide consistency, essential for large procurement contracts.
Industrial compliance standards such as EN 12477 (Class A/B), ANSI/ISEA 105, and ISO 11611 demand verifiable laboratory testing covering convective heat transfer, molten metal splash resistance, and contact heat thresholds.
Modern heavy-duty welding gloves combine Grade-A split cowhide with heat-deflecting aluminized fabrics and para-aramid threading (DuPont Kevlar®) to maximize tear resistance and prevent seam breakdown under radiant heat.
Understanding the transition from basic split leather hand protection to high-dexterity, multi-hazard ergonomic protection.
Transition from stiff unlined cowhide to 3D pre-curved keystone thumb and gunn-cut patterns lined with moisture-wicking FR cotton, mitigating repetitive strain injury during prolonged continuous passes.
Integration of high-dielectric grain goatskin and calfskin shells in TIG/MIG lines to eliminate electrical breakdown arcs during high-frequency pulse initiation.
Chrome-VI free tanning and reduced formaldehyde chemical finishes compliant with strict EU REACH regulations, preventing occupational dermatitis and hazardous emissions under heat exposure.
Barcoded batch tracking and standardized batch-testing documentation built directly into OEM manufacturing supply chains to facilitate seamless import safety clearance.
Engineering breakdown of leather grades, stitch reinforcements, and thermal insulation ratings for critical manufacturing decisions.
| Classification | Primary Substrate | Thermal Barrier | Tensile Seam System | Contact Heat Resistance | Applicable Industries |
|---|---|---|---|---|---|
| Heavy MIG / Flux-Core | 1.2–1.4mm Heavy Split Cowhide | Insulated Fleece + Flame-Retardant Foam | 4-Ply DuPont Kevlar® Welted Seams | 350°C to 500°C (Up to 15s) | Shipbuilding, Heavy Structural Steel |
| Precision TIG Welding | 0.8–1.0mm Premium Top-Grain Goatskin | Unlined / Lightweight FR Seamless Cotton | Para-Aramid High-Tensile Thread | 100°C to 200°C (High Tactility) | Aerospace, Pressure Vessel, Pipe Line |
| Foundry & Molten Splash | Aluminized Backing + Split Cowhide Palm | Multi-Layer Silica Fabric + Aerogel Composite | Triple Kevlar® Continuous Lock-Stitch | 500°C+ (Radiant Heat Shielding) | Smelting, Automotive Castings, Forges |
| Multi-Risk Utility / Stick | Selected Grain Pigskin / Split Cowhide | Laminated FR Cotton Canvas | Reinforced Palm & Thumb Saddle | 250°C to 350°C (Abrasion Resistant) | Mining Maintenance, Oil & Gas Pipelines |
Tailored thermal and mechanical glove configurations deployed across demanding industrial production environments.
High salinity, heavy multi-pass welding, and constant abrasive surface friction. Requires water-resistant treatments paired with Class A thermal resistance.
Critical root-pass pipe welding requiring supple goatskin palms for rod manipulation combined with heavy split leather cuffs to resist hot slag rollback.
Repetitive high-speed resistance and robotic MIG cell assistance. Emphasizes palm vibration damping, high cut ratings (ANSI A4+), and heat deflection.
Extreme radiant temperature spikes exceeding 800°C. Managed through custom aluminized backings, split leather aprons, and multi-layer thermal shielding.
High amperage arc gouging, continuous beveling, and heavy handling of pre-heated steel plates requiring double-layer reinforced palm patches.
How direct partnership with an integrated manufacturing facility eliminates supply-chain vulnerabilities for safety brands and large distributors.
Unlike small assembly workshops that source split leather on speculative open markets, an integrated facility with internal hide processing controls chromium content, moisture levels, thickness tolerances (±0.1mm), and surface tensile strength. This guarantees zero lot-to-lot stiffness variations.
We transition technical drawings and user requirements into market-ready PPE collections. Our prototyping division provides detailed spec documentation, material declarations, and custom packaging for automated retail distribution.
Strategic product iterations driving thermal insulation, wearable ergonomics, and eco-sustainable manufacturing forward over the next production cycles.
Refining vegetable-oil tanning formulas to elevate split leather shrinkage resistance from 180°C up to 260°C dry heat exposure without oil stiffening.
Integrating 0.8mm silica aerogel membranes within the back-of-hand zone, reducing hand weight by 35% while doubling radiant thermal resistance.
Deploying graphene-infused yarn inside high-wear seam threads to deliver cut-level 5 resistance paired with fast dissipation of conductive contact heat.
Achieving zero water discharge with 100% bio-degradable preservation chemistry, fulfilling future EU environmental and ESG directives.
Critical engineering, certification, and procurement answers directly from our factory engineering team.
Type A designates heavy-duty welding gloves with higher thermal resistance, burn protection, and mechanical tear strength, ideal for high-heat MIG, stick, and submerged arc welding. Type B provides higher dexterity and tactile flexibility with lower mechanical ratings, specifically engineered for precision TIG operations.
Standard polyester or nylon threads decompose at temperatures between 180°C and 220°C, causing catastrophic seam separation when exposed to spatter. Para-aramid Kevlar® thread remains stable past 425°C, does not melt, and resists spark abrasion across continuous welding cycles.
Split cowhide provides high abrasion, spark deflection, and heat dissipation for heavy-amperage structural lines. Top-grain goatskin offers high tensile strength per millimeter, tensile flexibility, and tactile feel for TIG rods. Pigskin excels in oily or humid conditions due to porous breathability without stiffening after drying.
Standard OEM sample development takes 7–10 days with written tech packs. Container bulk shipments average 35–45 days across our scalable 500,000 pairs/month capacity. Standard custom MOQ starts at 1,200 to 2,400 pairs per style depending on leather customization and private label packaging requirements.
Explore our full-body flame-retardant and thermal protection product lines. Engineered in harmony with our welding glove range to provide comprehensive job-site PPE packages.