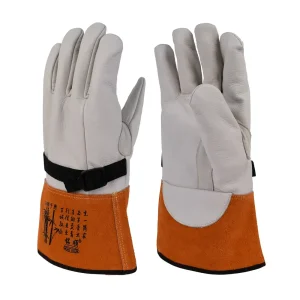
Factory-direct OEM/ODM thermal workwear manufactured with split cowhide, top-grain goatskin, and flame-retardant industrial textiles.
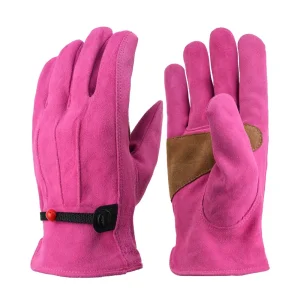
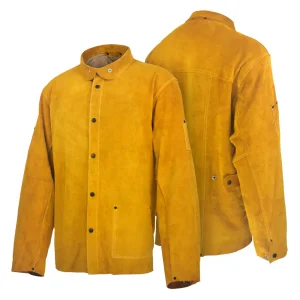
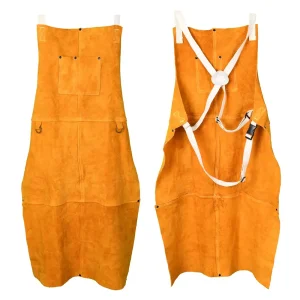

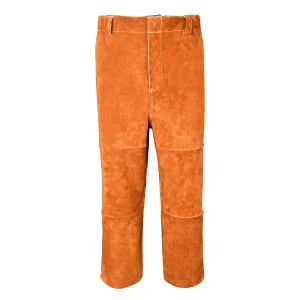
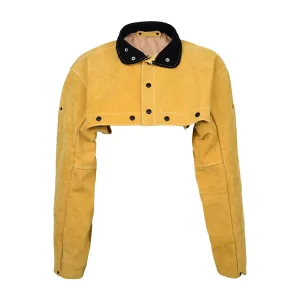
Operating directly within the Gaozhou industrial leather corridor, Ming Shun integrates raw material processing, tannery chemical consistency, and automated precision cutting under a singular roof.
Direct control over hide splitting yields exact calibers (1.2mm–1.6mm A-grade cowhide). Our proprietary vegetable-synthetic re-tanning eliminates volatile organic compounds and maintains heat resistance thresholds exceeding 500°C contact exposure.
Heat degradation occurs at thread failure points first. Every pair of custom heat proof gloves utilizes 3-ply to 5-ply Para-Aramid (DuPont Kevlar®) stitching with buried seam welting, avoiding spark burn-through and mechanical unraveling during heavy load transfer.
Located in Gaozhou, Guangdong, our 25+ year infrastructure spans 1,000+ technical employees, achieving over 500,000 pairs of gloves monthly capacity. Complete supply-chain resilience shields clients from geopolitical and seasonal delivery shocks.
Modern occupational safety necessitates a paradigm shift from thick, unyielding leather mitts to ergonomic, multi-layer composite thermal shields that balance tactile dexterity with extreme contact thresholds.
Combining outer silicone-impregnated split leather with aluminized basalt foil and needle-punched aramid fleeces to reflect up to 95% of radiant infra-red heat loads.
3D-articulated keystone thumb patterns eliminate operator hand exhaustion in repetitive robotic feed manipulation, significantly decreasing workplace injury frequencies.
Unifying EN 407 (Thermal Risks), EN 388 (Mechanical Cut/Tear), and ANSI/ISEA 105 into unified manufacturing specs for seamless global inventory distribution.
Implementation of zero-effluent leather production cycles and waterborne adhesives adhering strictly to European REACH non-carcinogenic chemical compliance limits.
Engineered configurations explicitly customized for metallurgy processing plants, offshore platforms, automotive welding robots, and commercial foundries.
Engineered for extreme convective radiant heat up to 1000°C. Utilizing aluminized cowhide gauntlets with multi-tier fleece insulators to protect against molten slag splash and severe IR radiation.
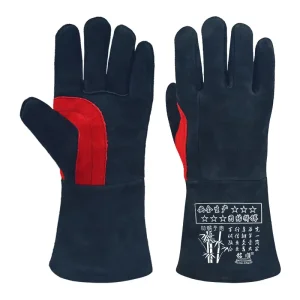
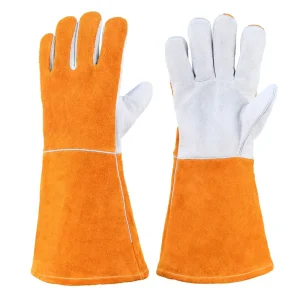
Heavy structural steel fabrication demands resilience against spatter and persistent contact heat. Features 1.4mm grade-A split cowhide reinforced with split palm patches and thumb-crotch buffers.
Focuses on fine tactile sensitivity. Employs ultra-supple premium top-grain goatskin with zero-seam index construction, enabling feed-wire micro control while shielding against scattered UV rays.
| Thermal Glove Classification | Material Core Architecture | Contact Heat Threshold (EN 407) | Primary Industrial Use Case | Reinforcement Specification |
|---|---|---|---|---|
| Type A Heavy Fabrication (MS-826BH) | Split Cowhide + Flame Retardant Cotton | 350°C for ≥ 15 seconds | Shipyard Hull MIG / SMAW Arc | Double Palm + Full Kevlar Welt |
| Type B Precision Tactile (MS-862) | Top-Grain Goatskin + FR Cuff | 100°C for ≥ 15 seconds | TIG Aerospace & Pipe Fabrication | Keystone Thumb + Unlined Finger |
| Thermal Foundry Extreme (MS-760F) | Aluminized Split Cowhide + Wool Liner | 500°C for ≥ 15 seconds | Foundry Casting & Ingot Handling | Insulated Back Hand Heat Pad |
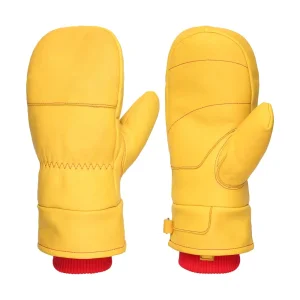
| Sub-Zero Industrial Hot-Work (MS-GVR05) | Water-Resistant Grain Cowhide + Polar Fleece | 250°C for ≥ 15 seconds | Arctic Pipelines & Offshore Gas | Thermal Barrier Vapor Lock Seam |
We eliminate international sourcing risks via audited quality gates, predictable delivery timelines, and full traceability across every production lot.
Comprehensive CAD analysis, sizing matrix alignment (Sizes 7-12 / S-3XL), leather thickness grading, and compliance pre-verification.
Rapid proto-typing within 5-7 working days. Physical evaluation samples submitted for chemical and tensile burn validation.
Embossed heat stamps, screen-printed silicone logos, woven woven cuffs, full-color barcode hangtags, and master carton packaging.
Strict AQL 1.5/2.5 testing. Stitch-per-inch density counting, Kevlar heat integrity confirmation, and dimensional fit certification.
Full container load (FCL) optimization via Shenzhen/Guangzhou ports. Fumigated heat-treated export pallets with desiccant barrier wrapping.
Direct, transparent answers from our engineering desk regarding compliance, production capacities, leather types, and order logistics.
Contact heat performance depends on leather density and thickness. Split cowhide (1.2–1.4mm) offers dense, fibrous structures suitable for level 2 and 3 contact heat (250°C to 350°C). Top-grain goatskin, while thinner, provides natural tensile flexibility for TIG dexterity, typically calibrated for level 1 (100°C) unless backed with an aramid insulating layer.
Standard MOQs for custom OEM heat-proof gloves start at 1,200 to 2,400 pairs per style/colorway, depending on bespoke leather dyeing requirements. Mass manufacturing requires approximately 30 to 45 business days post-sample sign-off. Repeat bulk contracts can leverage rolling warehouse safety stocks for 14-day dispatches.
Yes. Standard screen prints degrade under elevated heat. We employ heat debossing (stamping directly into leather grain), high-temperature silicone vulcanization, or embroidered patches stitched using non-combustible Para-Aramid threads to guarantee marking durability in extreme thermal environments.
Absolutely. Ming Shun provides official third-party test reports (from notified bodies such as CTC, SATRA, or SGS) covering EN ISO 11611 (Welding Garments), EN 12477 (Welding Gloves Type A/B), and EN 388 mechanical resistance ratings. All documentation is supplied with pre-production batch clearances.
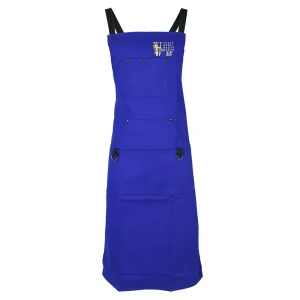
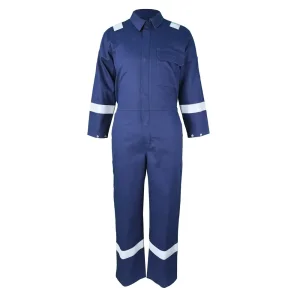
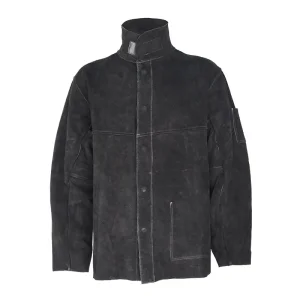
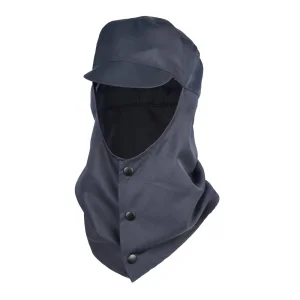
Explore high-demand certified welding coveralls, flame-retardant accessories, and heavy-duty winter leather PPE ready for customization.