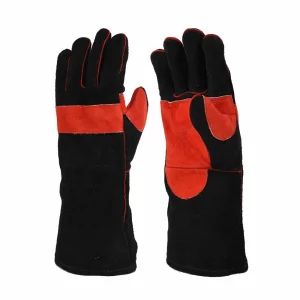
Direct manufacturer deployment of heavy-duty industrial leather gloves, ergonomic cut-and-heat welding barriers, and protective apparel built to rigorous international test standards.
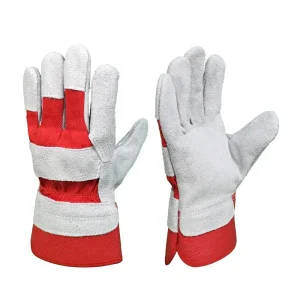
An exhaustive whitepaper review of supply chain realignments, EN 388/EN 407/ANSI 105 certification dynamics, and the critical transition toward high-integrity OEM manufacturing.
The global industrial protective gloves market is expanding rapidly, driven by automated manufacturing, heavy infrastructure, and aggressive workplace safety mandates across North America, Europe, and the APAC region. Sourcing leaders are moving decisively away from unverified trading intermediaries, preferring direct integration with source tanneries and manufacturing facilities.
Navigating global compliance requires complete mastery over shifting international testing protocols. Modern procurement managers require dual certification: European EN ISO standards (such as EN 388:2016+A1:2018 for mechanical risks and EN 12477 for welding) and North American ANSI/ISEA 105 cut/puncture classifications.
Hand injuries account for more than 40% of all recordable occupational workplace incidents in heavy fabrication and metal stamping. Modern safety engineering mandates that protective gloves eliminate hand fatigue while preserving tactile sensitivity, preventing workers from removing their PPE in high-risk zones.
Evaluating dermal tensile integrity, chrome versus eco-tannage thermal barriers, and reinforced seam engineering.
| Material / Construction Factor | Split Cowhide (A/AB Grade) | Top-Grain Goatskin | Pigskin Leather | Engineered Aramid Liners |
|---|---|---|---|---|
| Target Application | Heavy MIG/Stick, Slag & Radiant Heat | Precision TIG, Micro-Handling | Wet/Oily Machining, Low Temp | Cut Level A4-A9 Thermal Defense |
| Tensile Strength (MPa) | 18.5 – 22.0 MPa | 24.0 – 28.5 MPa (High density) | 14.0 – 17.5 MPa (Porous structure) | Over 3,000 MPa (Filament level) |
| Thermal Resistance | Continuous contact up to 350°C | Moderate contact heat (up to 150°C) | Breathable, up to 120°C | Non-melting, chars at >450°C |
| Dexterity Rating (EN 420) | Level 1 to Level 2 | Level 4 to Level 5 (Maximum) | Level 3 to Level 4 | Maintains flexible shell fit |
| Abrasion Cycles (EN 388) | >8,000 Cycles (Class 4) | >2,000 Cycles (Class 2) | >4,000 Cycles (Class 3) | Variable composite dependent |
| Oil & Moisture Recovery | Stiffens without proper conditioning | Naturally water repellent (Lanolin) | Dries soft without stiffening | Hydrophobic yarn coatings available |
Unlike factories relying on third-party commercial wet-blue stock, Guangdong Ming Shun oversees the tanning and grading process at the source. Controlling chrome levels, pH values (3.5–4.5), and fatliquor percentages ensures zero dermal irritation and repeatable heat insulation across 500,000 pairs monthly.
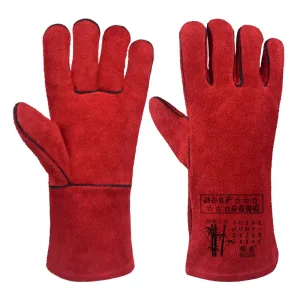
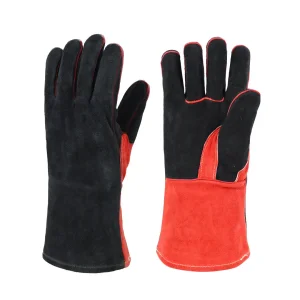
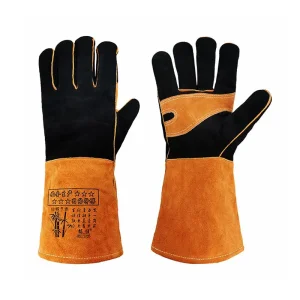
Welding and heavy mechanical environments expose seams to extreme heat and abrasive metal burrs. We construct our hand protection with 4-ply Kevlar® heat-resistant aramid threading protected by reinforced leather welts. This prevents thread burn-through and seam ruptures when handling heated structural components.
Traditional flat glove profiles force the worker's hand to fight against stiff leather resistance. Our pattern design uses three-dimensional anatomical digit curvature and inset keystone thumb geometry. This design cuts grip fatigue by up to 34% during long shifts in shipyards and heavy fabrication shops.
From ESG-compliant eco-tanning to intelligent tracking and hybrid nanocomposite shielding, discover what defines next-generation PPE manufacturing.
Continuous operational heritage in Gaozhou City, Guangdong, refining leather hand PPE since 1998.
Dedicated master cutters, pattern technicians, precision seamstresses, and certified QC inspectors.
Scalable mass production capacity designed to fulfill multi-container global distributor contracts reliably.
Fast turnaround from approved master sample to packed container dispatch at Gaozhou/Shenzhen ports.
Global chemical regulations, notably EU REACH Annex XVII, place stringent limits on extractable Chromium VI content in leather PPE (under 3 mg/kg). Our R&D facility utilizes organic vegetable retanning and modified trivalent synthetic agents to completely eliminate the risk of carcinogenic oxidation.
Future hand protection combines traditional leather durability with engineered synthetic backings. By fusing split cowhide palms with 4-way stretch breathable flame-retardant (FR) textiles, we achieve maximum spatter protection while improving heat release on the back of the hand.
Moving beyond manual scissor work, Ming Shun's production lines employ digital oscillating knife and CNC laser cutting arrays. Computerized pattern nesting scans each raw hide for natural flaws, maximizing yield, minimizing waste, and guaranteeing sub-millimeter component tolerances.
Engineered hand protection built to address precise thermal loads, mechanical hazards, and ergonomic demands across major global industries.
Handling sheet metal panels after high-tonnage stamping requires maximum cut defense combined with dry grip. Our goat and cowhide hybrid styles provide EN 388 Level D/E cut barriers alongside natural puncture resistance against micro-burrs and sharp flashings.
Salt-fog humidity, wet steel, and constant multi-process stick/flux-cored welding require heavy-duty dermal shielding. Ming Shun's oil-treated split cowhide retains its grip and flexible feel without hardening or rotting under marine climate cycling.
Ironworkers operating at heights require hand protection that handles abrasive structural beams, impacts, and heavy torque wrenches. We reinforce palm contact zones with double-layer split cowhide to resist severe abrasion from handling shot-blasted I-beams.
Every pair of gloves and protective garment manufactured at our Gaozhou facility follows a strict, traceable manufacturing workflow to eliminate quality variations.
Hides are graded for thickness (1.1mm to 1.4mm), fiber density, surface elasticity, and moisture content before entering production lines.
Dedicated tannery drums match custom Pantone brand colors while applying flame-retardant chemistry directly into the leather structure.
Hydraulic clicking presses and computerized laser cutters shape fingers, thumbs, cuffs, and reinforcements with exact sub-millimeter tolerances.
Branding is applied via deep hot-stamp leather debossing, multi-color heat transfers, or flame-retardant direct embroidery.
Skilled operators assemble gloves using 4-ply Kevlar® thread, inserting protective leather welt strips along high-risk seams.
Breathable cotton, fleece, or cut-resistant composite liners are inserted and bonded to prevent lining pull-out when hands are sweaty.
Gloves undergo heated hand-form shaping to set the ergonomic pre-curve, eliminate creases, and verify dimensional sizing consistency.
Every pair is inspected for loose stitches, thickness variations, and needle fragments (via automated metal detection) before export packing.
Technical guidance for safety equipment importers, wholesale distributors, and safety engineers partnering directly with Ming Shun.
Guangdong Ming Shun Labour Protective Products Co., Ltd. (formerly Gaozhou Mingshun Labor Protection Products Co., Ltd.) is a factory-direct manufacturer located in Pukang Industrial Park, Gaozhou City, Guangdong. We operate our own leather tanning and processing facilities, precision die-cutting shops, and dedicated sewing lines with over 1,000 on-site employees.
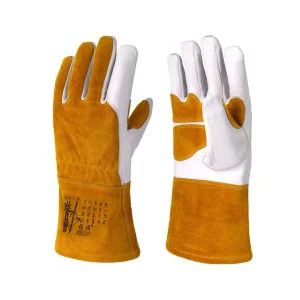
Type A gloves provide higher thermal protection, heavy-duty radiant heat defense, and superior mechanical resistance (abrasion, tear, puncture), making them ideal for high-amperage MIG and Stick welding. Type B gloves offer greater dexterity and tactile feel at the cost of lower thermal bulk, designed specifically for precision TIG welding.
Yes. Our OEM/ODM engineering teams regularly work from buyer tech packs, CAD sketches, or competitor benchmark samples. We can adjust panel patterns, leather thickness, lining blends, custom leather dye shades, woven branding labels, debossed palm logos, and retail-ready packaging to match your program.
Standard OEM glove orders typically start at 1,200 to 2,400 pairs per style/colorway, depending on custom leather dyeing needs. Standard lead times average around 45 calendar days after master pre-production sample sign-off, supported by our 500,000+ pairs monthly factory capacity.
We maintain strict control over our wet-end chemistry and drumming baths. By using high-grade trivalent chromium agents, organic vegetable masking tannins, and exact pH neutralization baths, our finished leathers consistently test below the 3.0 mg/kg limit under ISO 17075-1:2017 detection standards.
We follow strict AQL 1.5/2.5 inspection standards across every production batch. In addition to manual dimensional and seam pull-force tests, 100% of finished gloves pass through conveyorized metal detection tunnels to ensure zero broken needle fragments remain inside the fingers or palm padding.
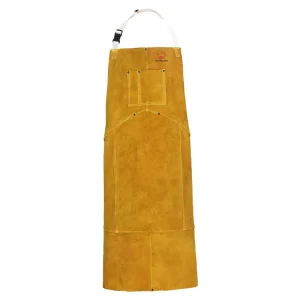
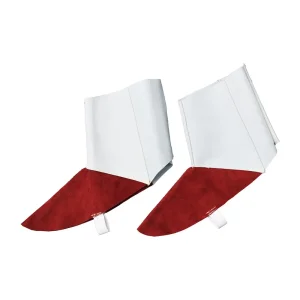
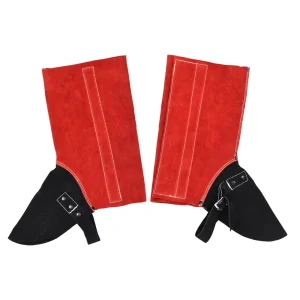
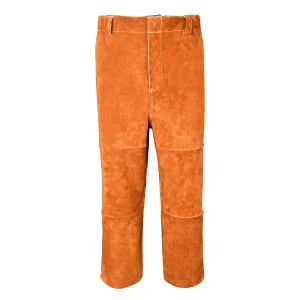
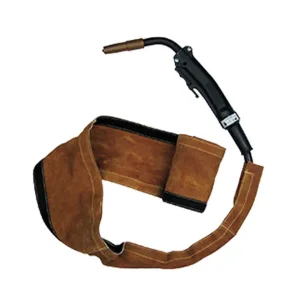
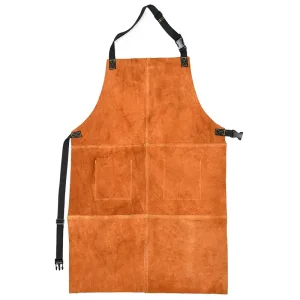
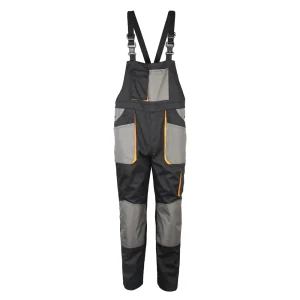
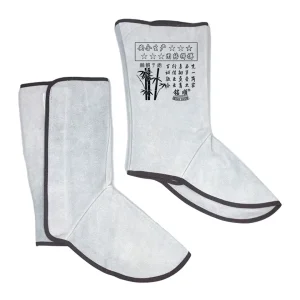
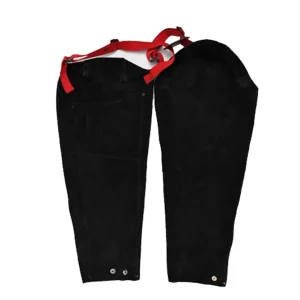
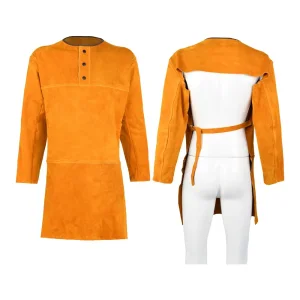
Complete your hot-work and heavy handling protective programs with our split cowhide welding aprons, spats, trousers, protective cable covers, and durable workwear accessories.